Skip to content
01

CompleteJanuary 2026 – June 2026

Stryker logo

Precisely constrains and moves optical devices with respect to a target. Four motorized and four manual axes, 10 µm resolution, inside a blackout cage. Replaced a completely manual bench.

Role
R&D Mechanical Engineering Co-op
Organization
Stryker Endoscopy
Timeline
January 2026 – June 2026
Tools
SOLIDWORKS, Creo, HALT chamber, Standard + torsional Instron, One-off fixtures, Excel
Project type
R&D Engineering · Experimental Design · Precision Motion · Verification + Validation · Medical Devices
01.0 — IN MOTIONThe bench moving through its motorized axes.

Specifications

Positioning resolution
10 µm
Motorized axes
4
Manual axes
4
Optical control
Complete blackout cage
Fixture value
≈ $25,000
  • R&D Testing
  • Experimental Design
  • Automation / Motion Systems
  • Medical / Human-Centered Design
01

Assembly

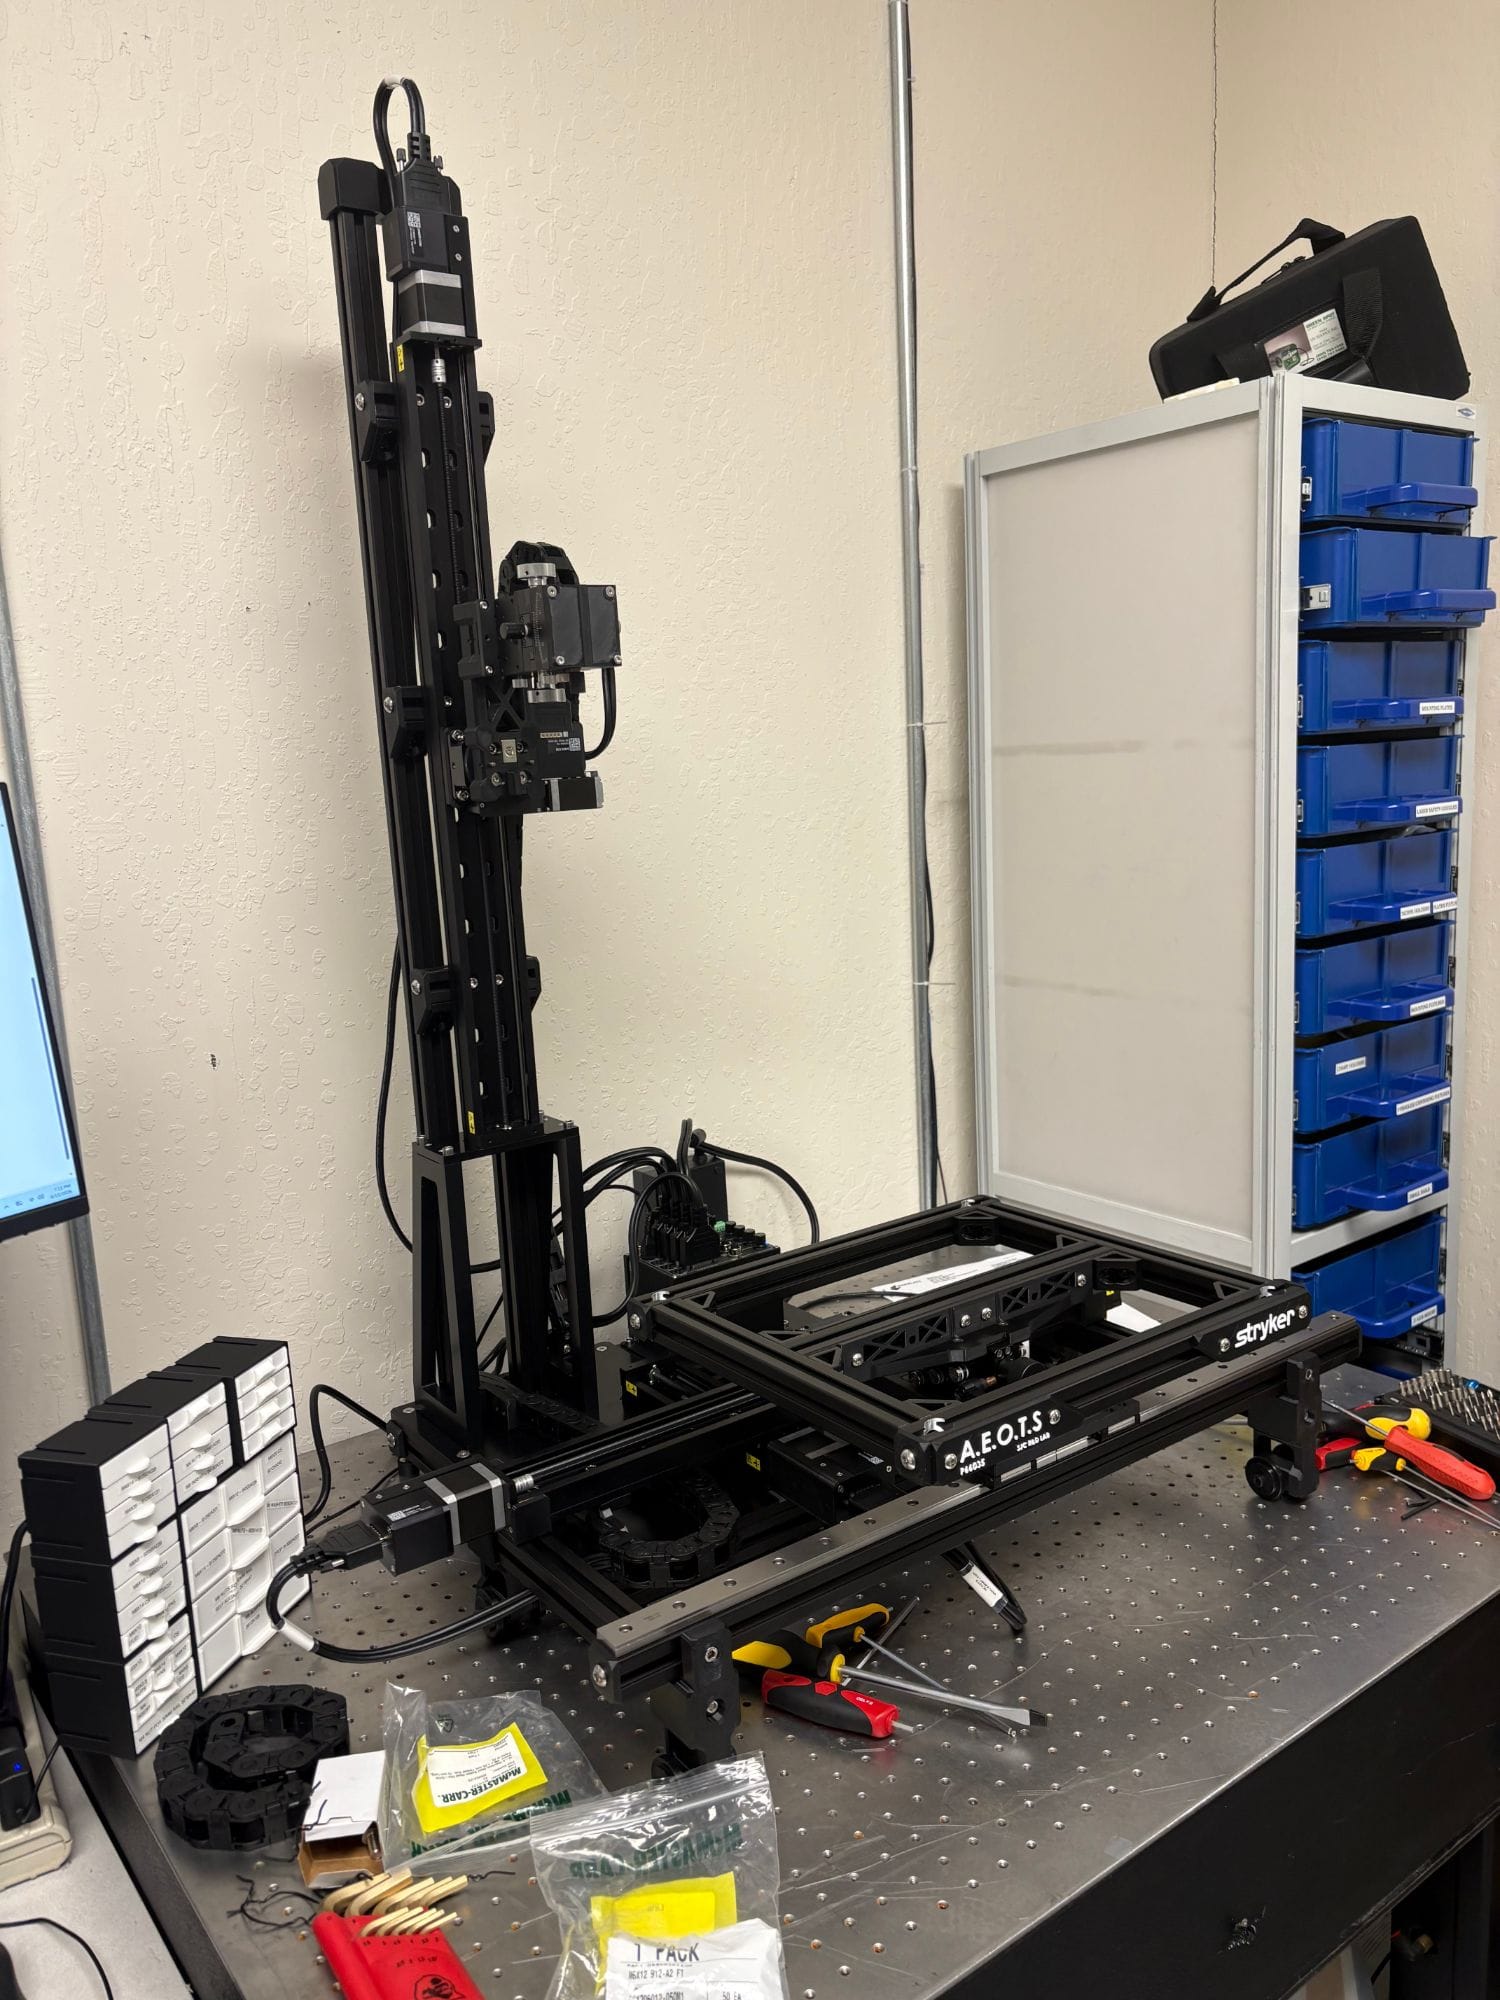
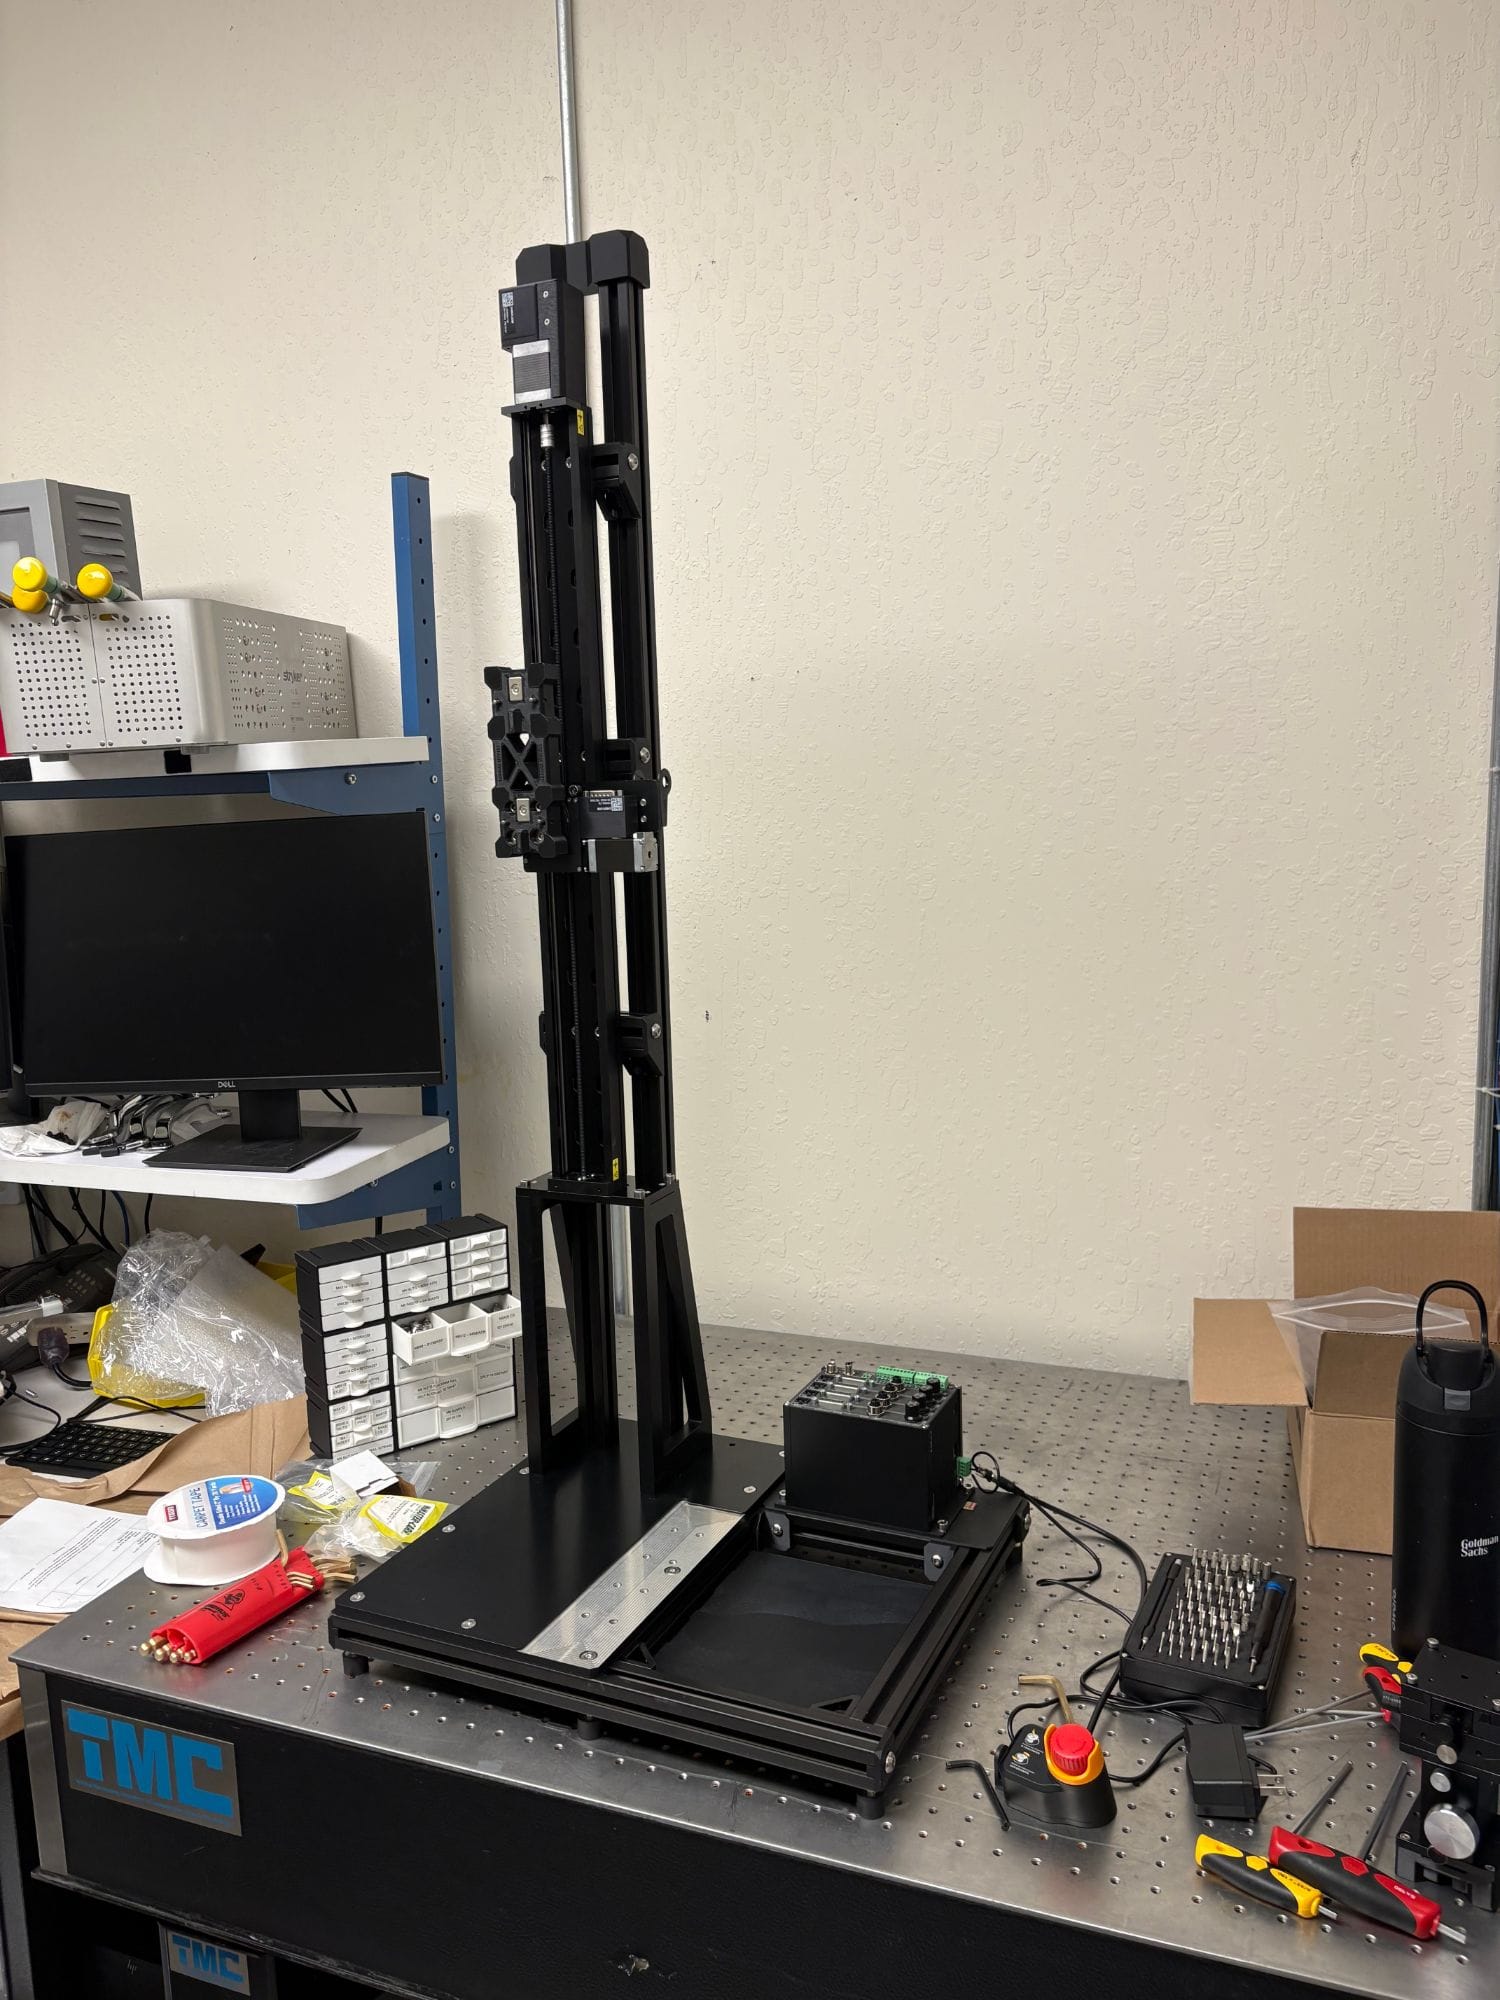
The assembled bench outside its cage: a vertical tower with a stage head, a two-axis gantry stage on rails, and the controller behind.
01.27 — FULL VIEWThe assembled bench outside the cage.
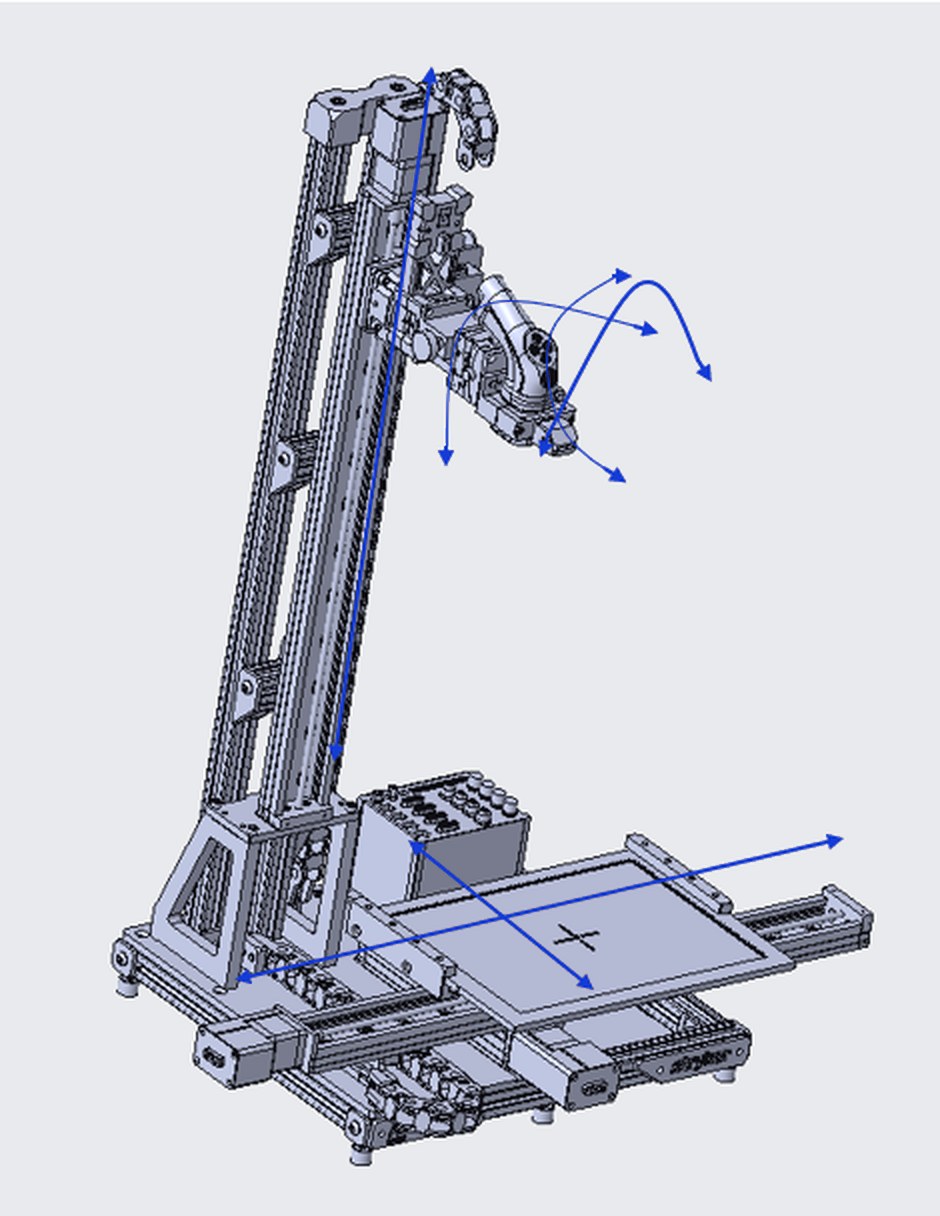
CAD assembly of the optical positioning gantry: a vertical tower on a two-axis base stage with an articulated head at the top, travel arrows marking each axis of motion.
01.1 — GANTRY ASSEMBLYThe gantry assembly, with each axis of travel annotated.
02

Imatest manual adjustment

Purely motorized adjustment risks collision, so a lab jack was incorporated beneath the larger light box.

The light pad kept its functionality, and the offset of the light box was designed in.
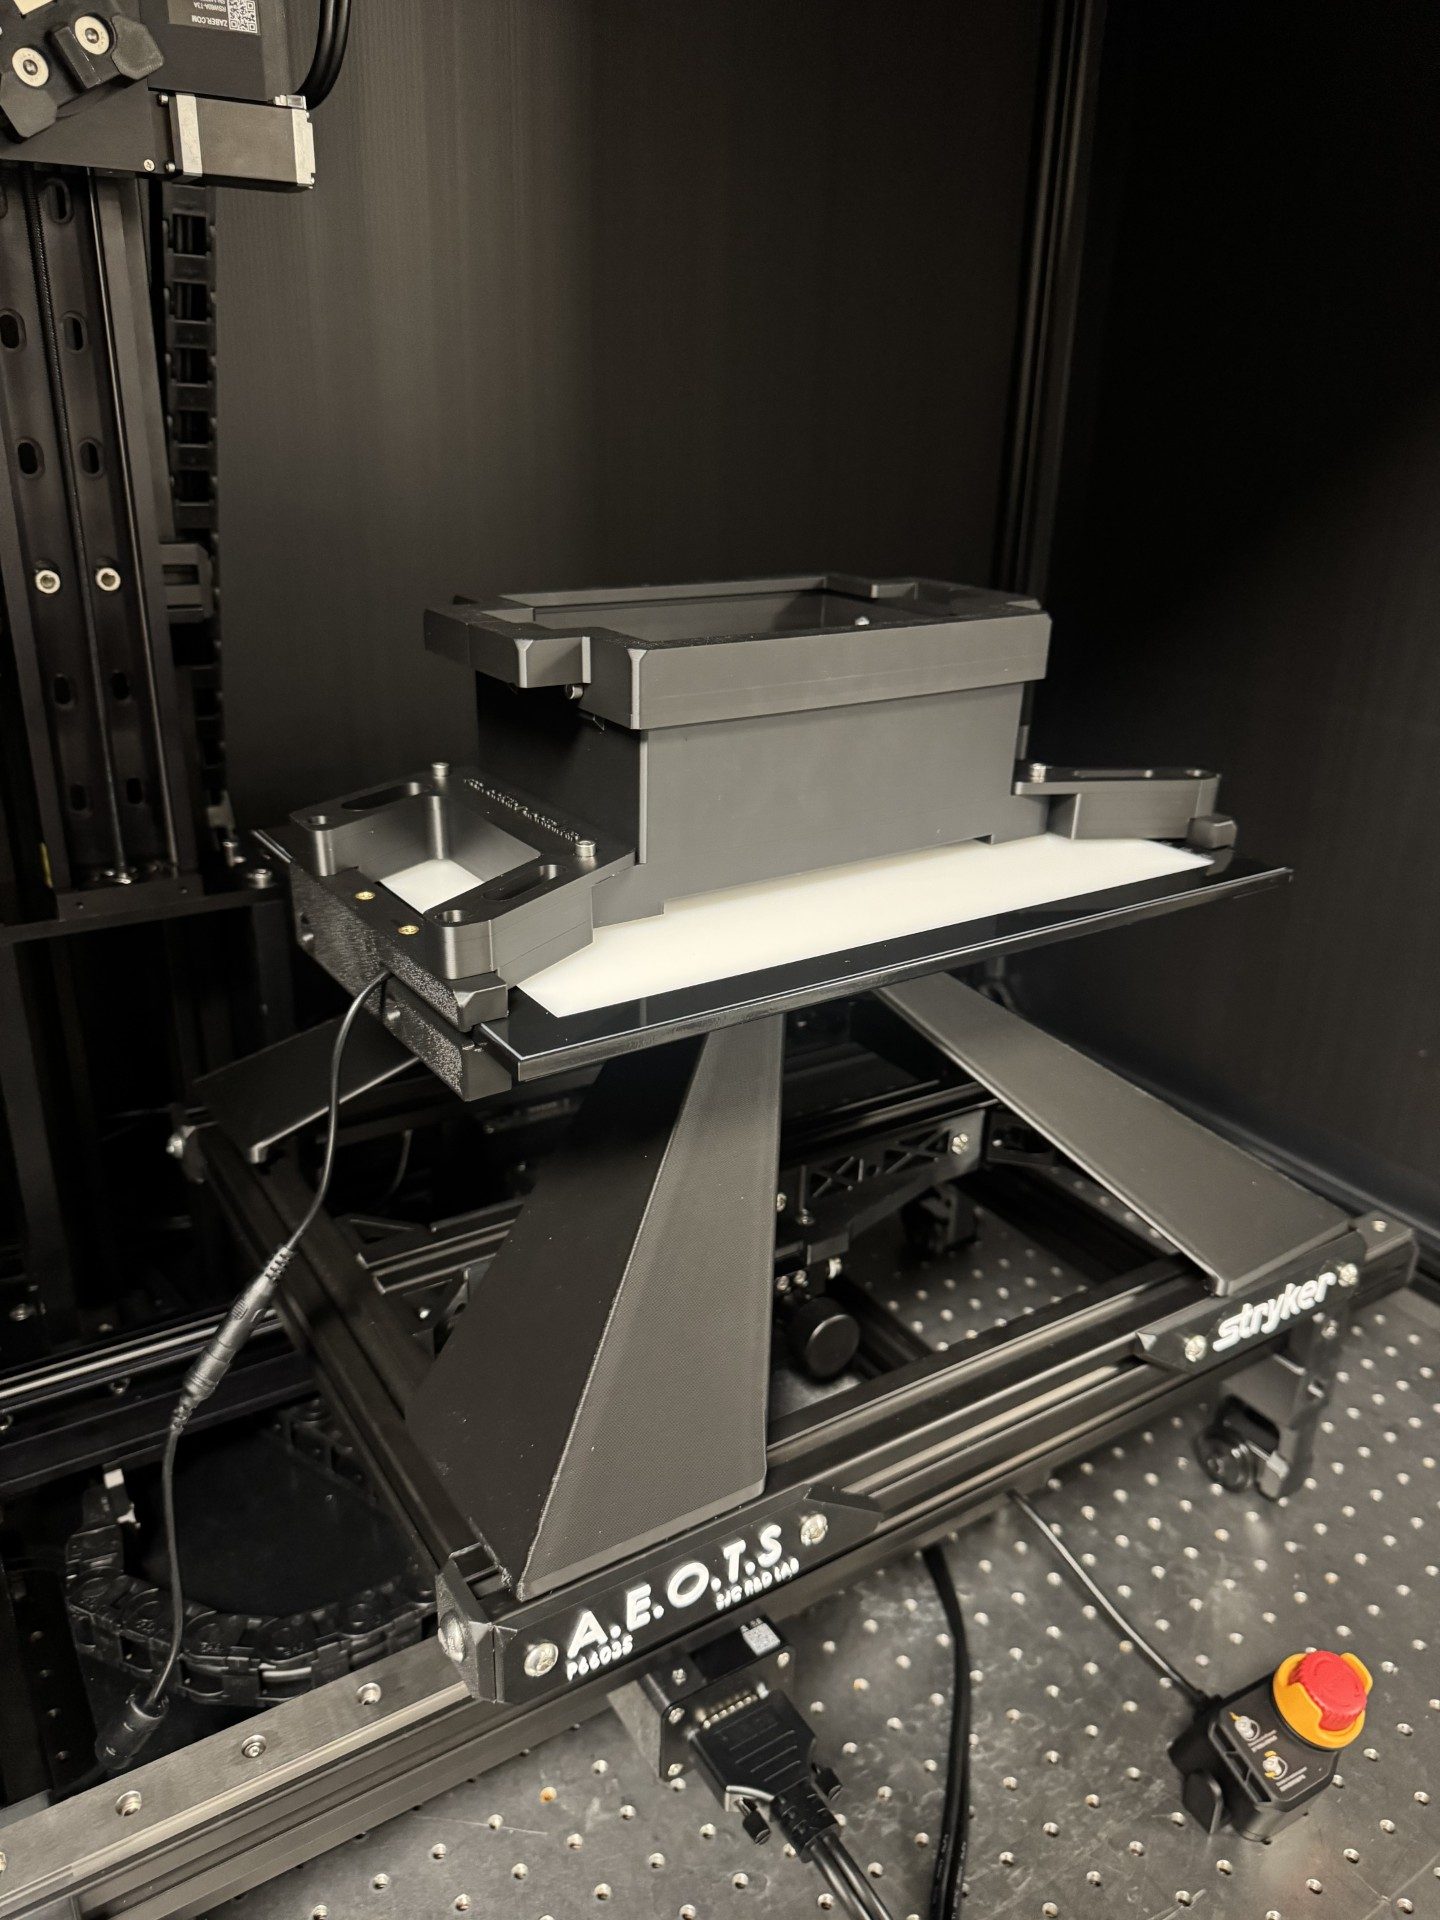
The light box mounted on a lab jack inside the cage, positioned above the target stage.
01.6 — LIGHT BOXLight box on its lab jack — manual height adjustment, retained to avoid collision risk.
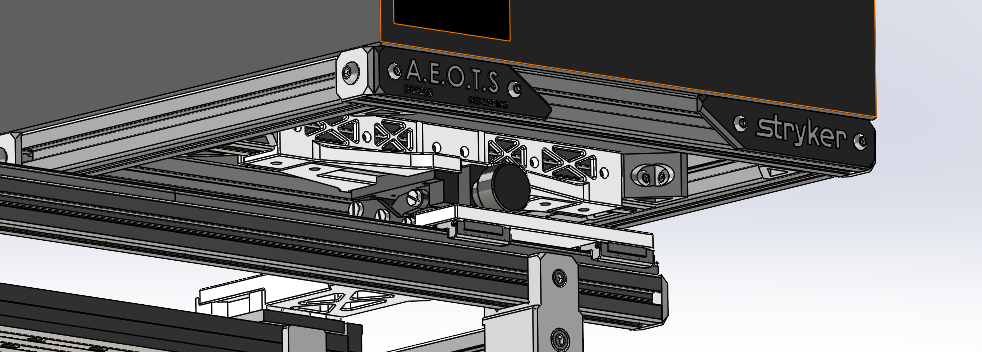
CAD view of a slim bracket mounted beneath an aluminium extrusion frame.
01.20 — LIGHT PAD MOUNTThe light pad keeps its function, mounted under the stage.
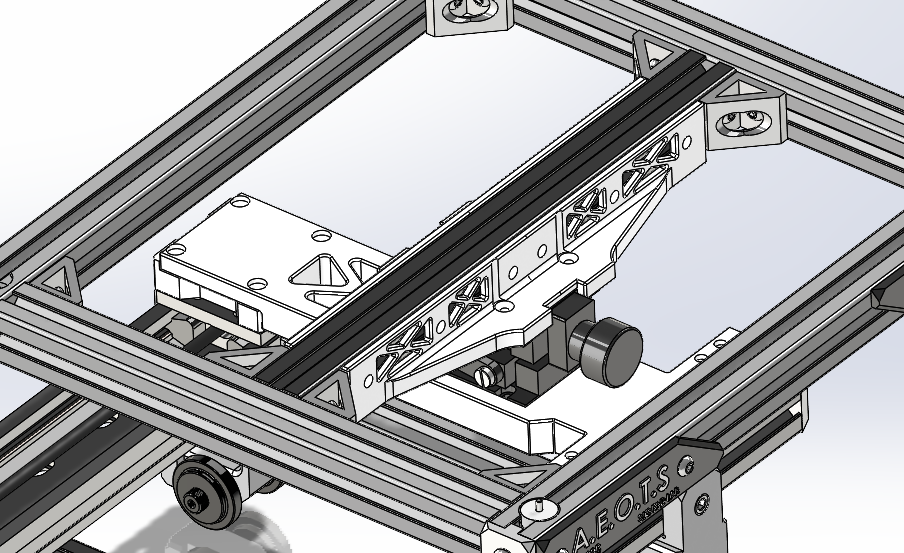
CAD view from below of a frame with a motor and lead screw between the rails.
01.21 — STAGE UNDERSIDEStage underside: drive hardware and the lab jack mount.
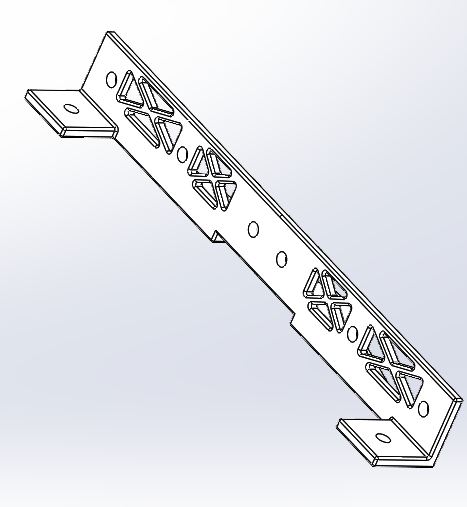
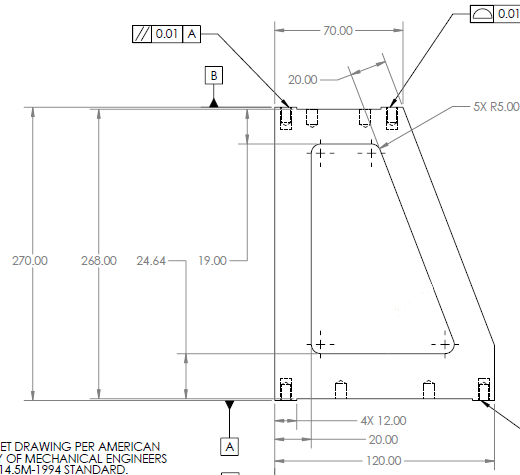
CAD view of a flat machined arm with triangular cutouts and mounting holes.
01.22 — JACK ARMSupport arm for the lab jack, lightened where it could be.
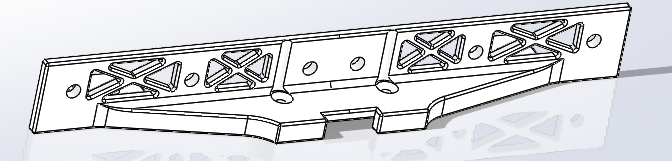
CAD view of two machined arms with lightening cutouts arranged side by side.
01.23 — ARM PAIRThe arms paired up.
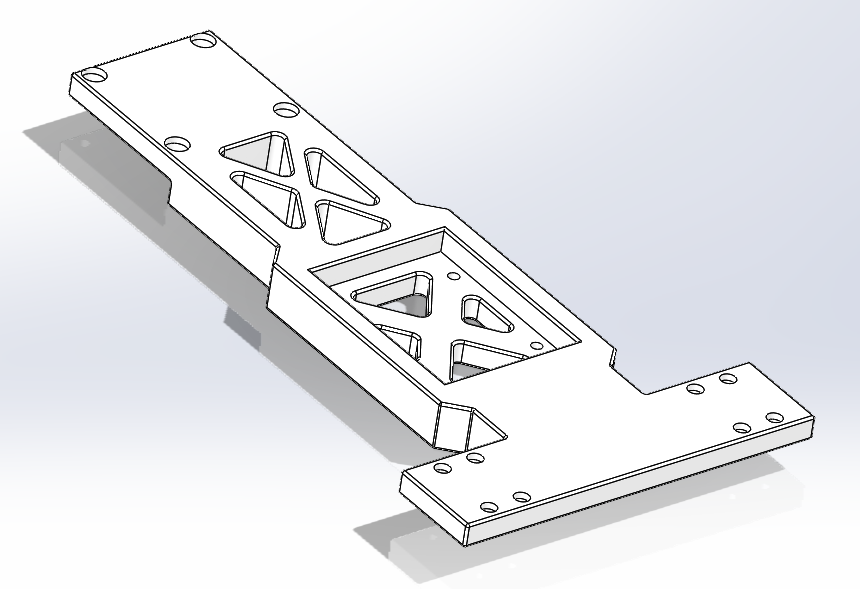
CAD view of a long flat plate with lightening cutouts and bolt holes.
01.24 — BASE PLATEBase plate for the jack assembly.
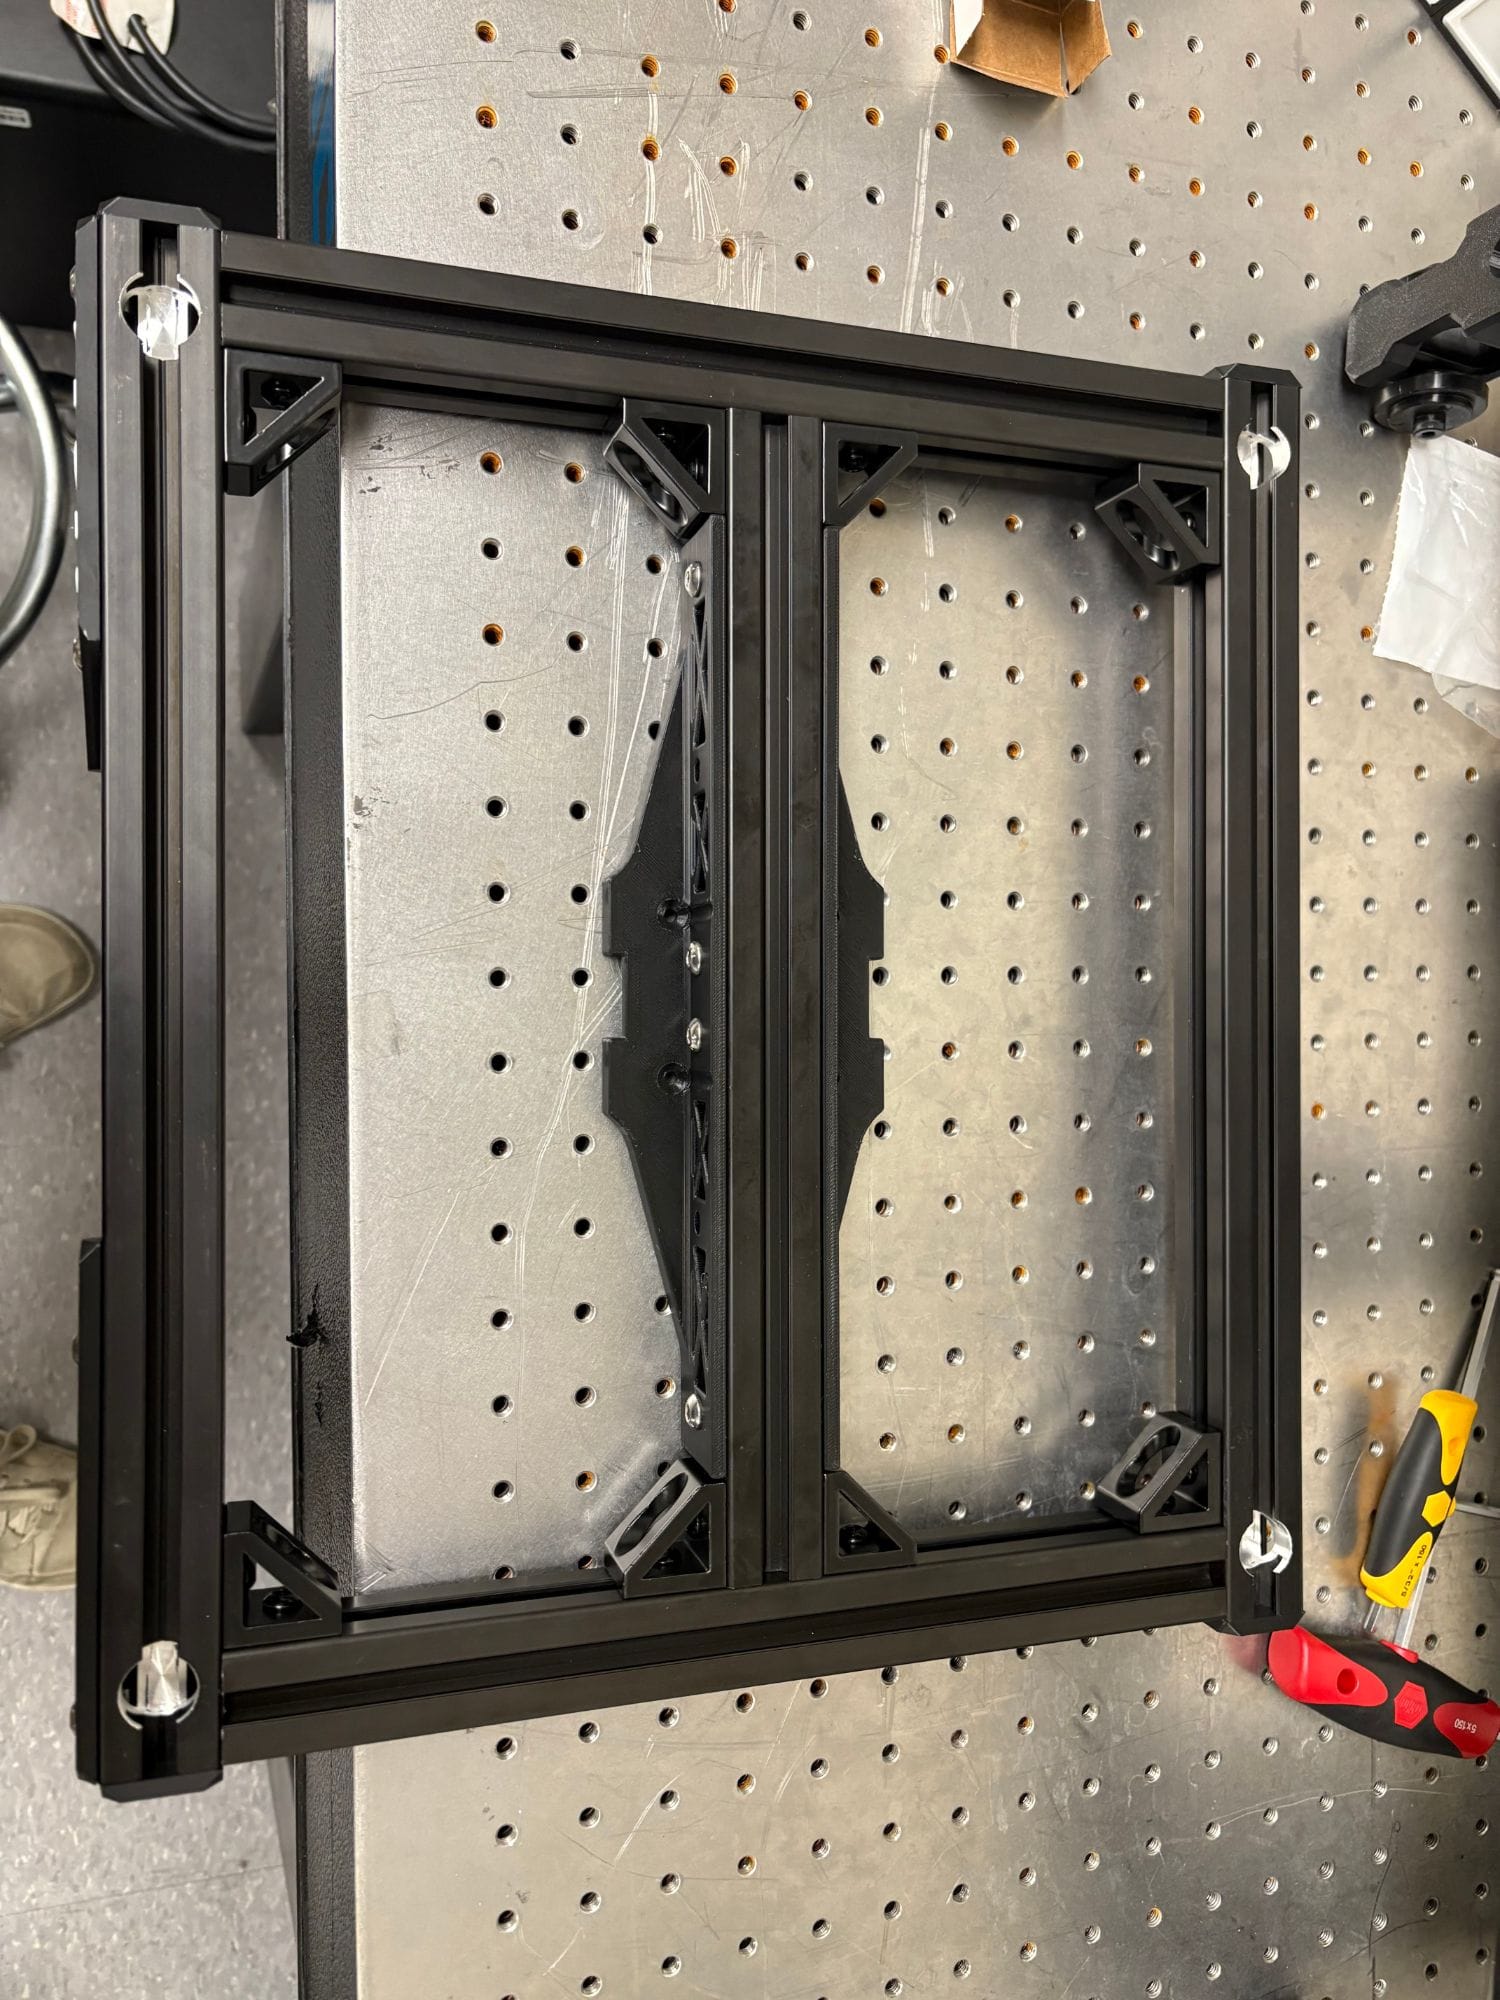
Overhead view of a black extrusion subframe with a printed centre bracket bolted across it.
01.30 — SUBFRAMEExtrusion subframe with the printed centre bracket.
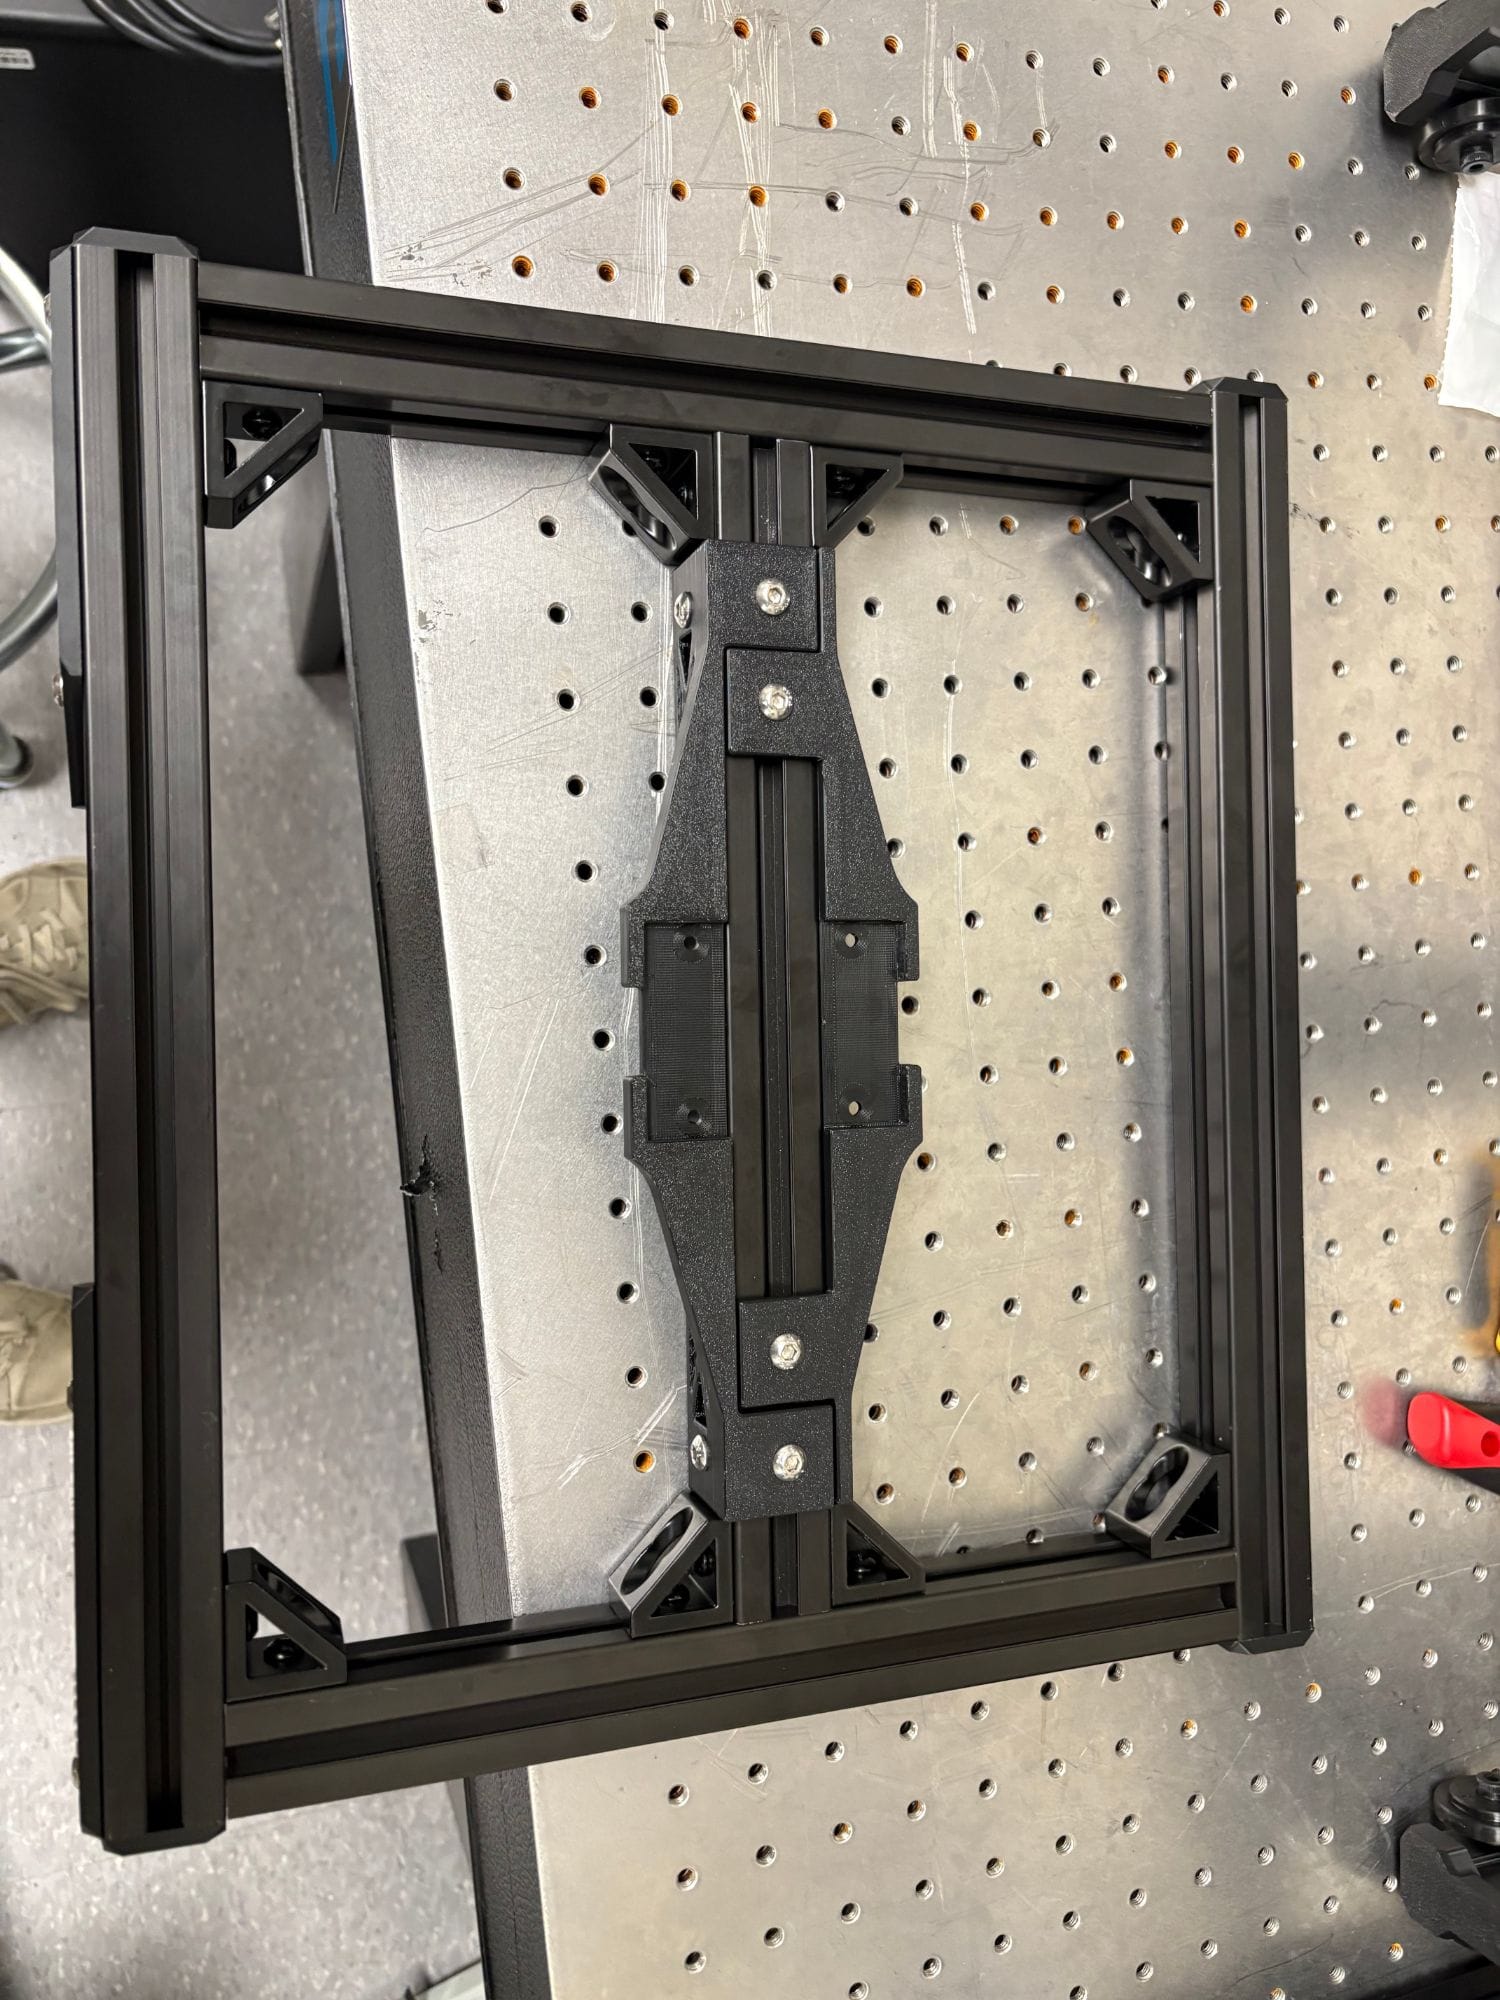
Overhead view of a two-bay extrusion subframe with printed diamond braces on the centre members.
01.31 — SUBFRAME, BRACEDThe two-bay subframe with printed braces.
03

Gantry height

The original height could not use the full Z-axis range of motion.

The offset was increased to accommodate the Imatest light box.
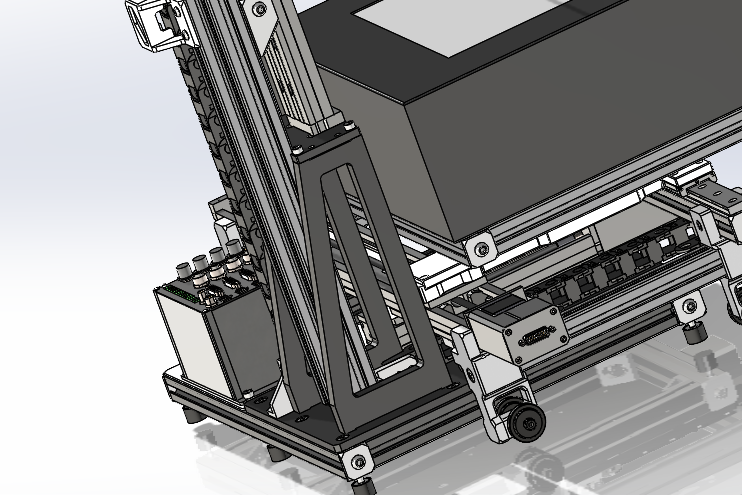
CAD elevation of a gantry tower showing an increased mounting offset above the base.
01.9 — GANTRY HEIGHTGantry offset increased — the original height could not use the full Z travel.
CAD detail of a bracket raising a tower above its base plate.
01.25 — OFFSET DETAILThe increased offset, in detail.
04

Fixtures

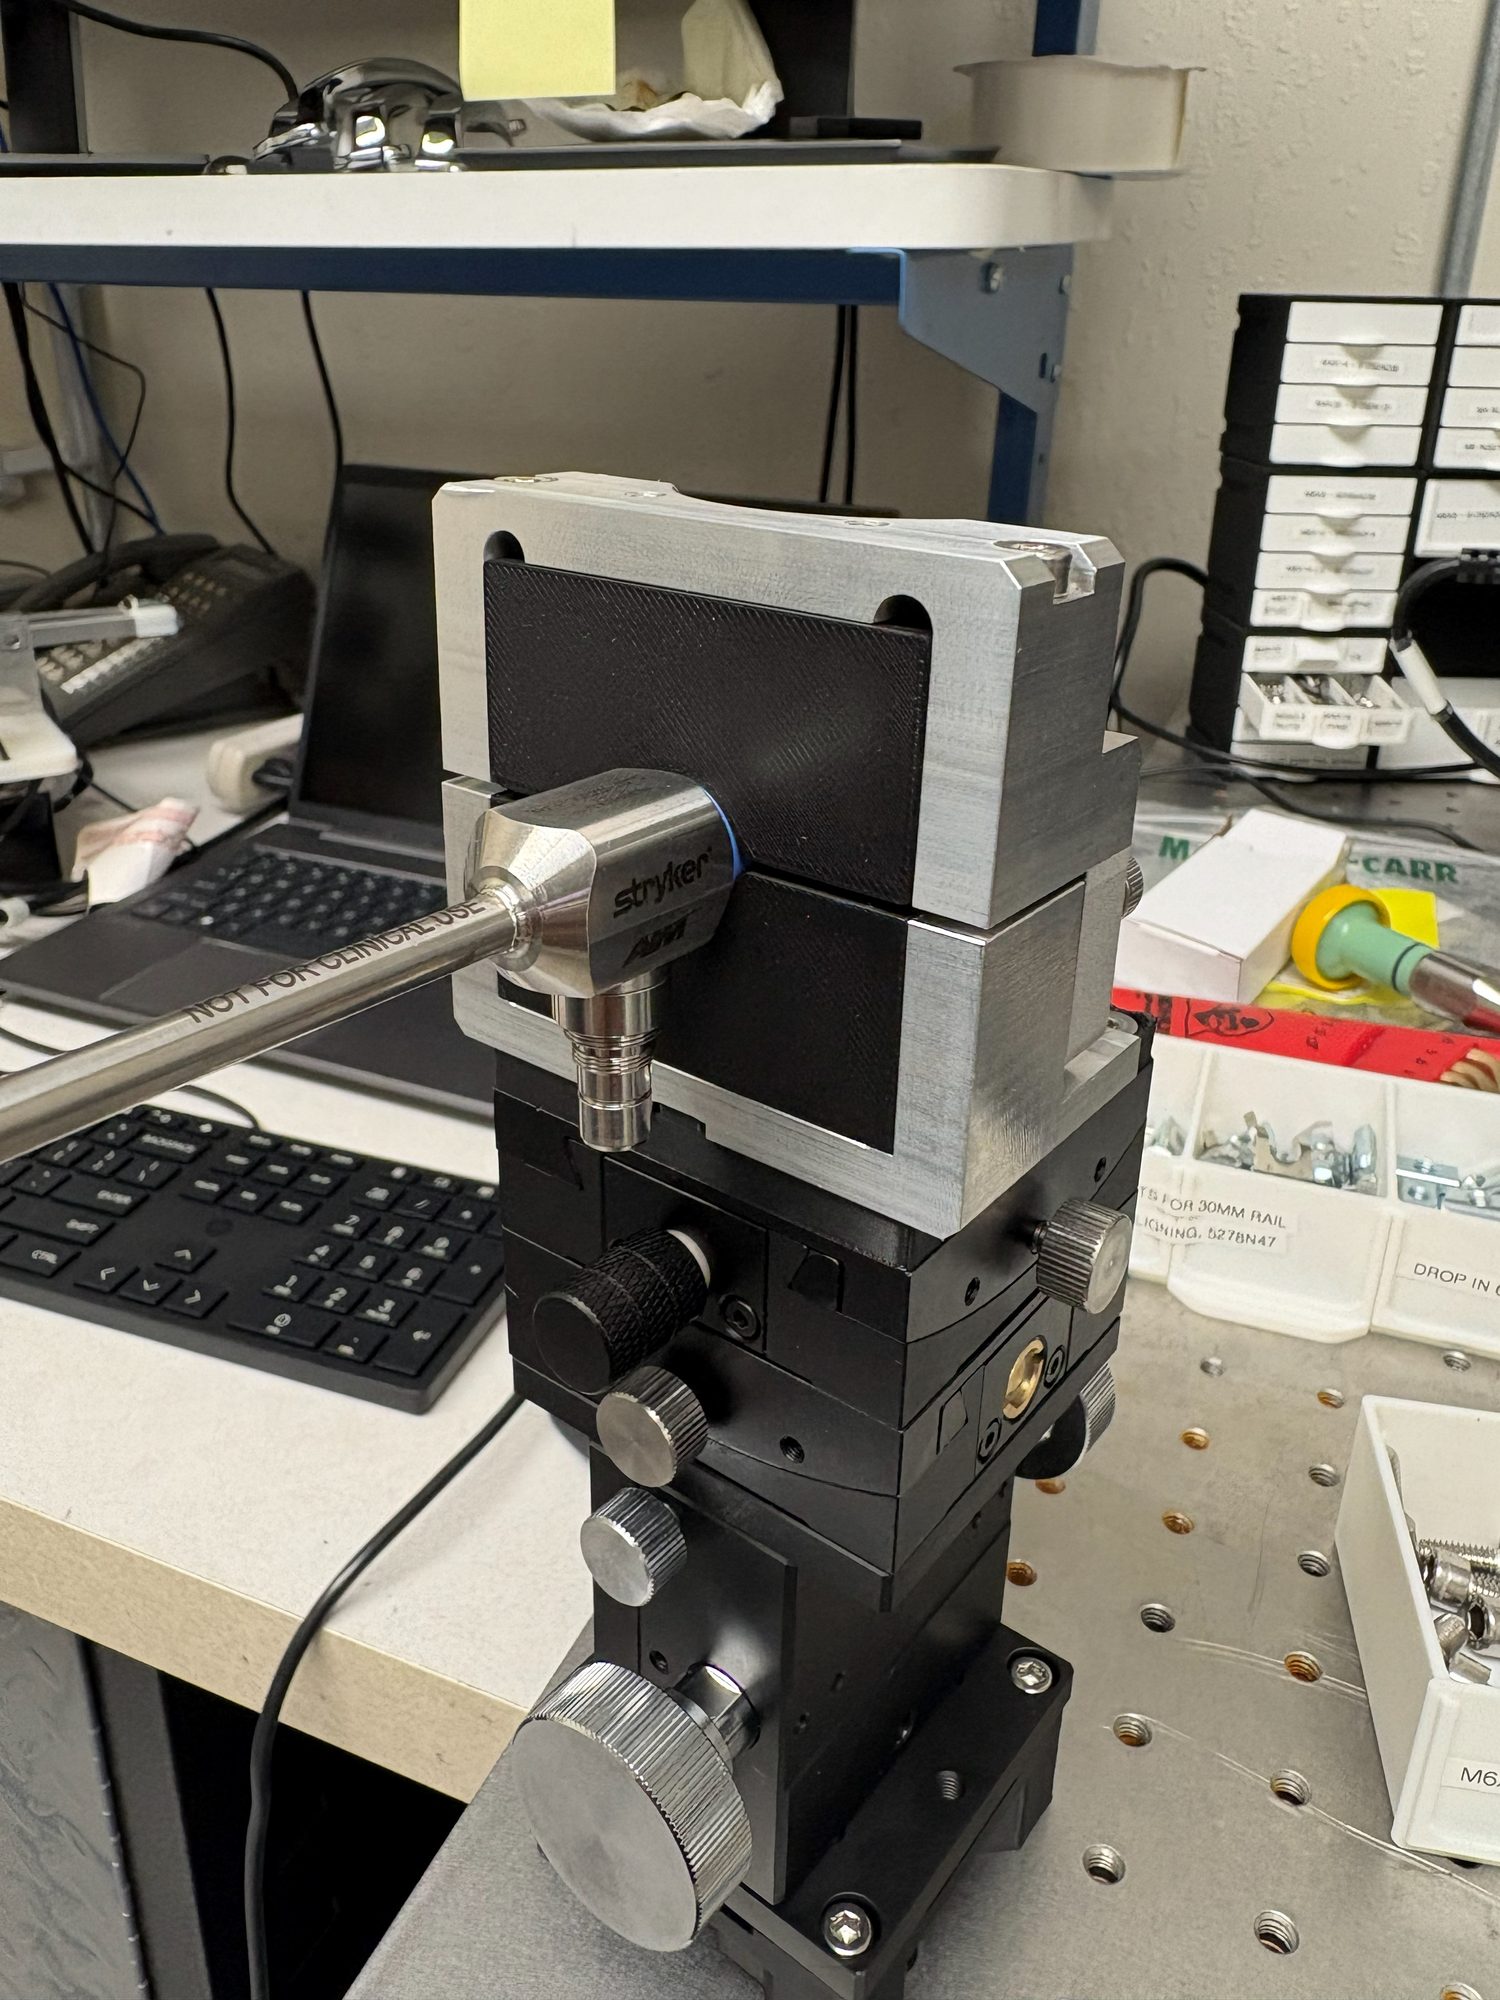
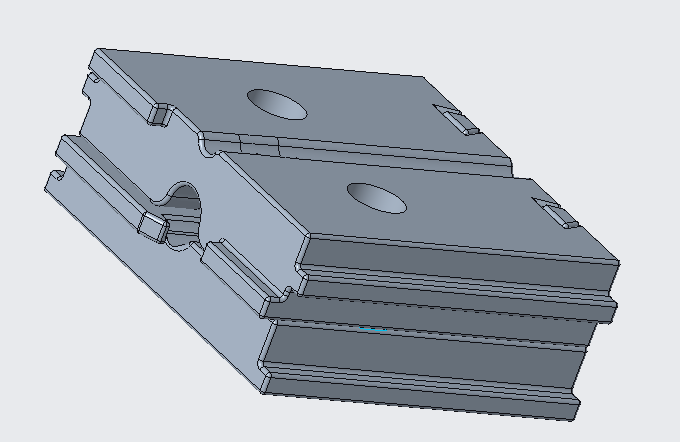
A machined universal clamp with printed inserts fixtures any size or diameter scope.

A second fixture holds any size flexible scope tip.
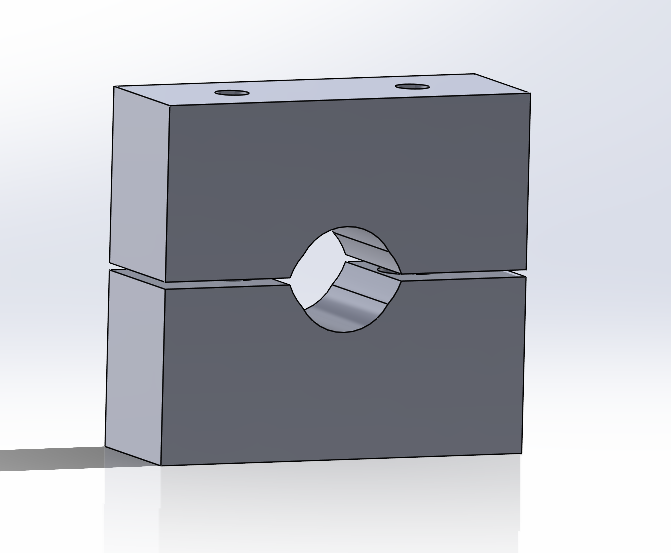
CAD of the machined universal scope clamp, split into two halves around a central bore.
01.4 — UNIVERSAL CLAMPThe machined universal clamp, which takes printed inserts for each scope diameter.
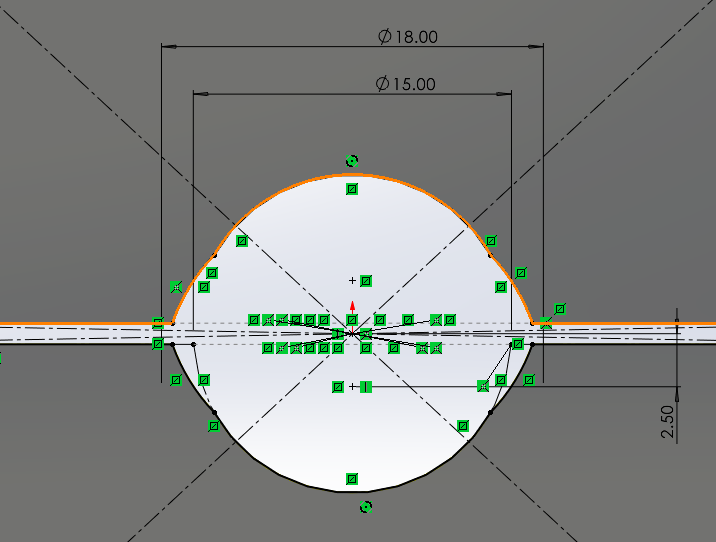
Dimensioned sketch of the clamp bore showing the 15 mm and 18 mm diameters the printed inserts span.
01.5 — ALIGNMENTInsert geometry: one machined clamp covers the full range of scope diameters.
A machined clamp mounted on a precision stage gripping the shaft of an endoscope.
01.7 — CLAMP IN USEThe clamp in use, holding a scope on the stage.
CAD view of a low block fixture with a shaped channel for holding a flexible scope tip.
01.8 — FLEXIBLE TIP FIXTUREA second fixture family holds flexible scope tips of any size.
05

Blackout cage

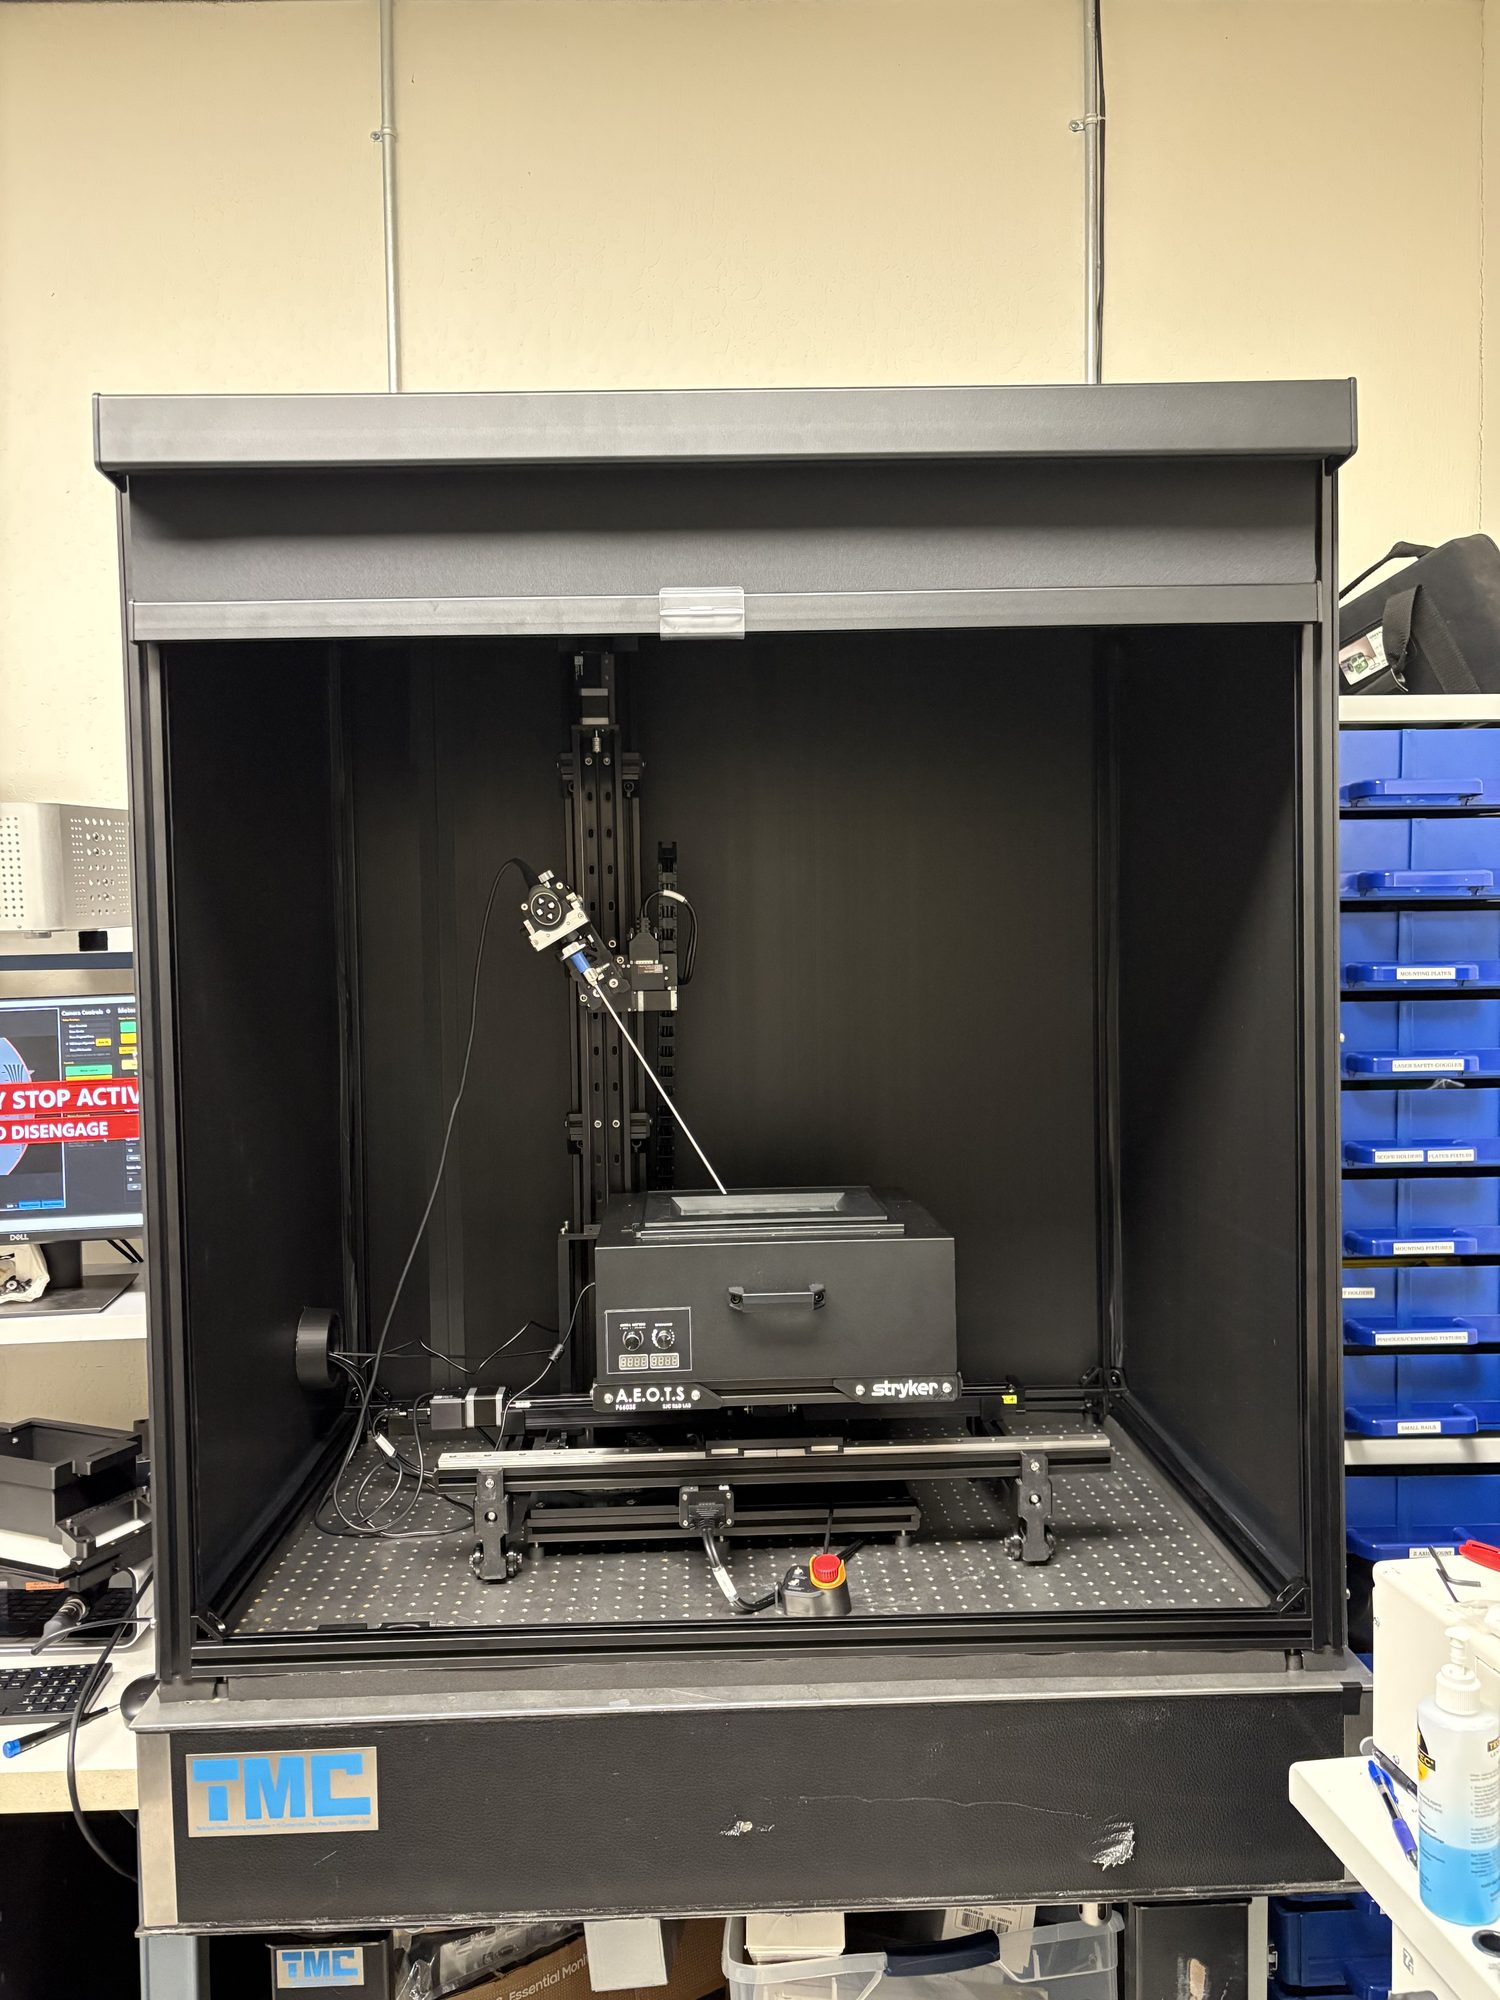
A blackout cage encloses the bench for complete optical isolation.
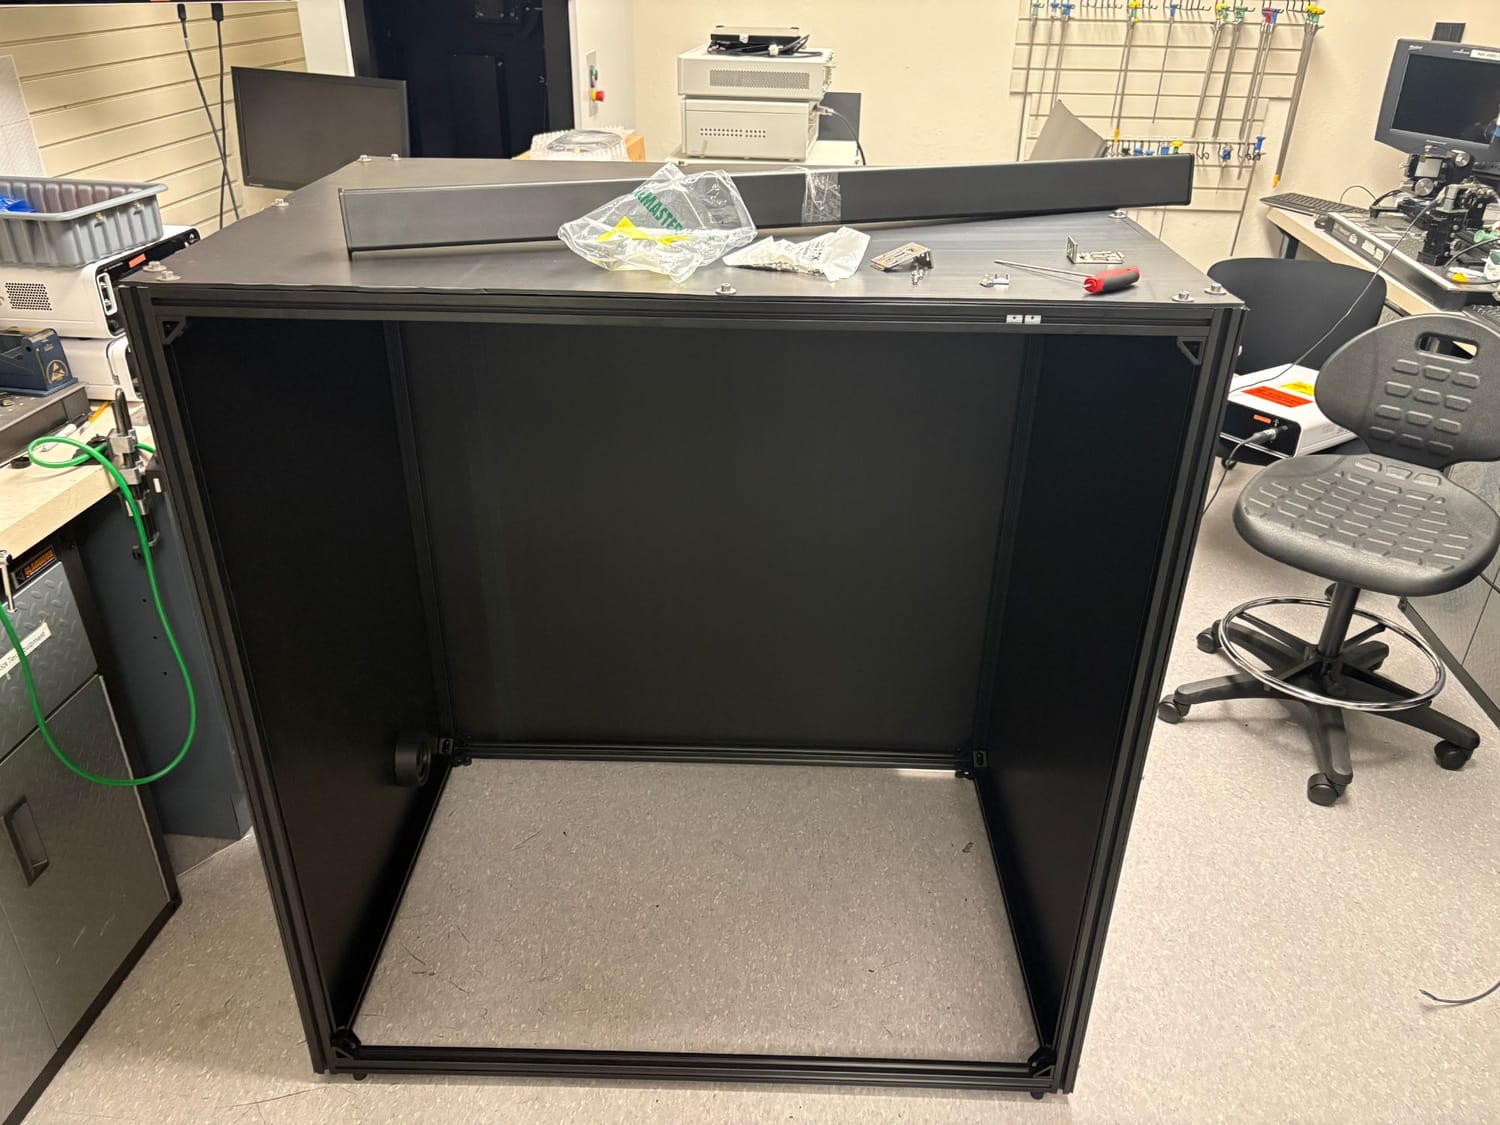
The blackout cage frame with black panels fitted on three sides, open at the front.
01.35 — CAGE FRAMEThe cage frame and panels during assembly.
The blackout cage with its door open, the scope fixture and target stage visible inside.
01.2 — BLACKOUT CAGEThe blackout cage open, with the scope fixture and target stage inside.
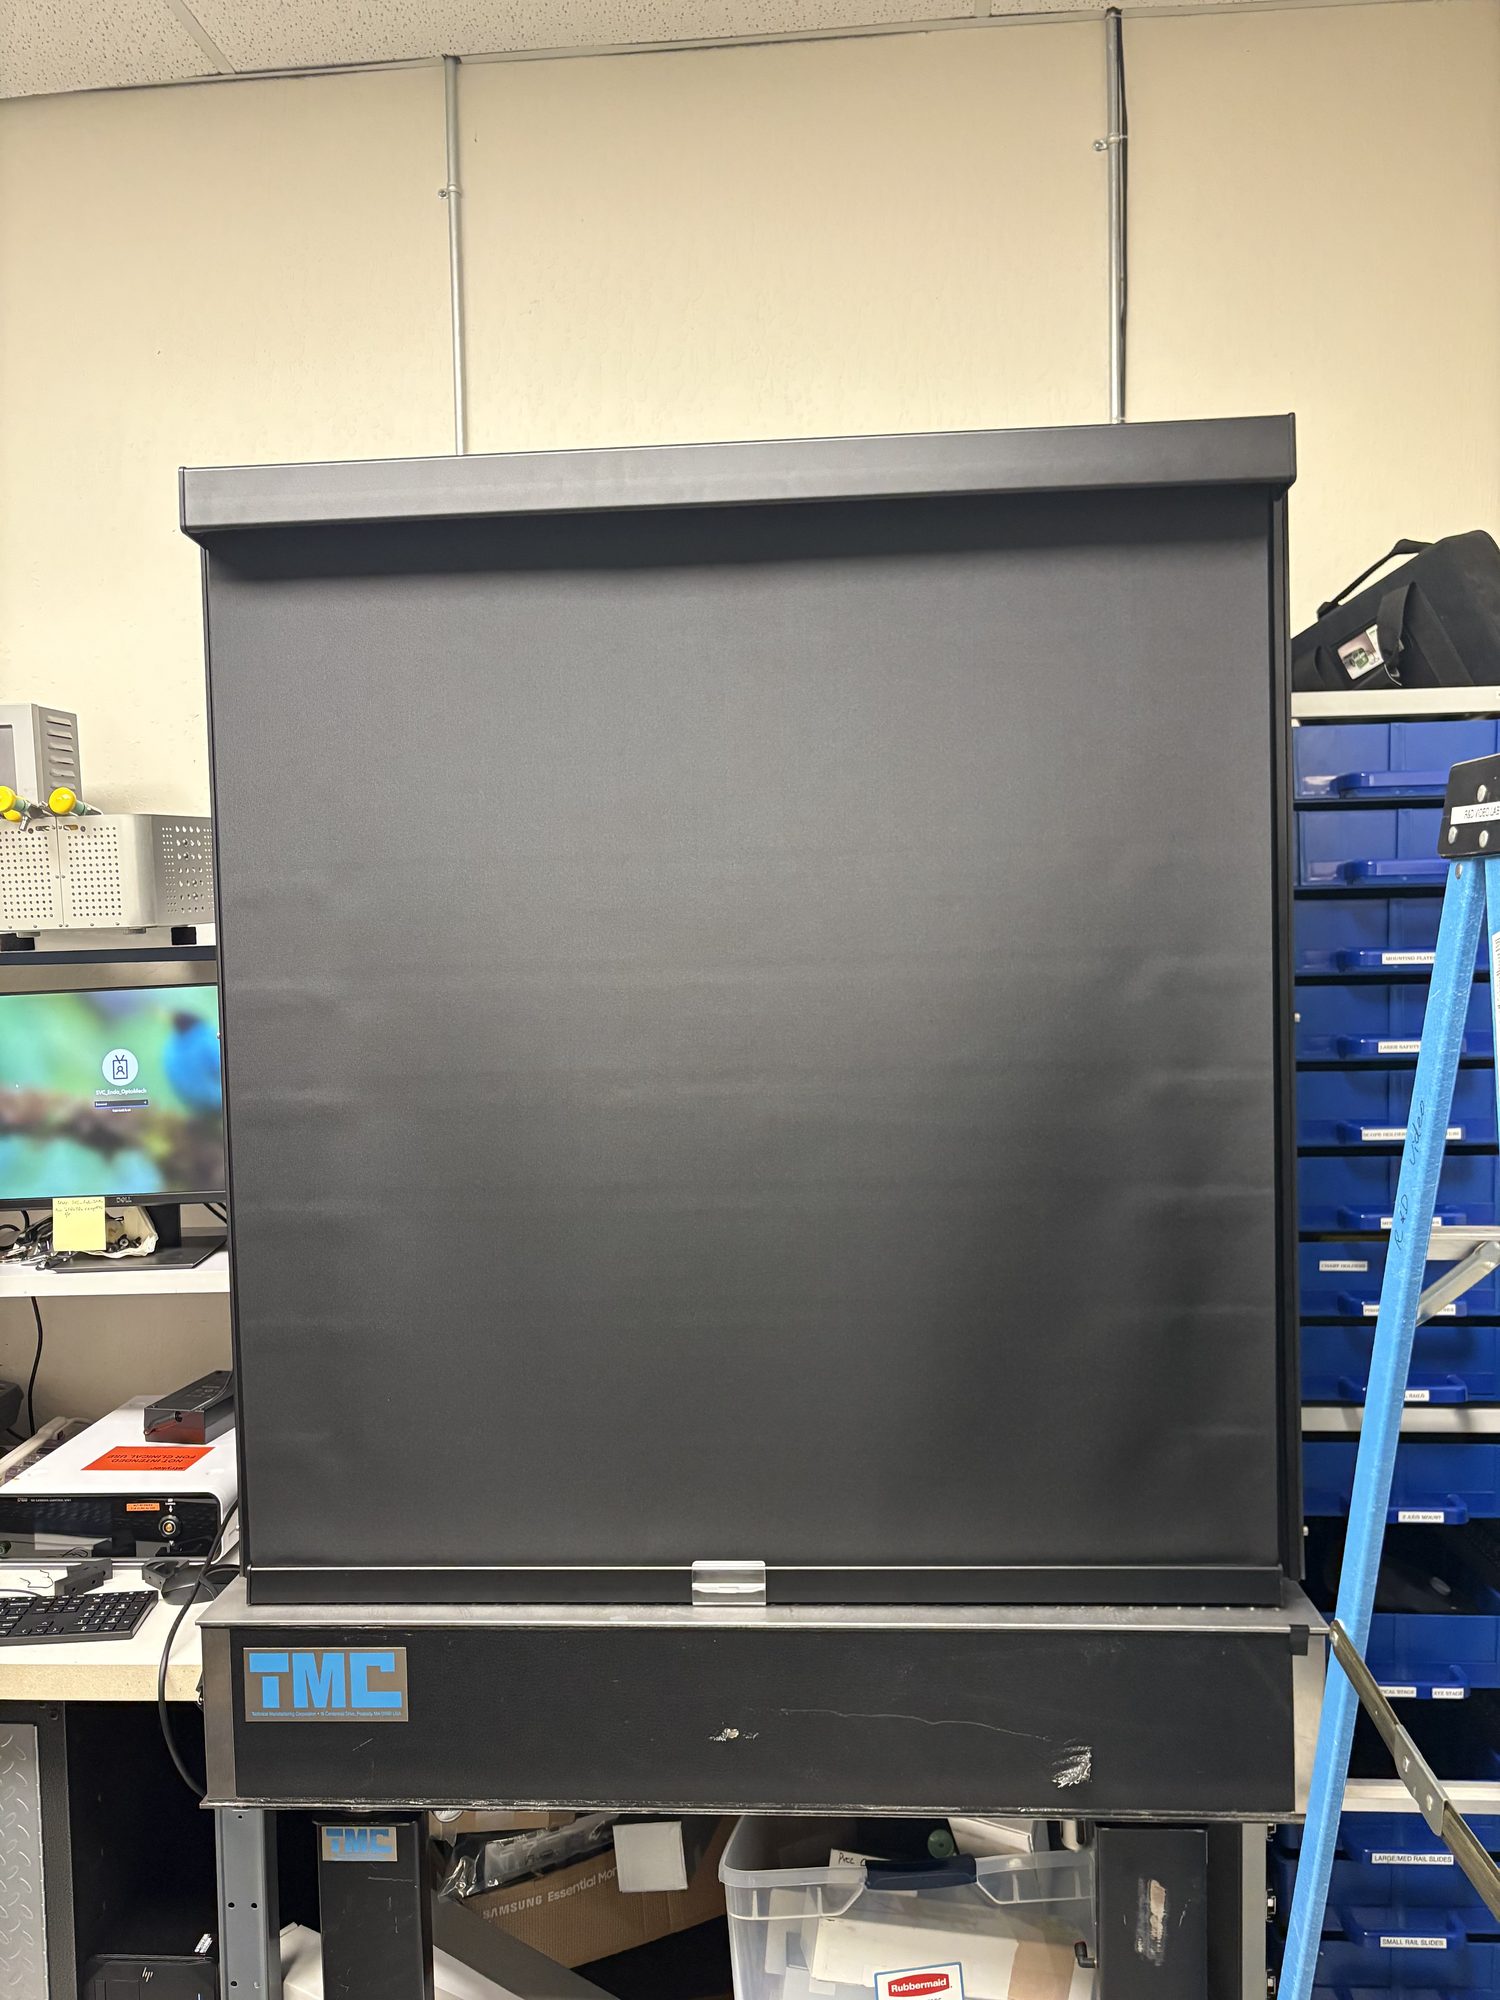
A matte black enclosure with its door closed on a laboratory bench.
01.14 — CAGE CLOSEDClosed for a run — complete optical isolation from ambient light.
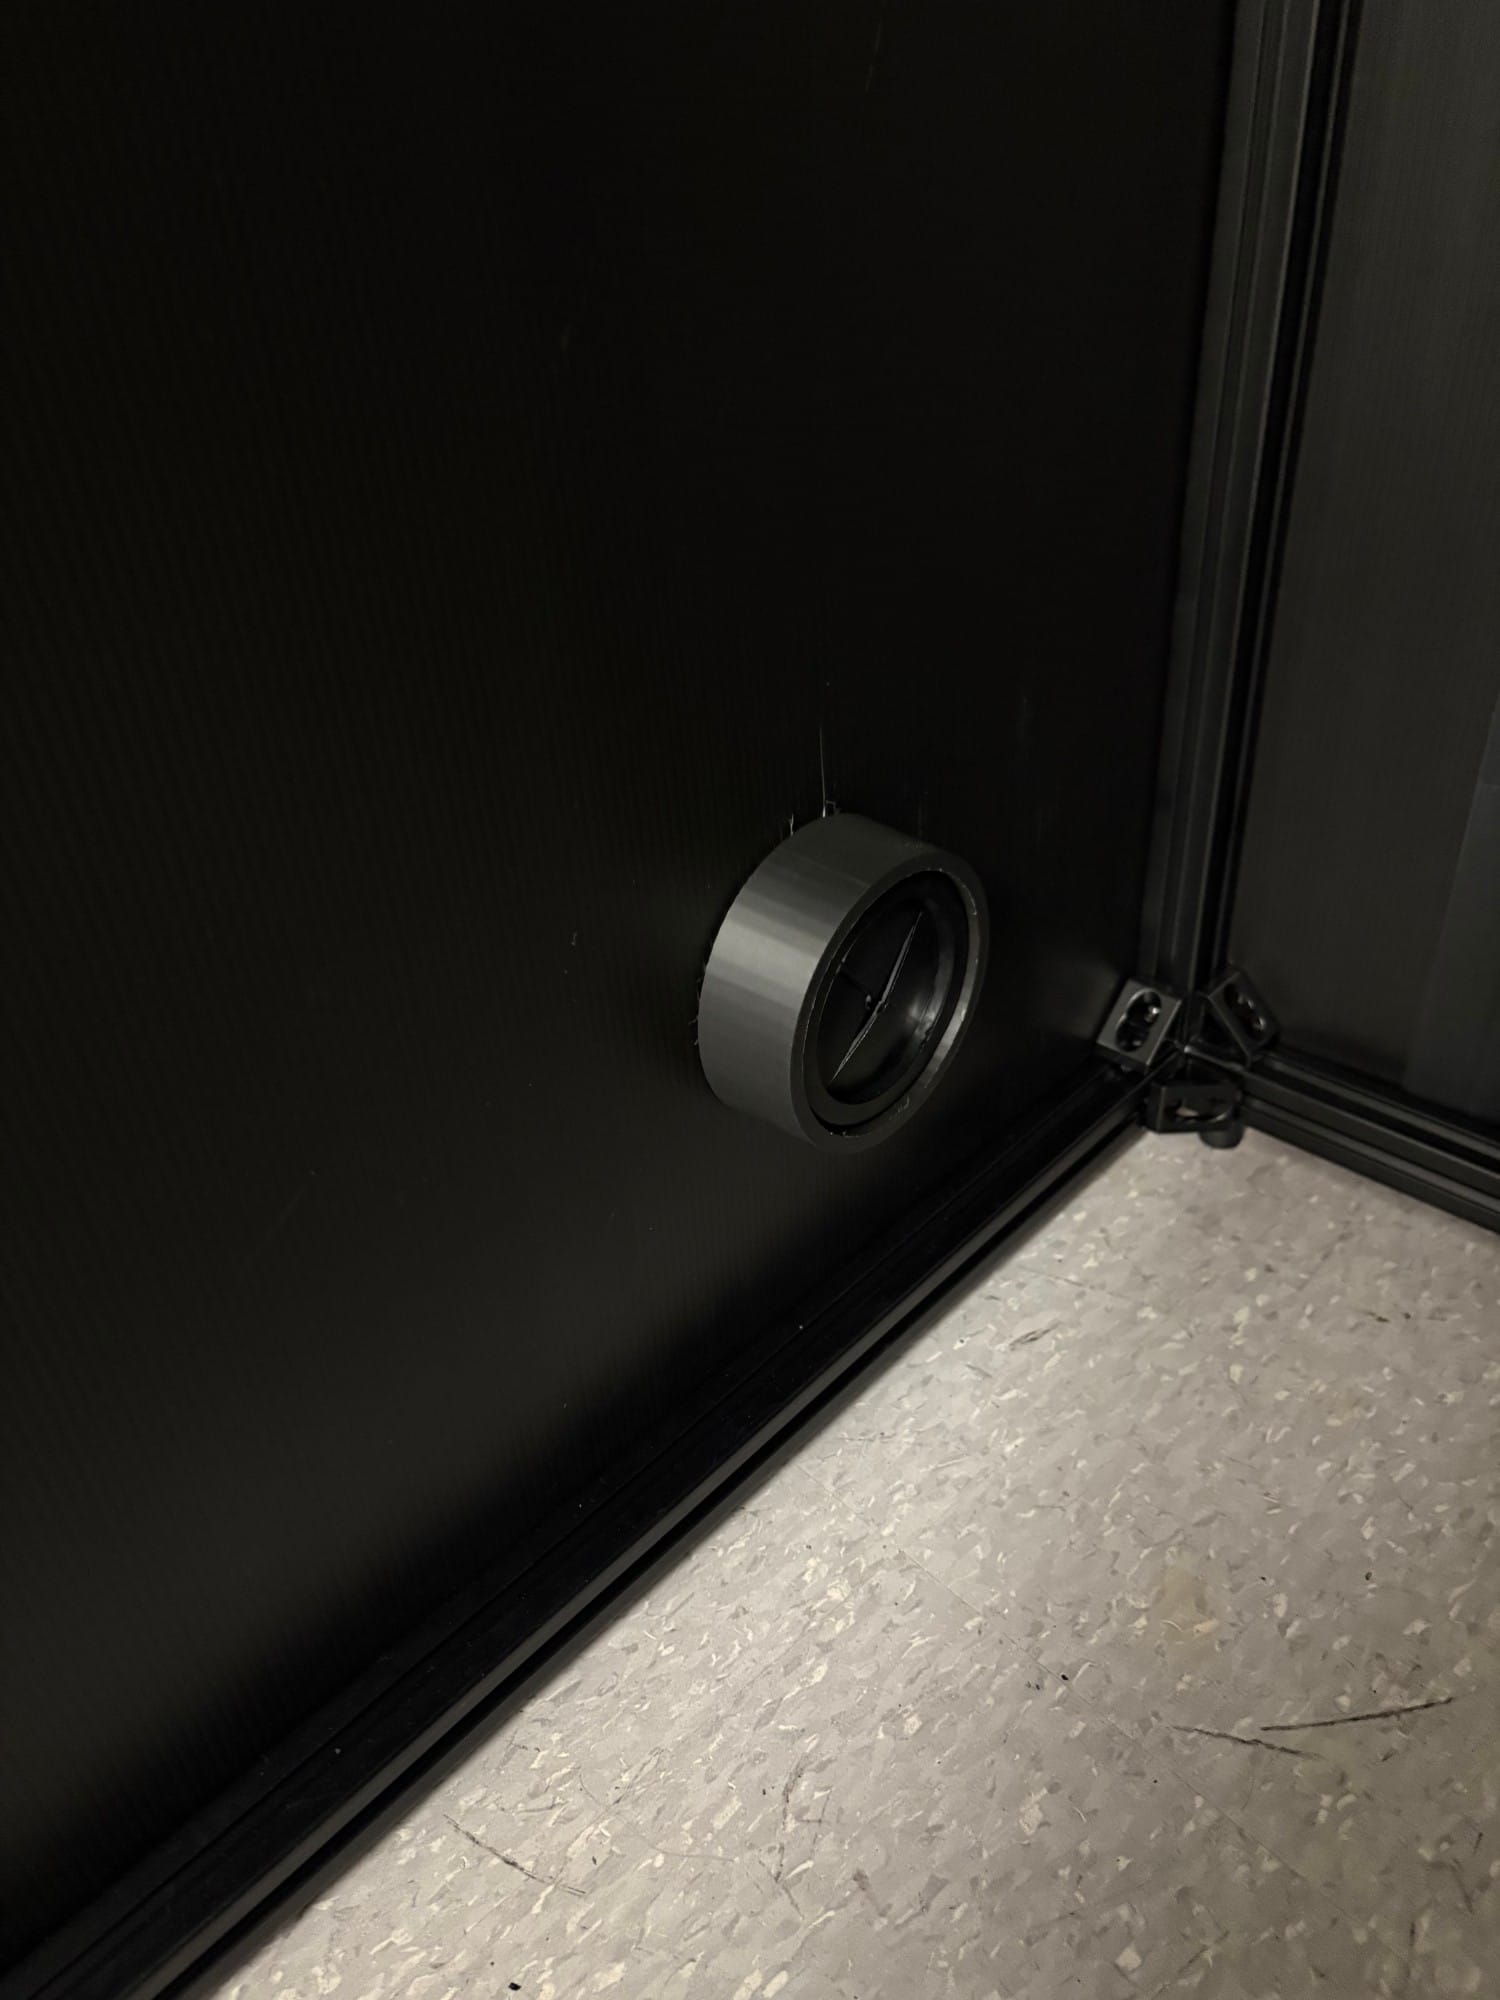
A round cable pass-through with a brush seal set into a black cage panel.
01.36 — CABLE PORTA cable passthrough in the cage wall.
06

Tower mounting

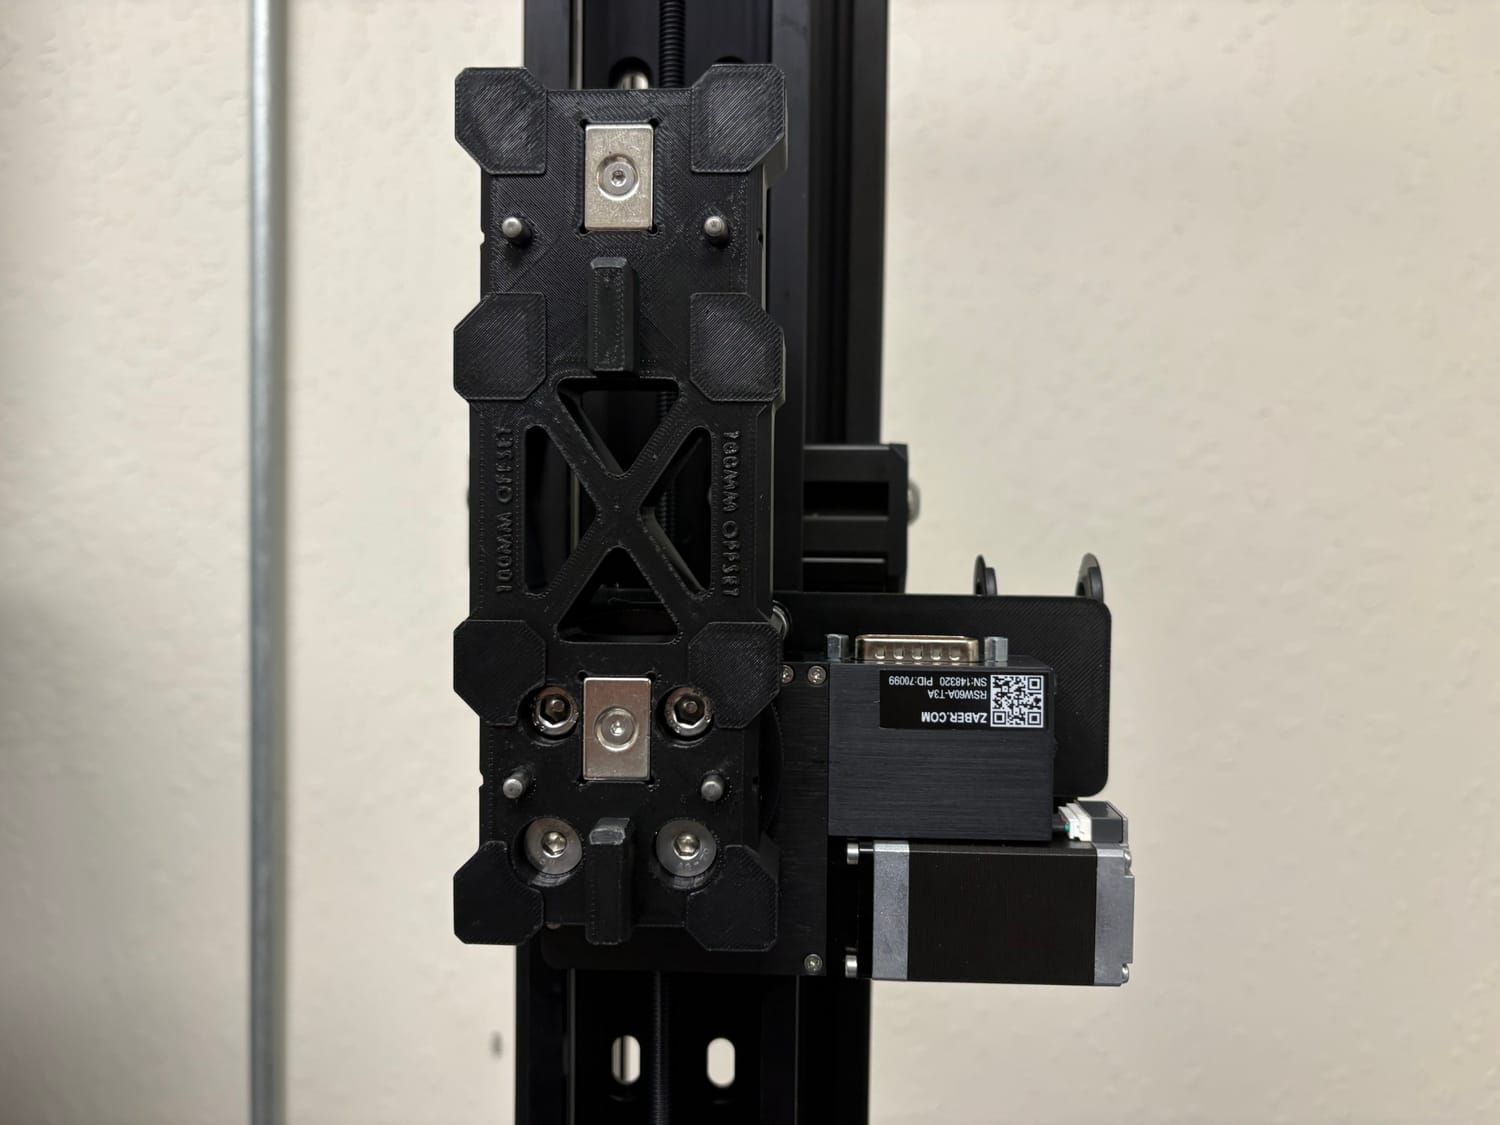
Tower retention force was too low.

The recession was increased to allow placement of two magnets.
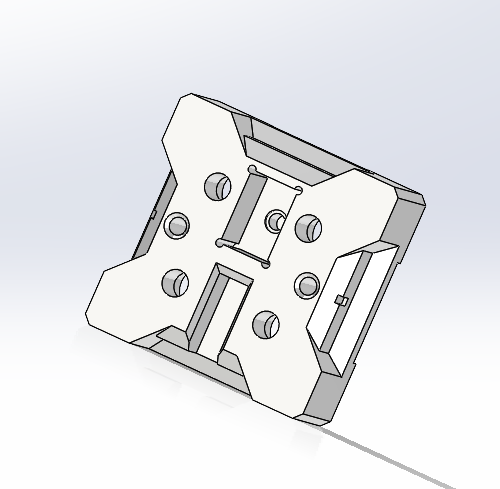
CAD detail of a recessed mounting pocket sized for two cylindrical magnets.
01.10 — TOWER MOUNTINGTower retention was too weak; the recess was deepened for a second magnet.
A black 3D-printed mounting plate on the vertical stage carriage, with two steel plates, locating pins and "100MM OFFSET" printed along its sides.
01.37 — TOWER MOUNTThe printed tower mount on the vertical carriage.
07

Build

Machined, printed, assembled and wired in-house.
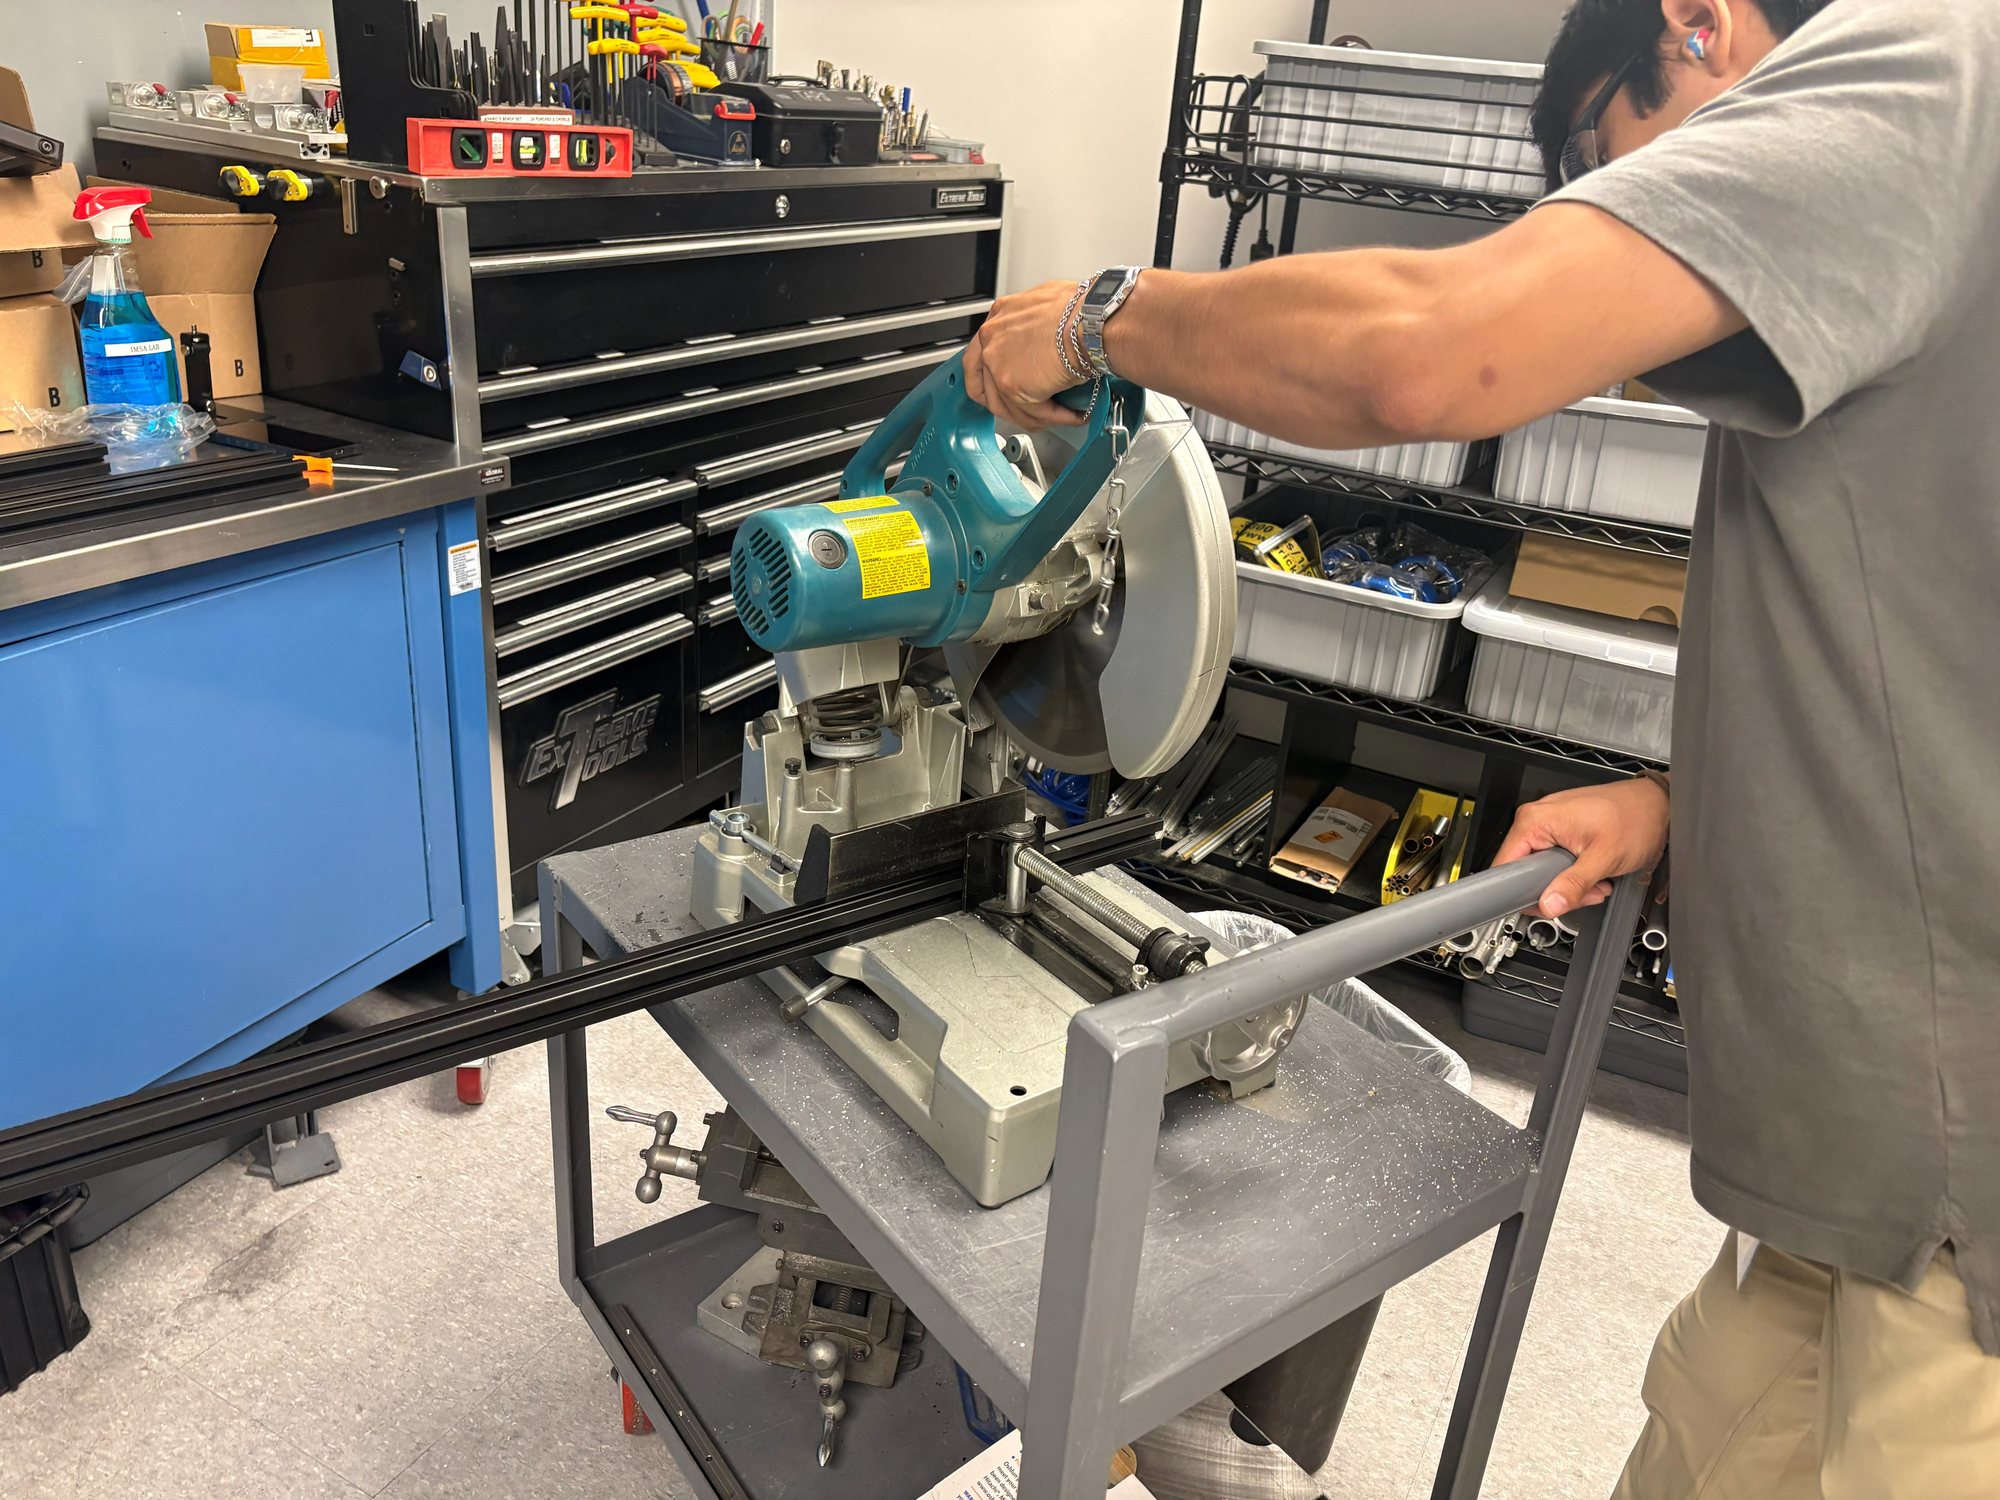
A person cutting an aluminium extrusion on a mitre saw at a workshop bench.
01.26 — CUTTING EXTRUSIONCutting extrusion to length.
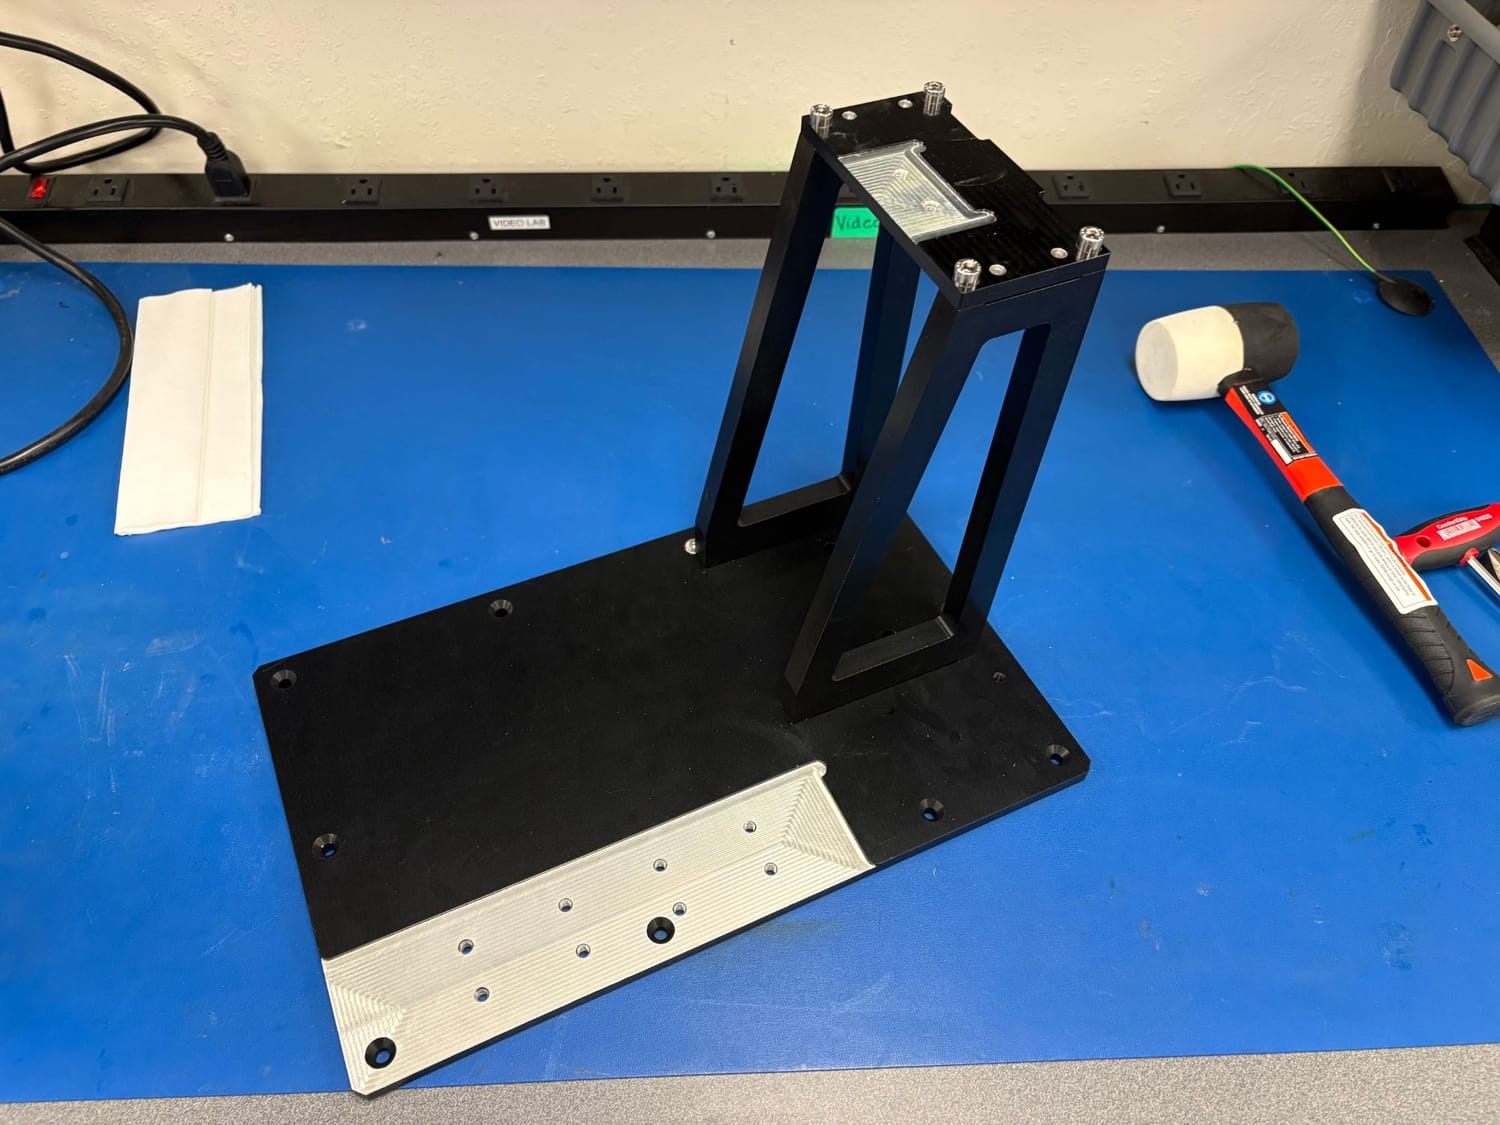
A black anodized base plate with a bare-aluminium machined pocket and a hollow tower support standing on it.
01.29 — MACHINED BASEAnodized base plate and tower support, with a machined pocket.
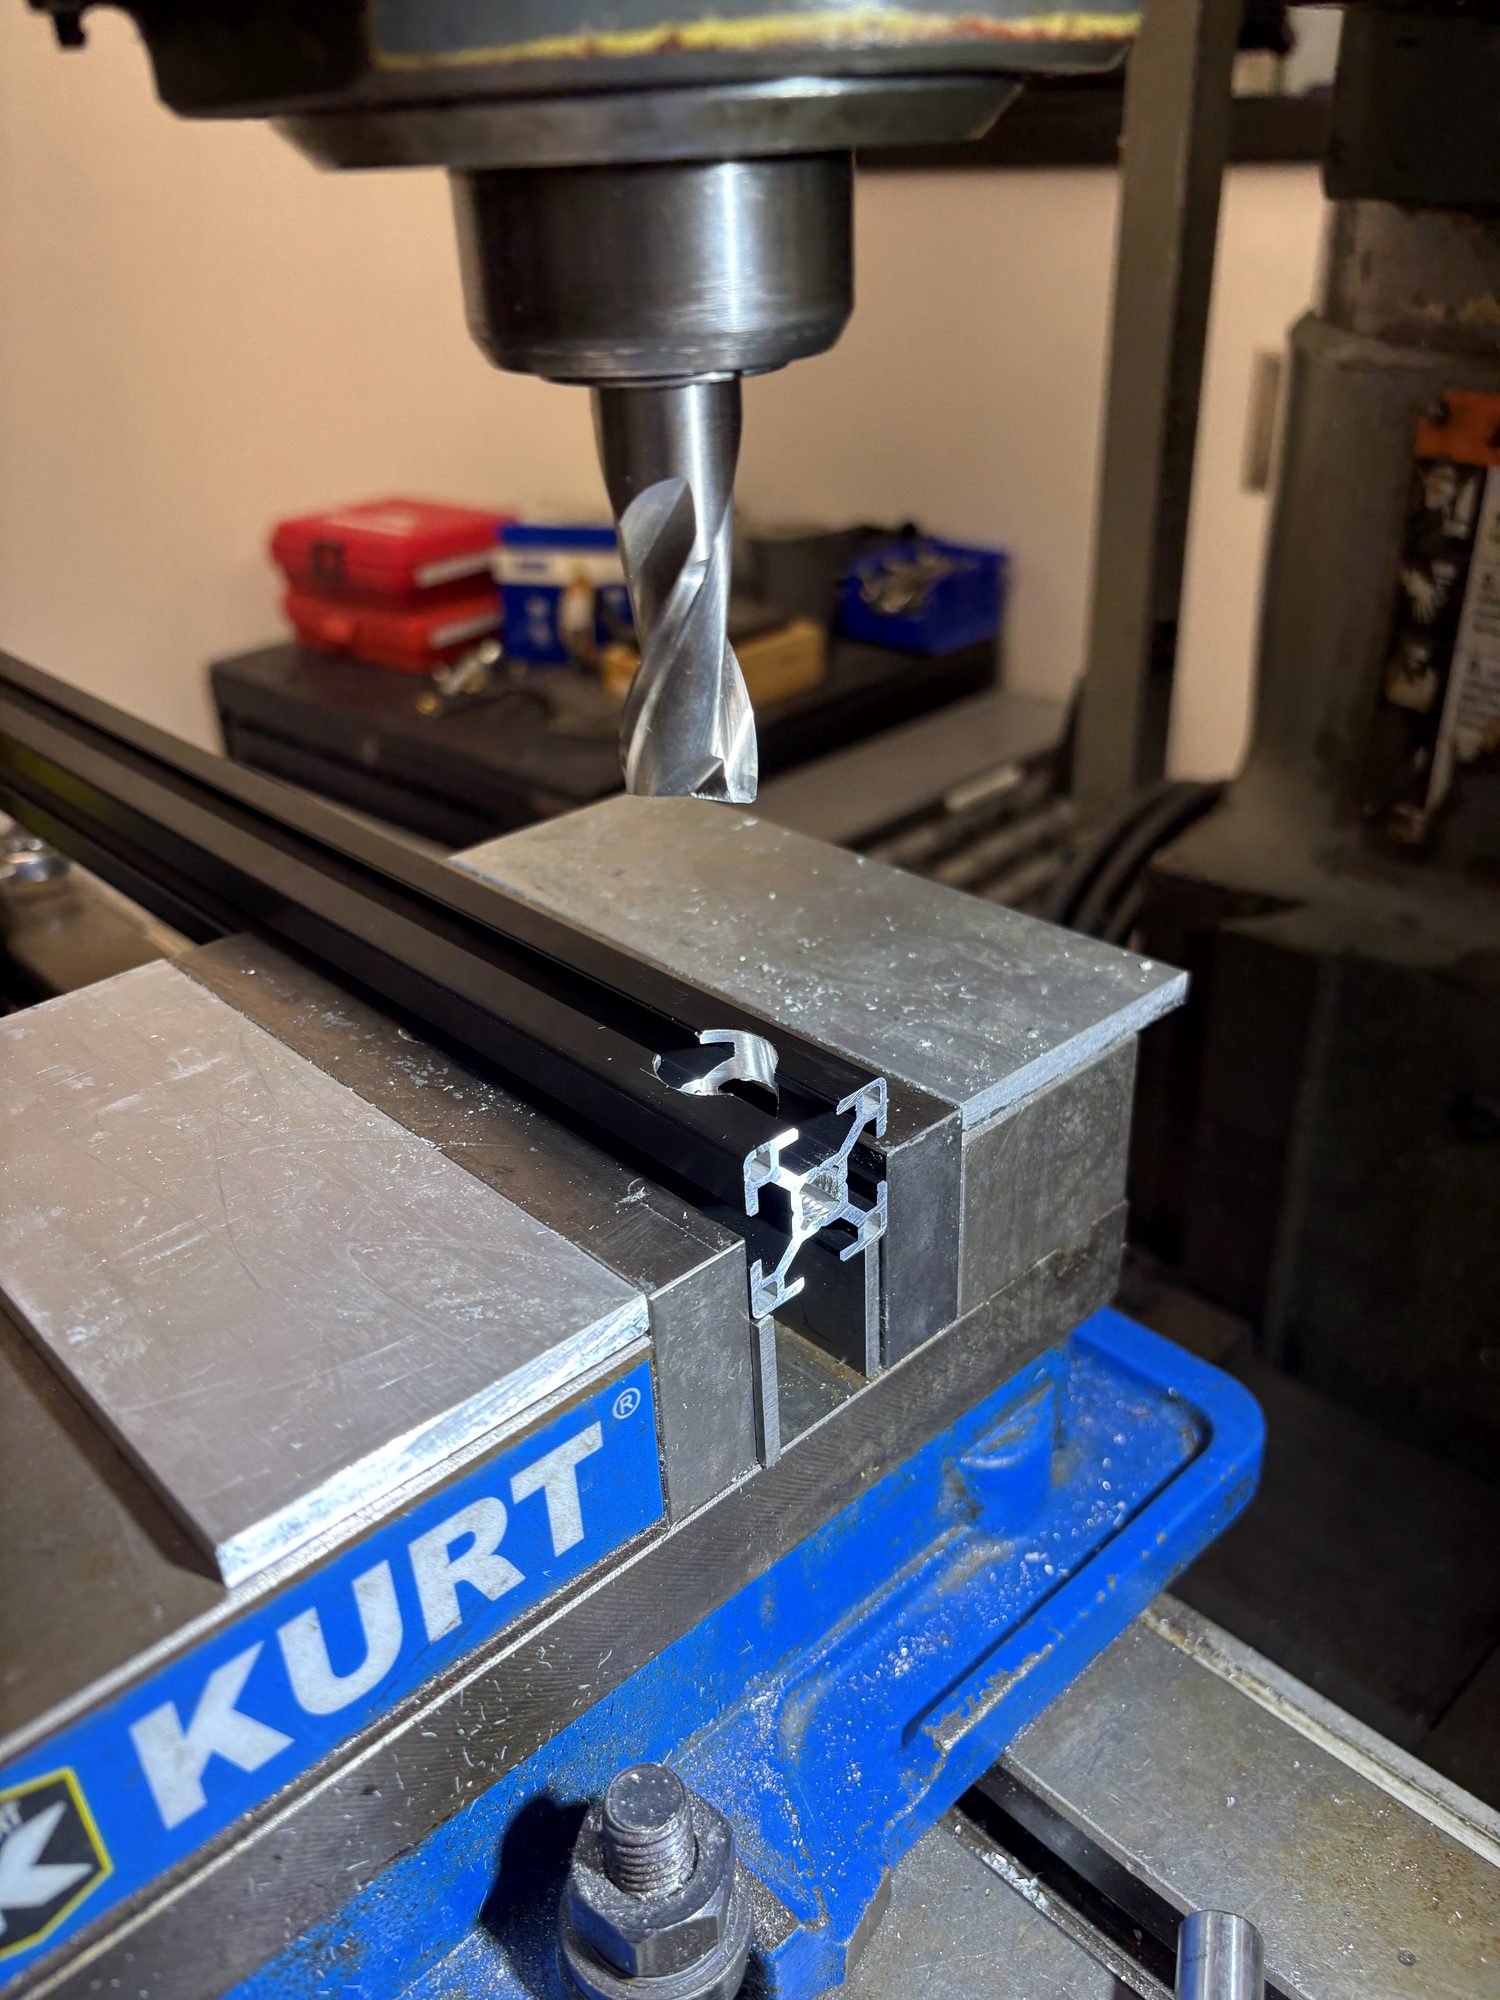
An end mill cutting an aluminium extrusion held in a milling vice.
01.11 — MACHININGMachining fixture components in-house.
A dial indicator on a magnetic base checking a part clamped in a vice on a surface plate.
01.12 — ALIGNMENTIndicating in before cutting — the alignment features had to be right.
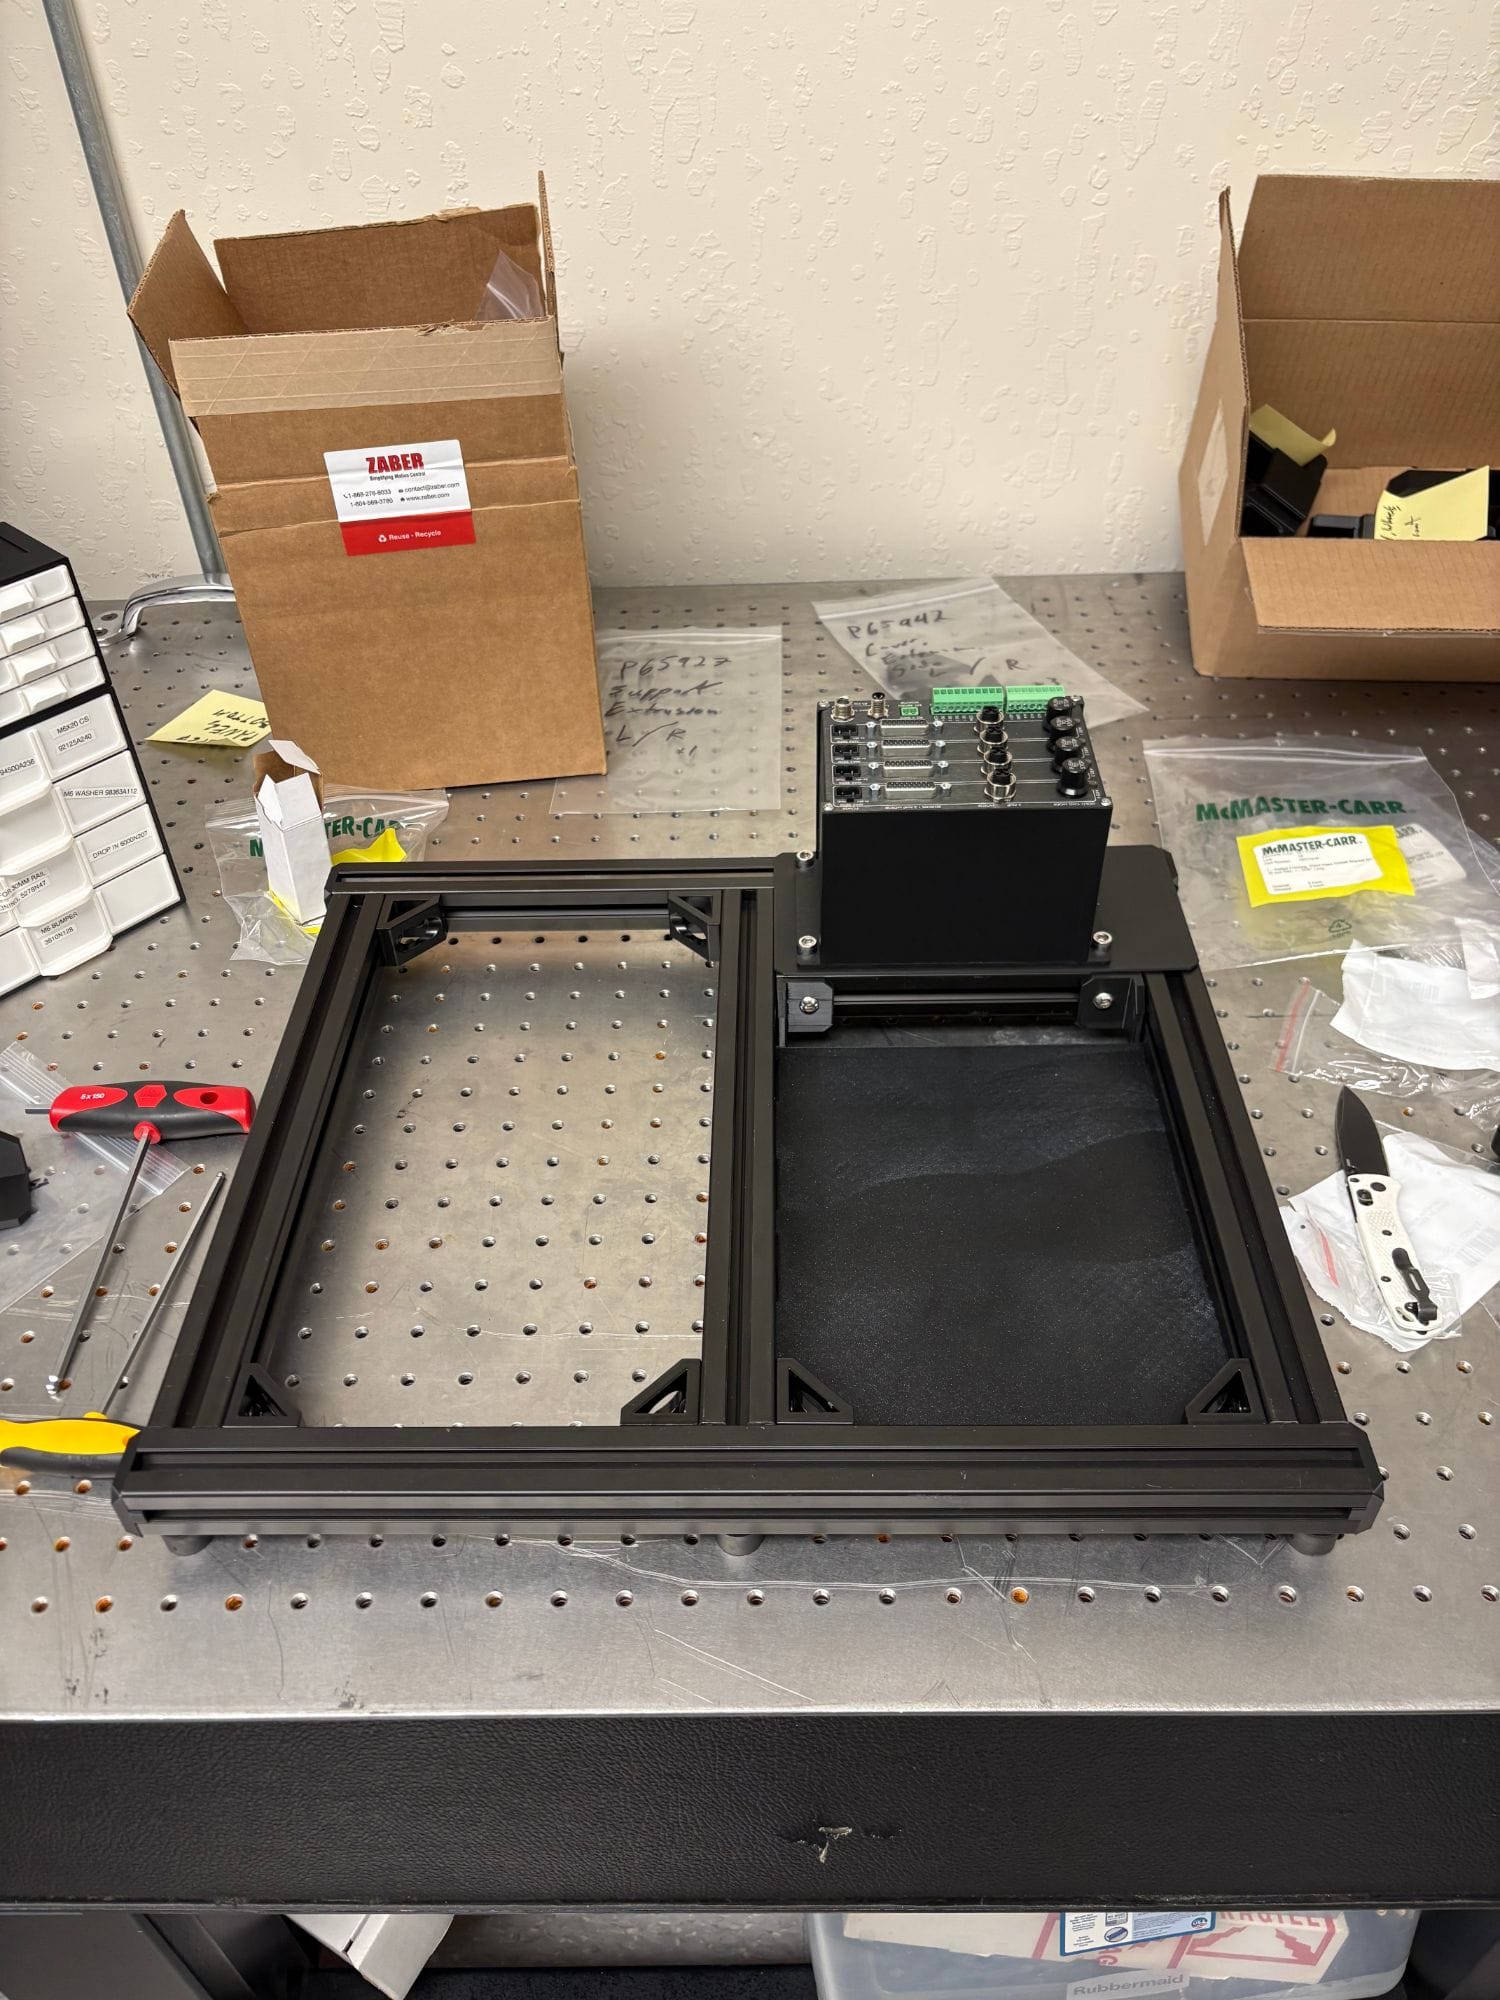
The two-bay subframe on an optical table with the motion controller mounted at the back of one bay.
01.32 — CONTROLLER BAYThe subframe with the motion controller mounted.
The vertical tower stage standing on its base plate beside the controller, before the gantry stage was fitted.
01.28 — TOWER AND BASEThe tower on its base plate, before the gantry stage went on.
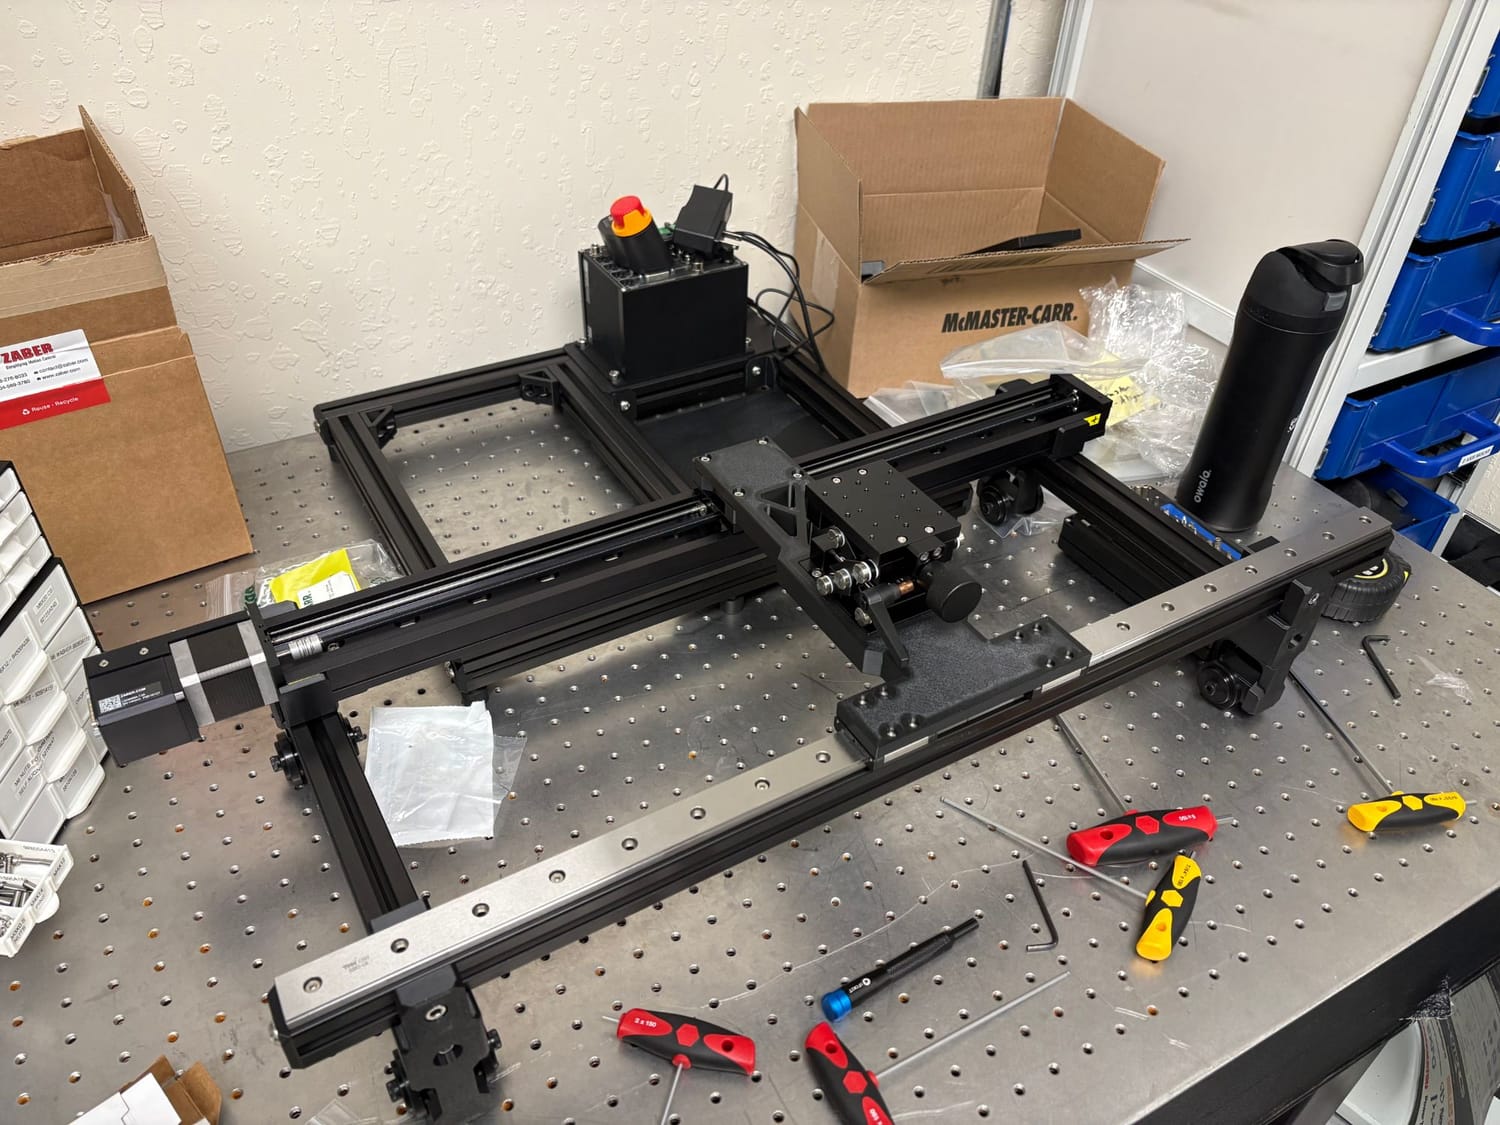
The gantry stage on its rails with a stepper-driven axis and manual stages on the carriage.
01.34 — GANTRY STAGEThe gantry stage on its rails, with the manual stages on the carriage.
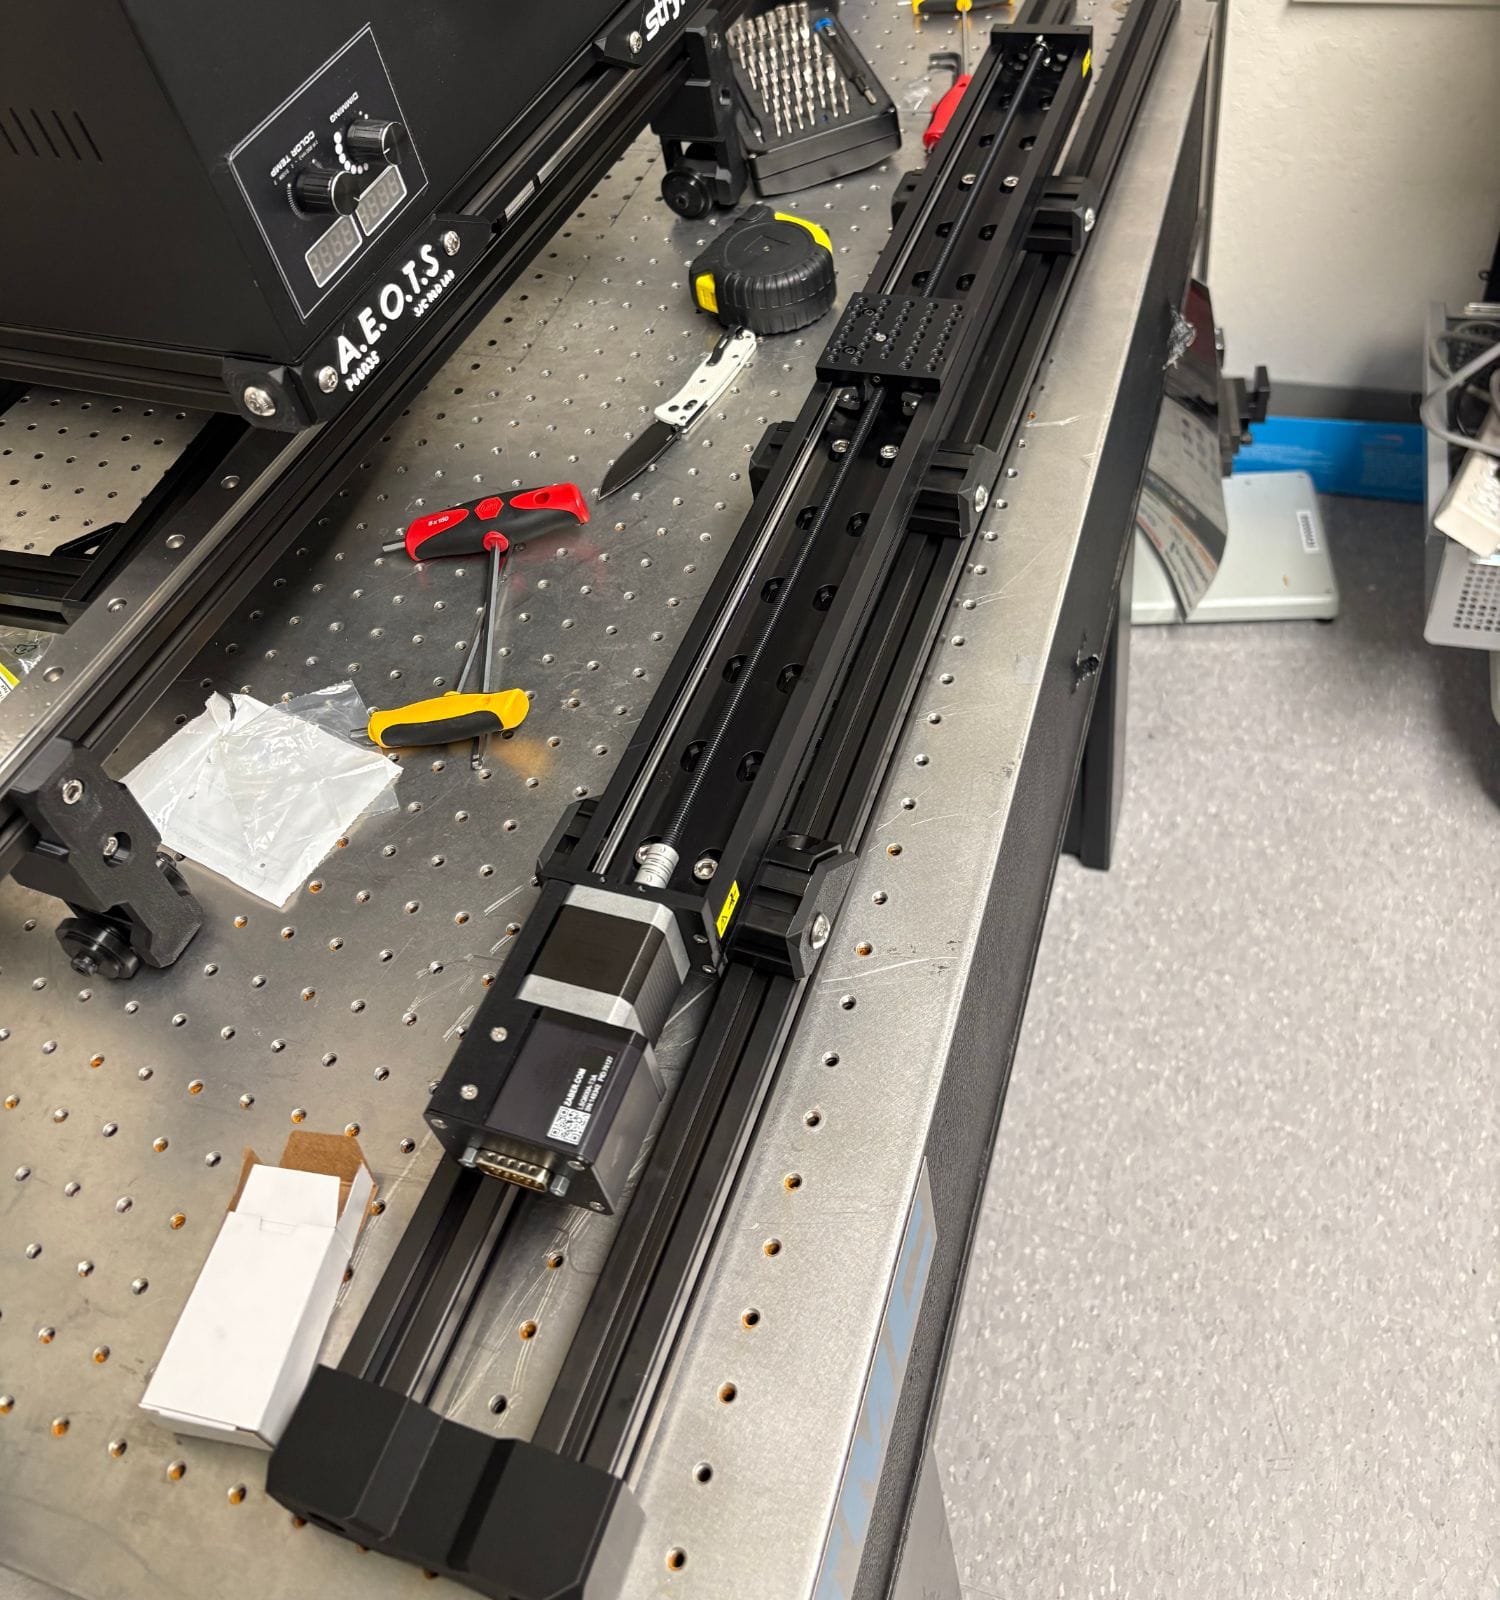
A long motorized linear stage with its stepper motor lying on an optical table.
01.33 — LINEAR STAGEA motorized linear stage before installation.
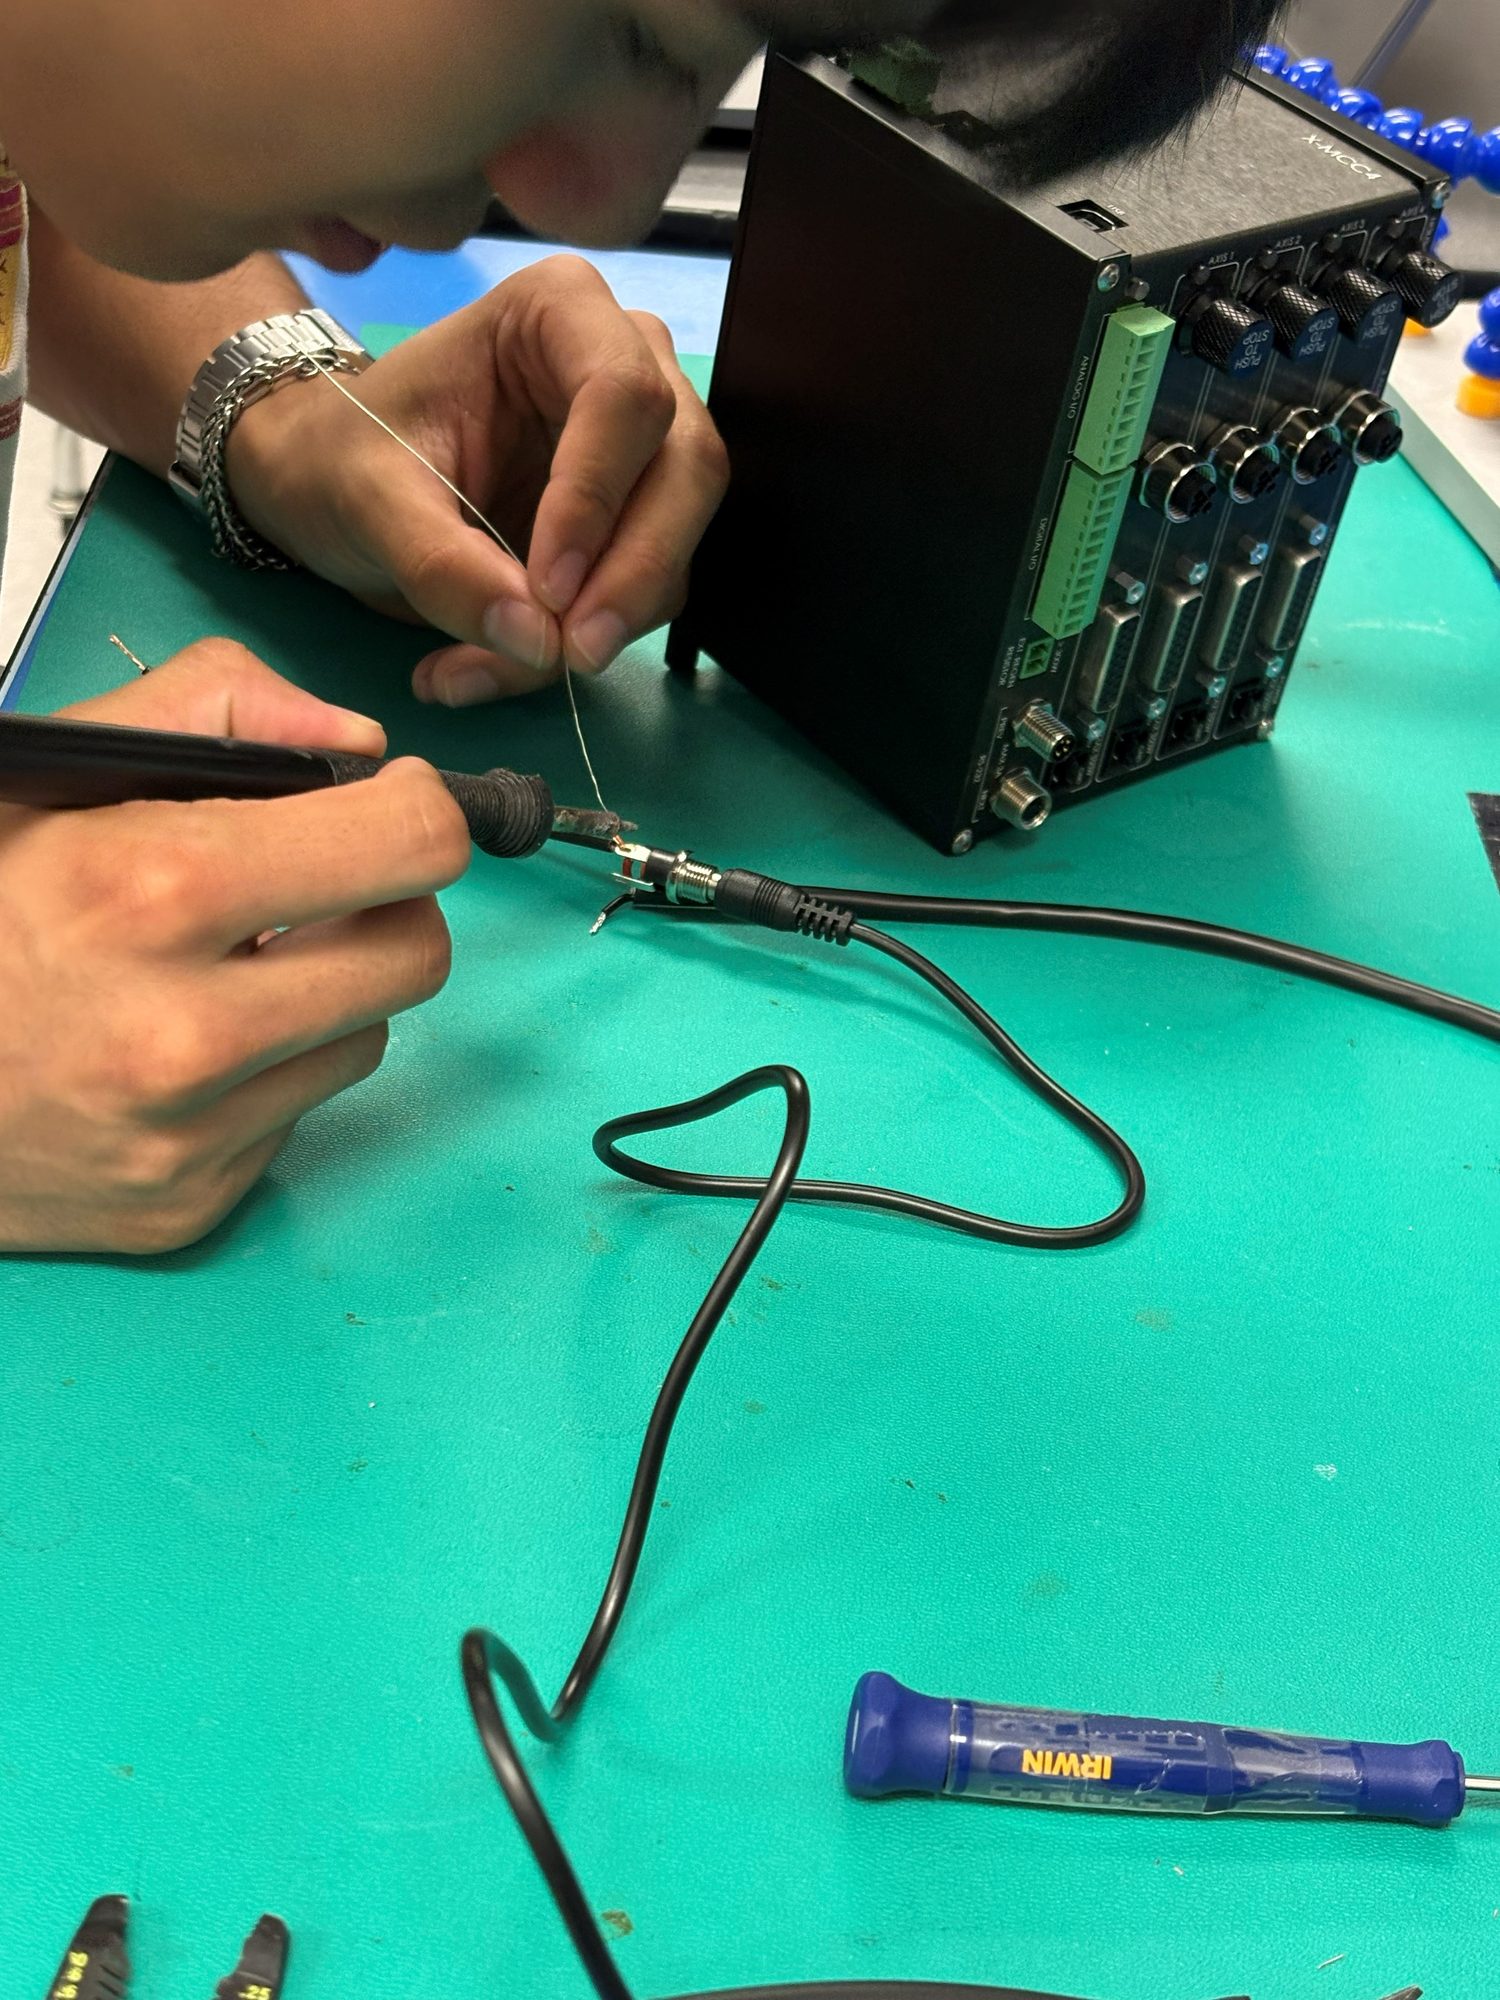
Hands soldering a connector at a bench beside an equipment enclosure with terminal blocks.
01.13 — WIRINGWiring the controller: the build included the electrical side, not just the mechanics.
Confidentiality

Proprietary information withheld.

Let’s talk.

Open to co-op, internship and project conversations in mechanical design, product development and R&D.