Upcycling fabric scraps into beads that can be used in jewelry designs or sold wholesale.
- Mechanical Engineer
- Generate Product Development Studio
- September 2025 – December 2025
- Onshape, SLA resin, FDM + heat-set inserts, Tool steel (Xometry), Lead screw + linear rail, 8020 frame
- Generate product-development team
- Product Development · Sustainability · Automation / Motion Systems · Tooling · Additive Manufacturing
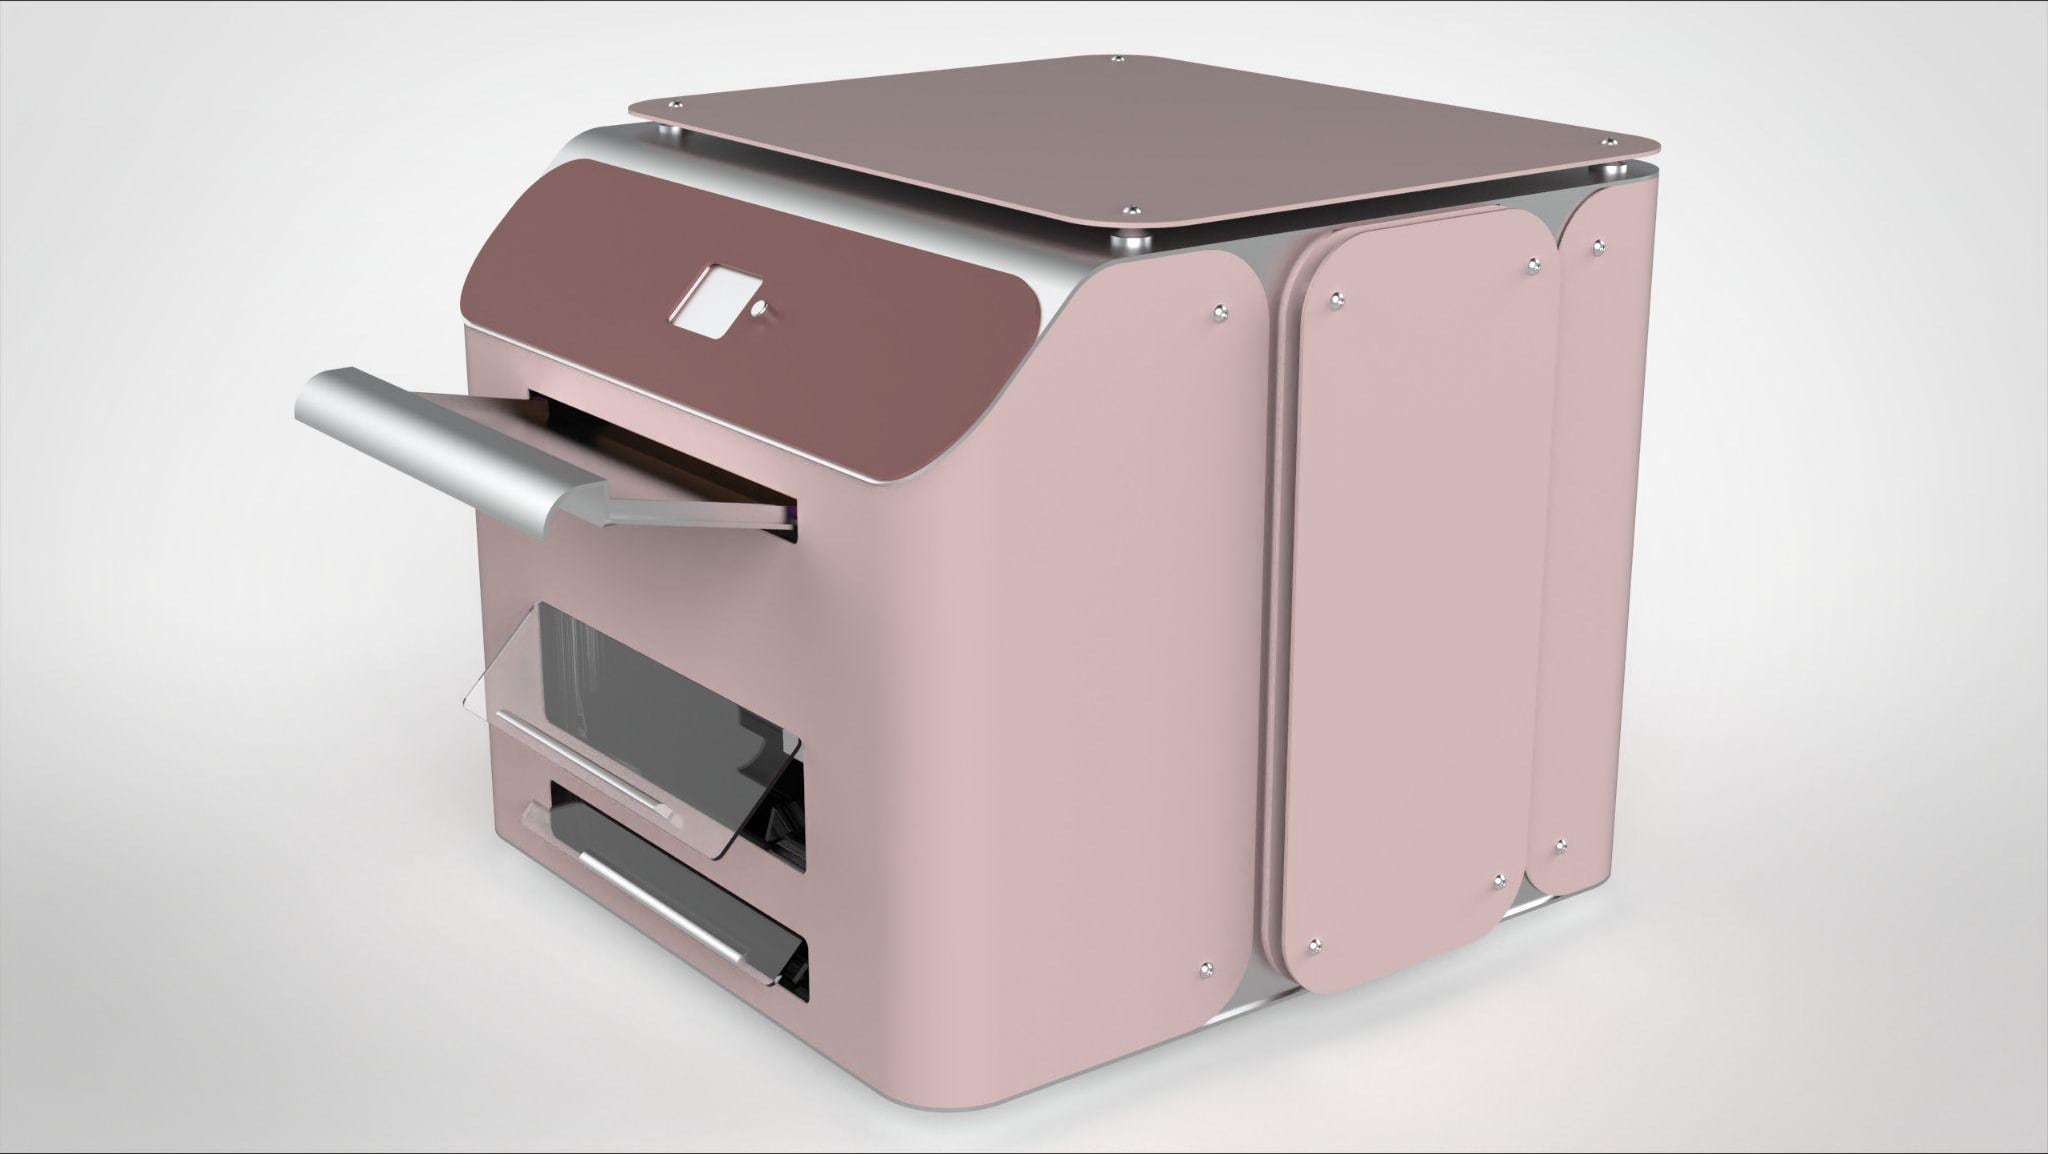
Specifications
- Heating, molding, cutting, and dispensing
- Two fabric layers with a PC-ABS hot glue sheet sandwiched between them
- Heated plate maintained at approximately 90°C
- Five-pointed flower, cut around a molded dome
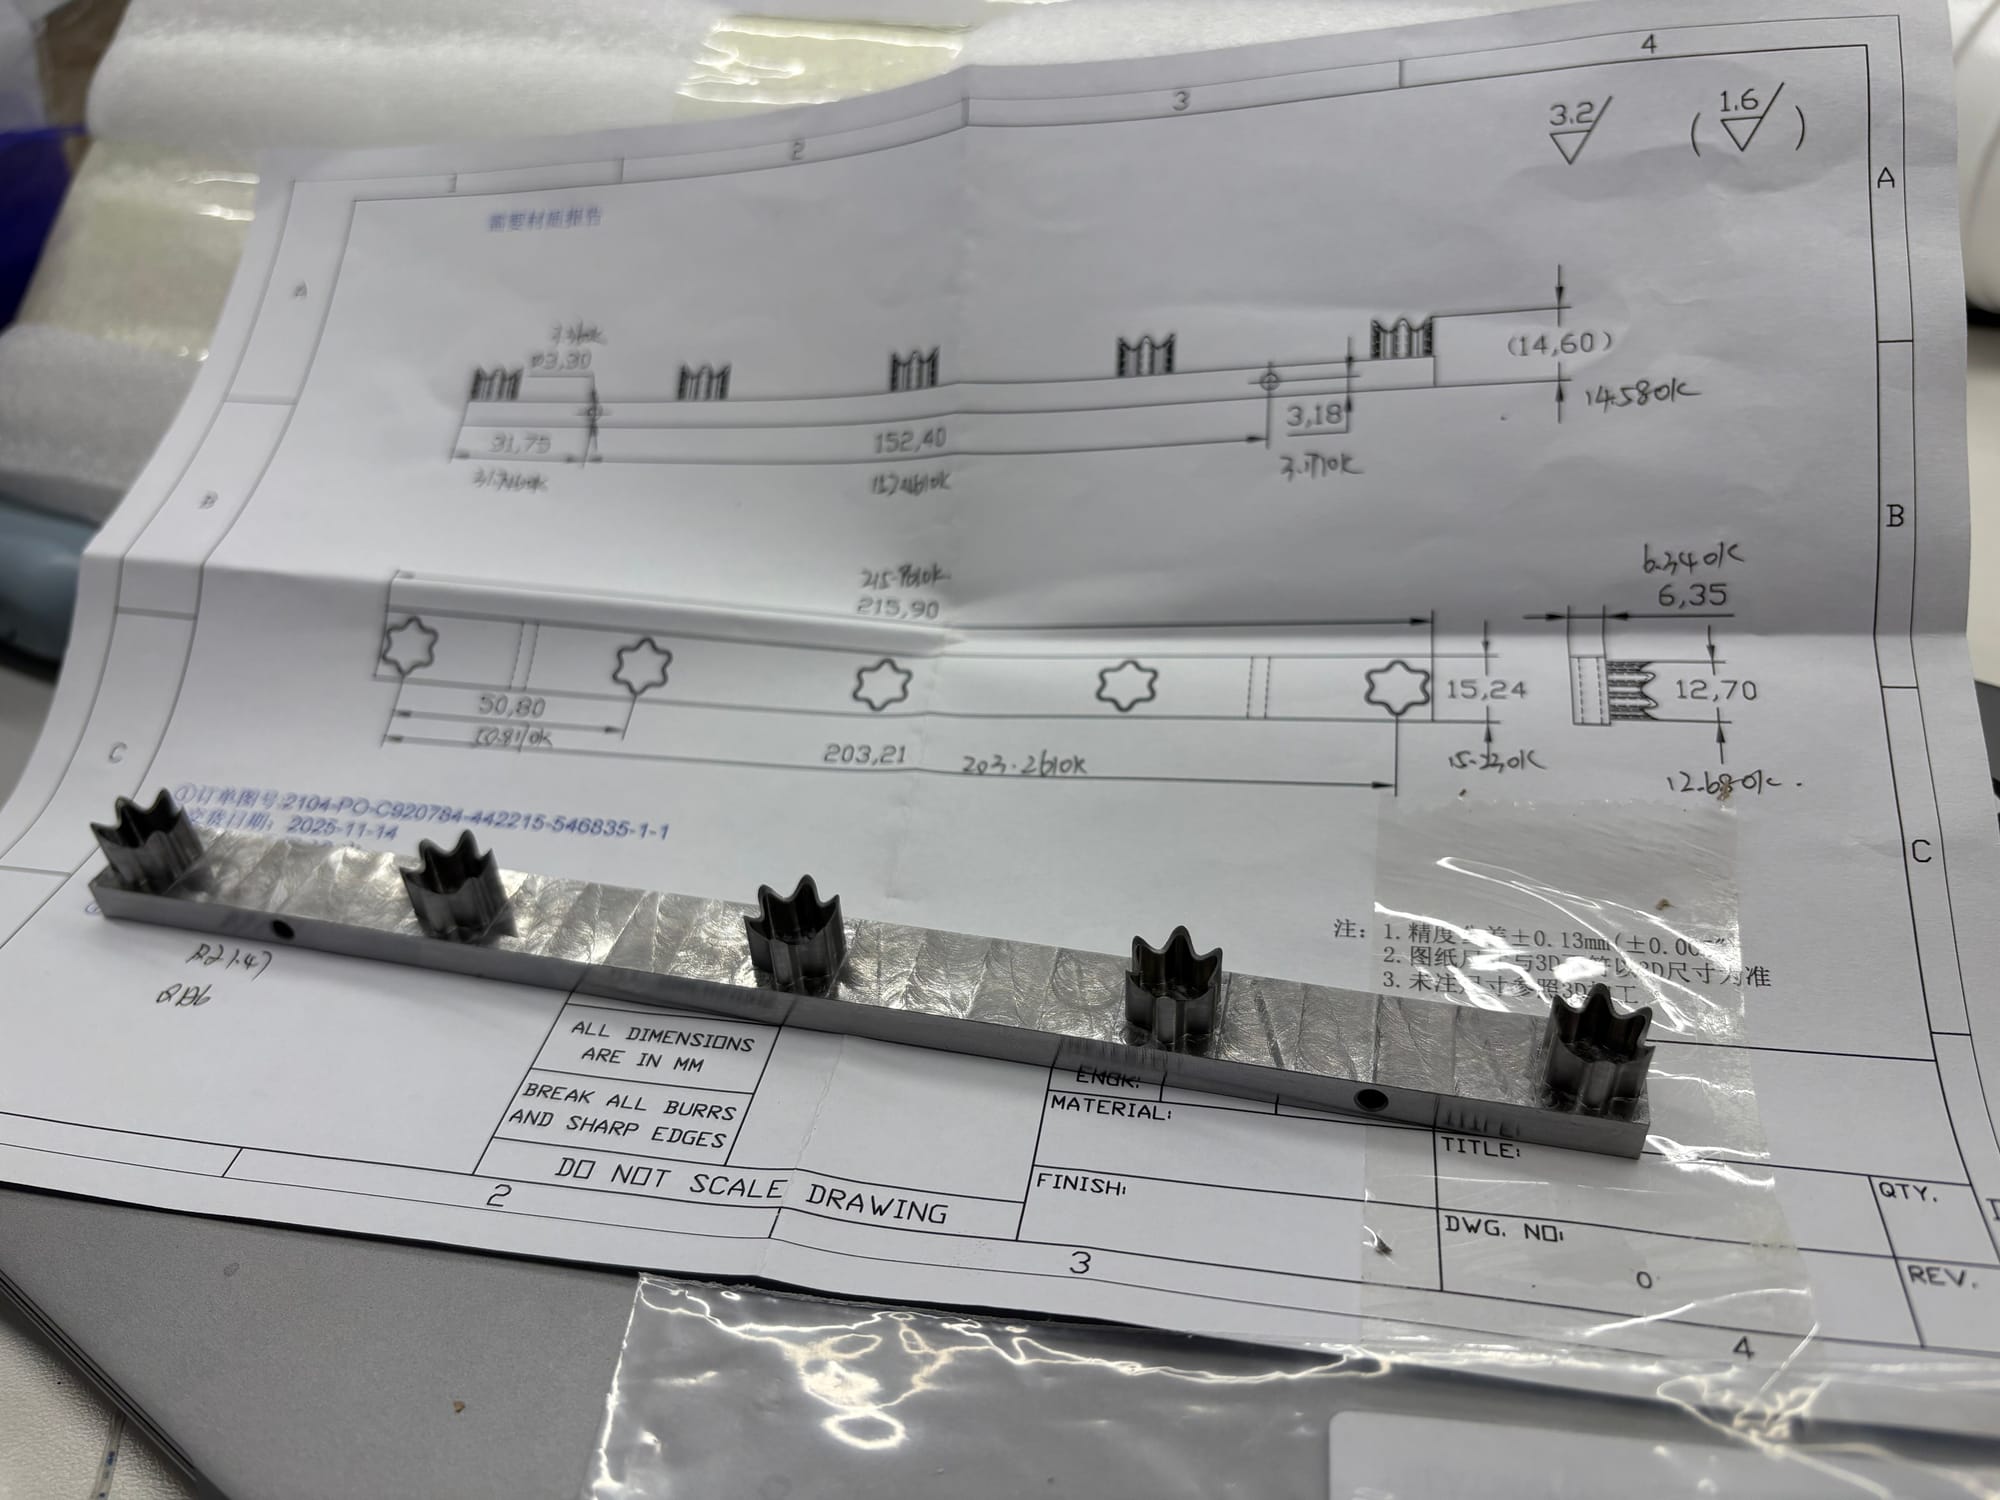
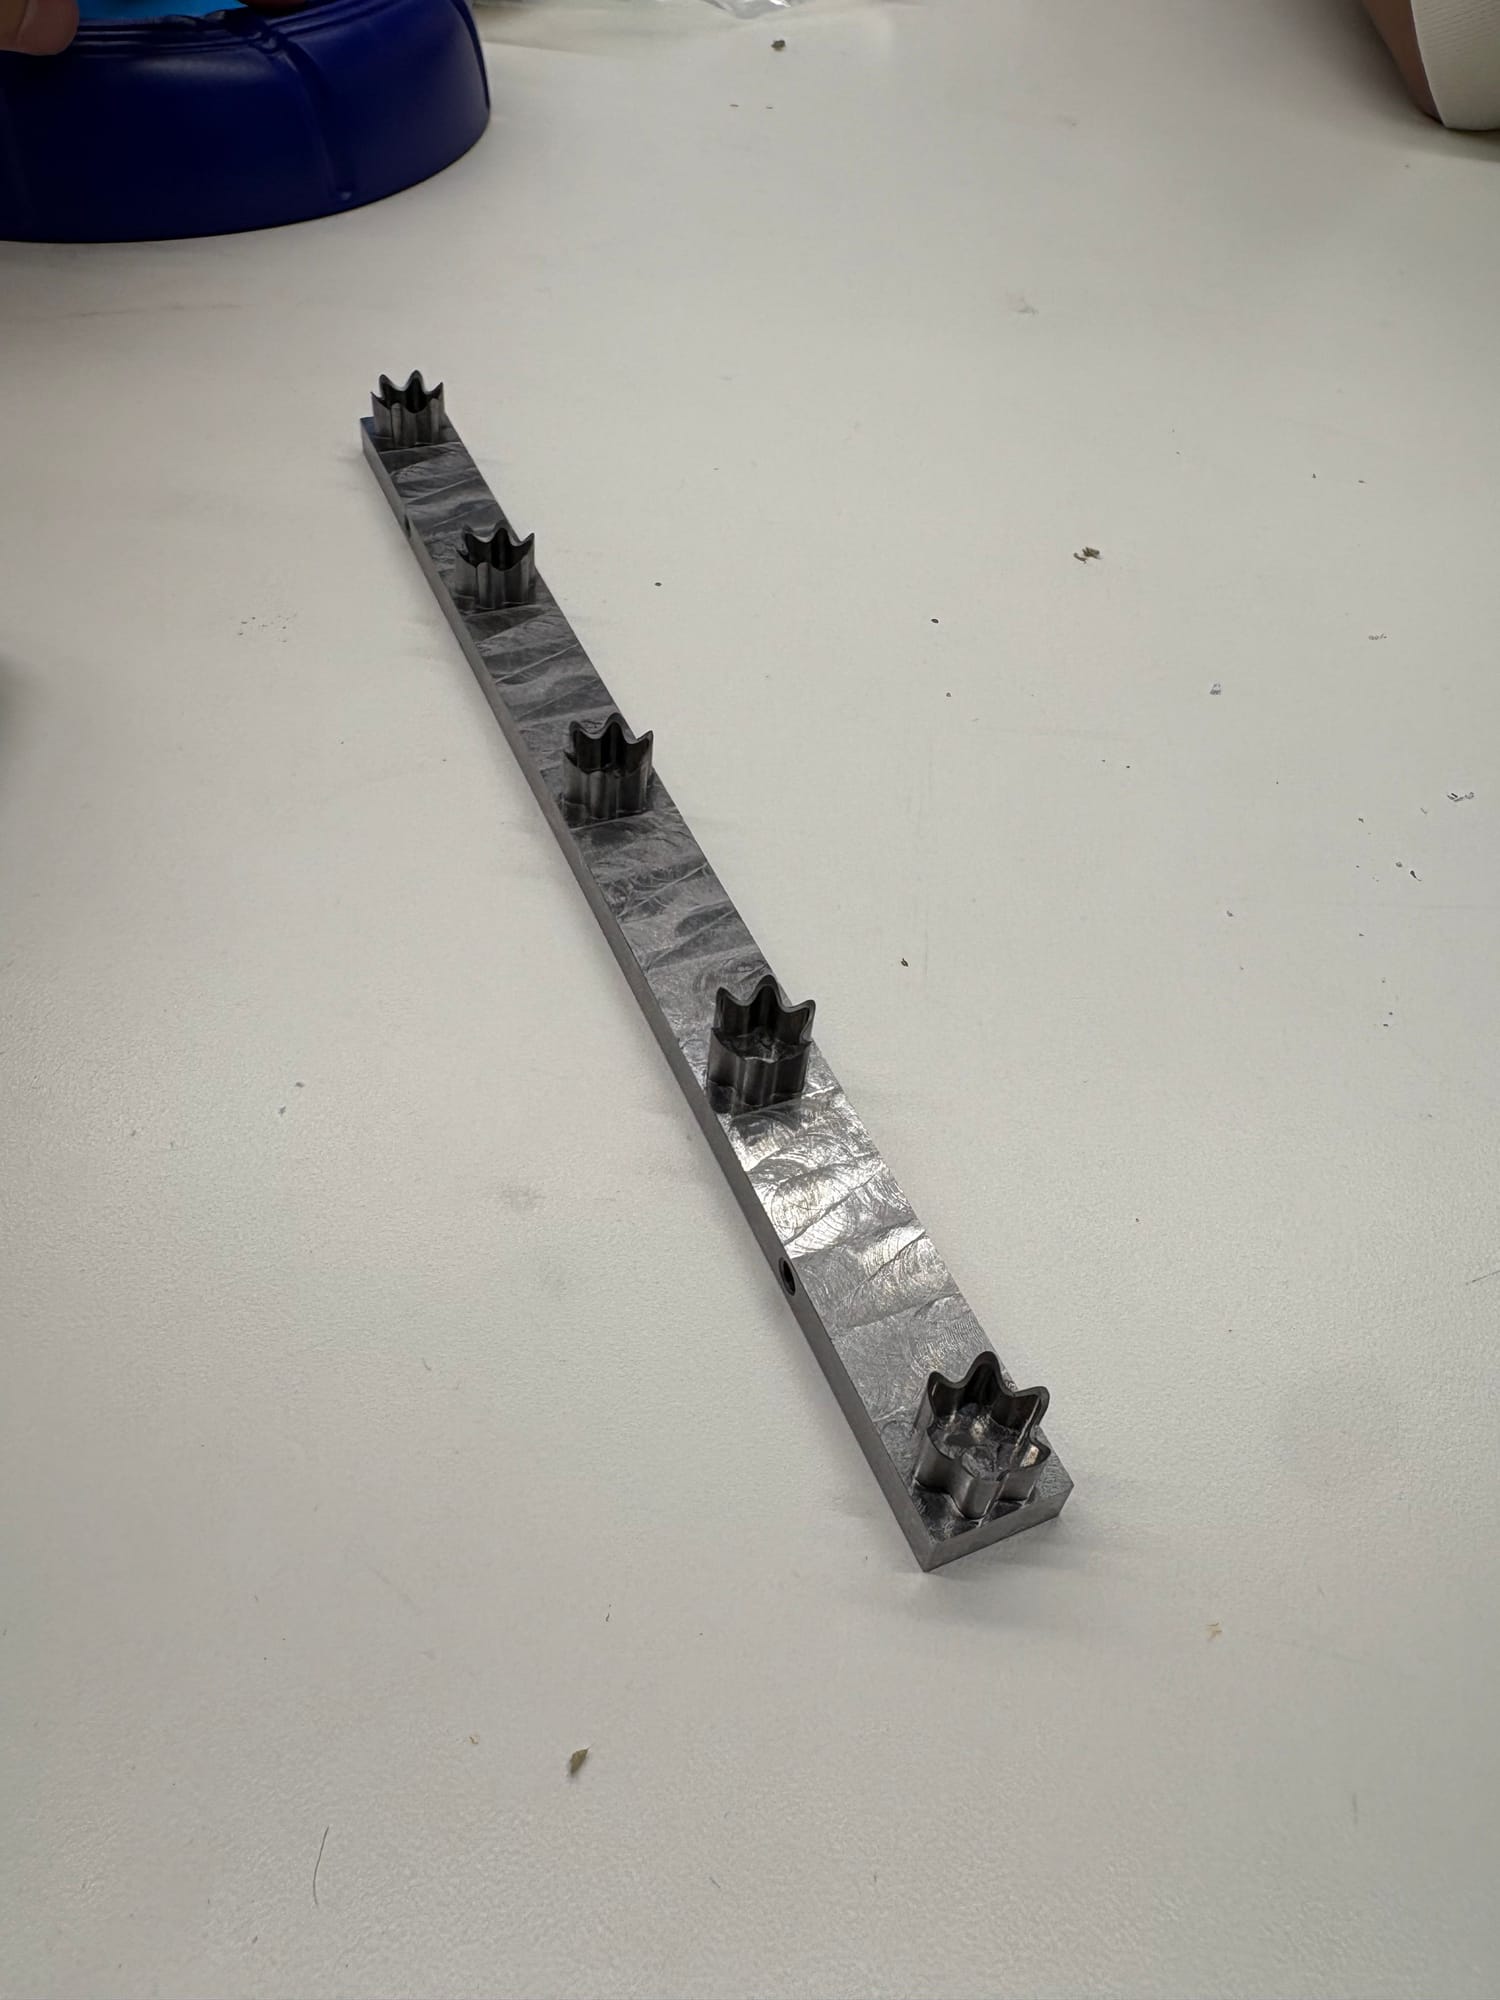
- Custom-machined hard tool steel, five flower-shaped blades
- SLA resin
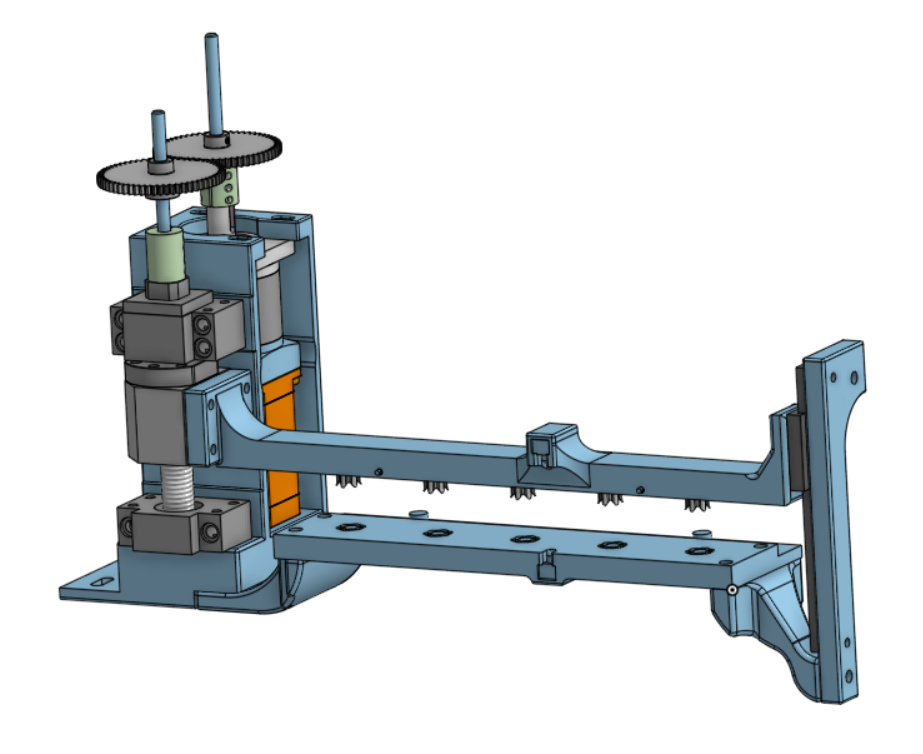
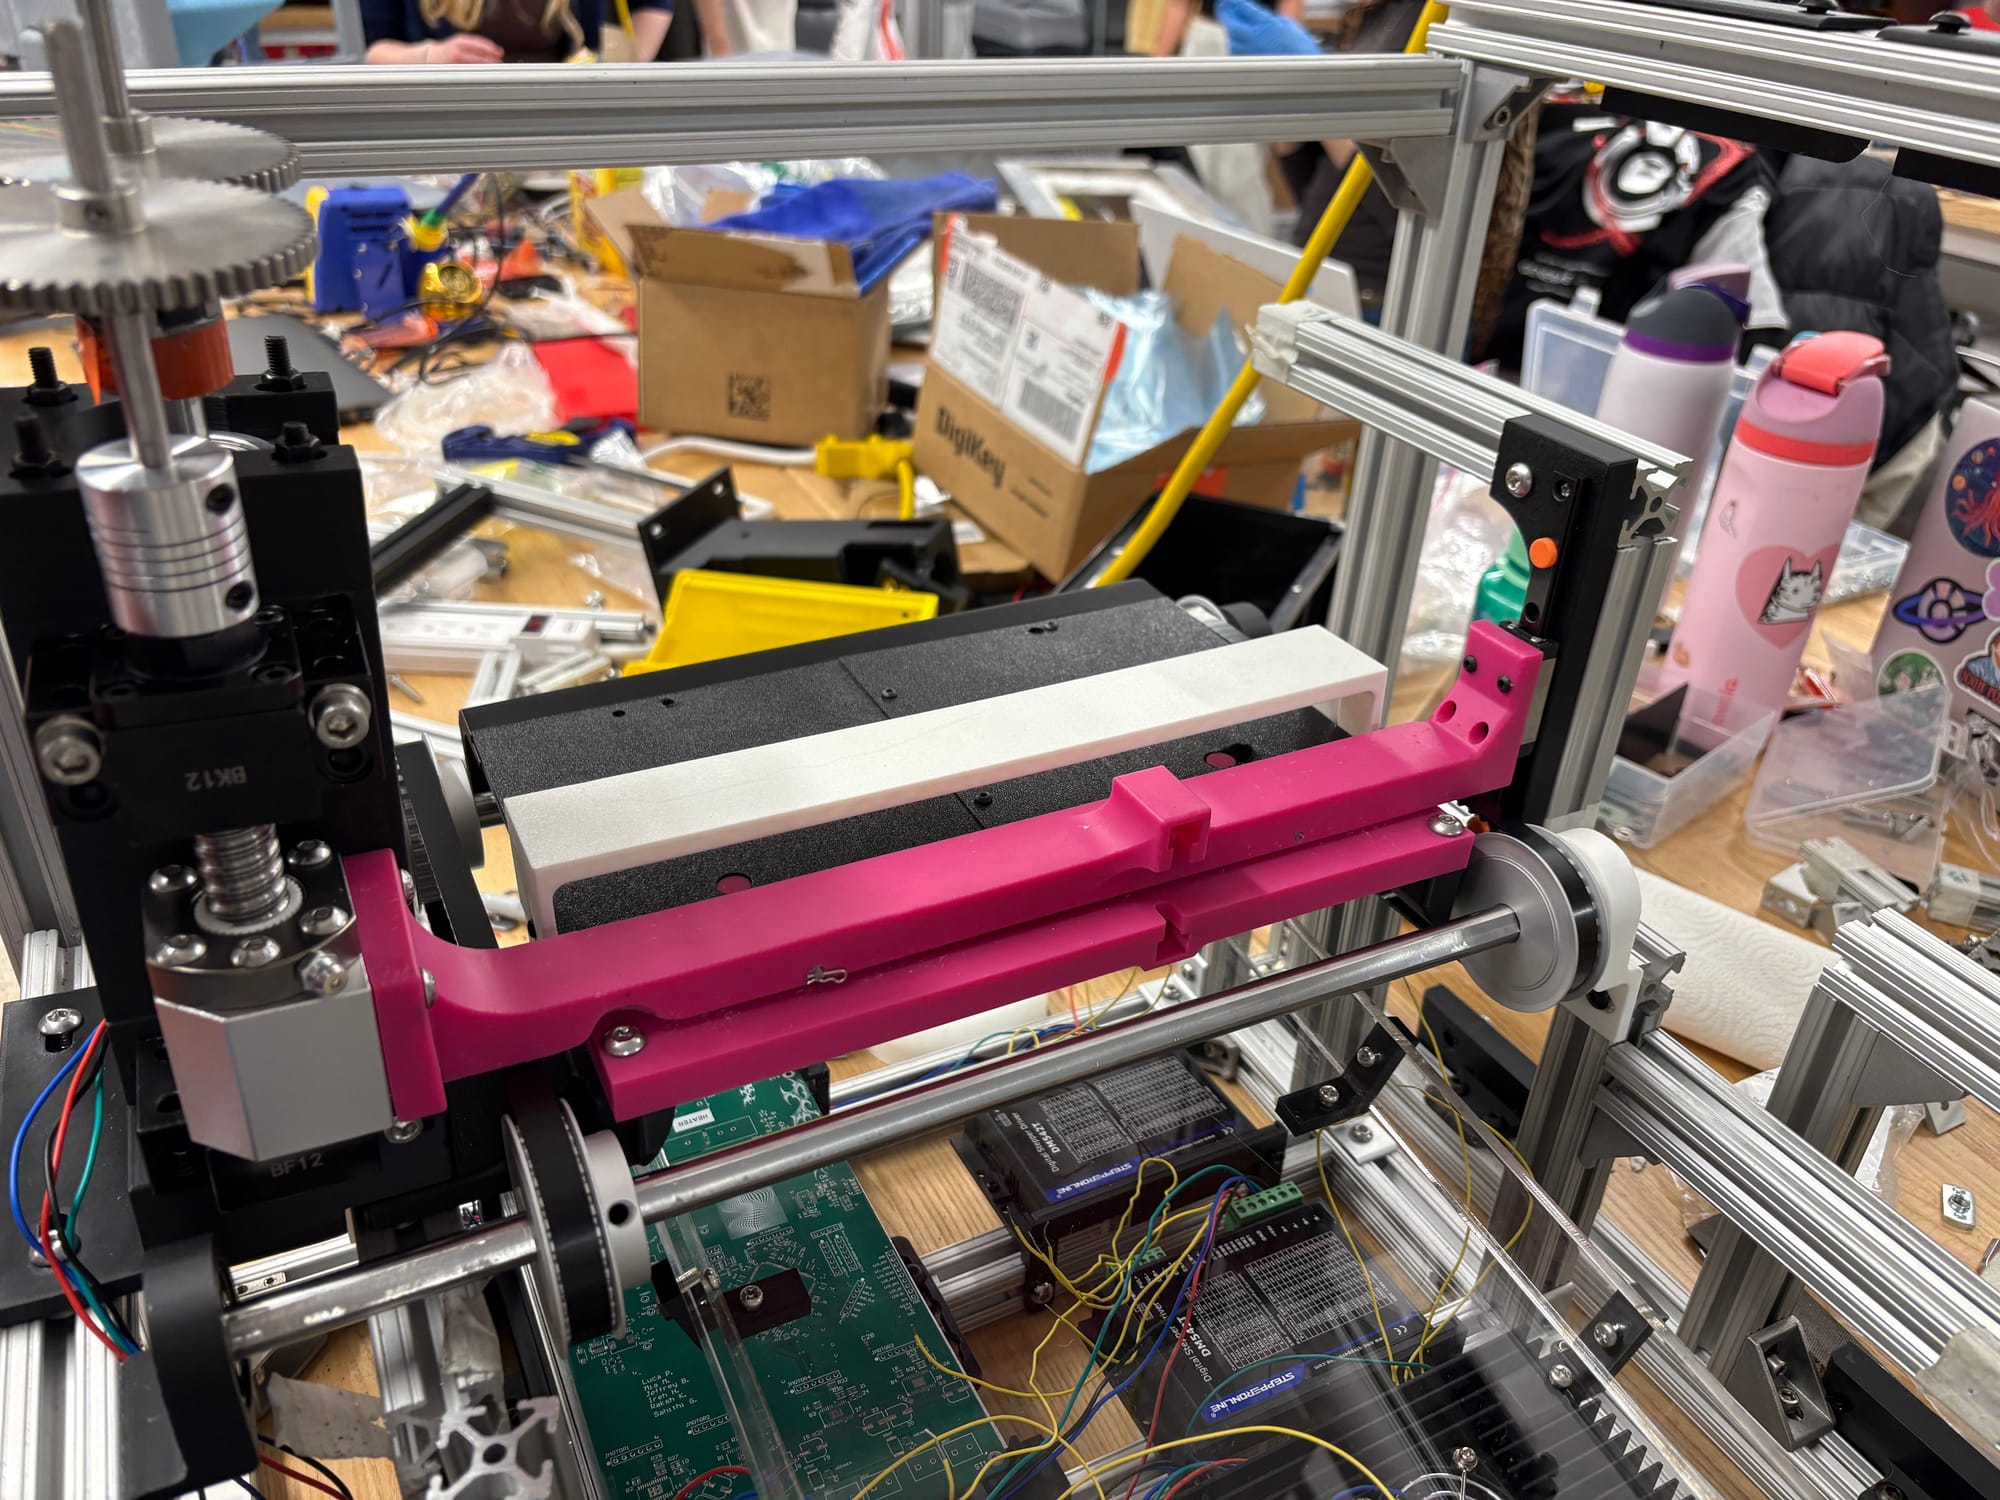
- Lead screw at one end, linear rail on the other
Focus areas
- Clean, consistent cuts
- Repeatability
- Tolerance stackup
- Machining cost
System
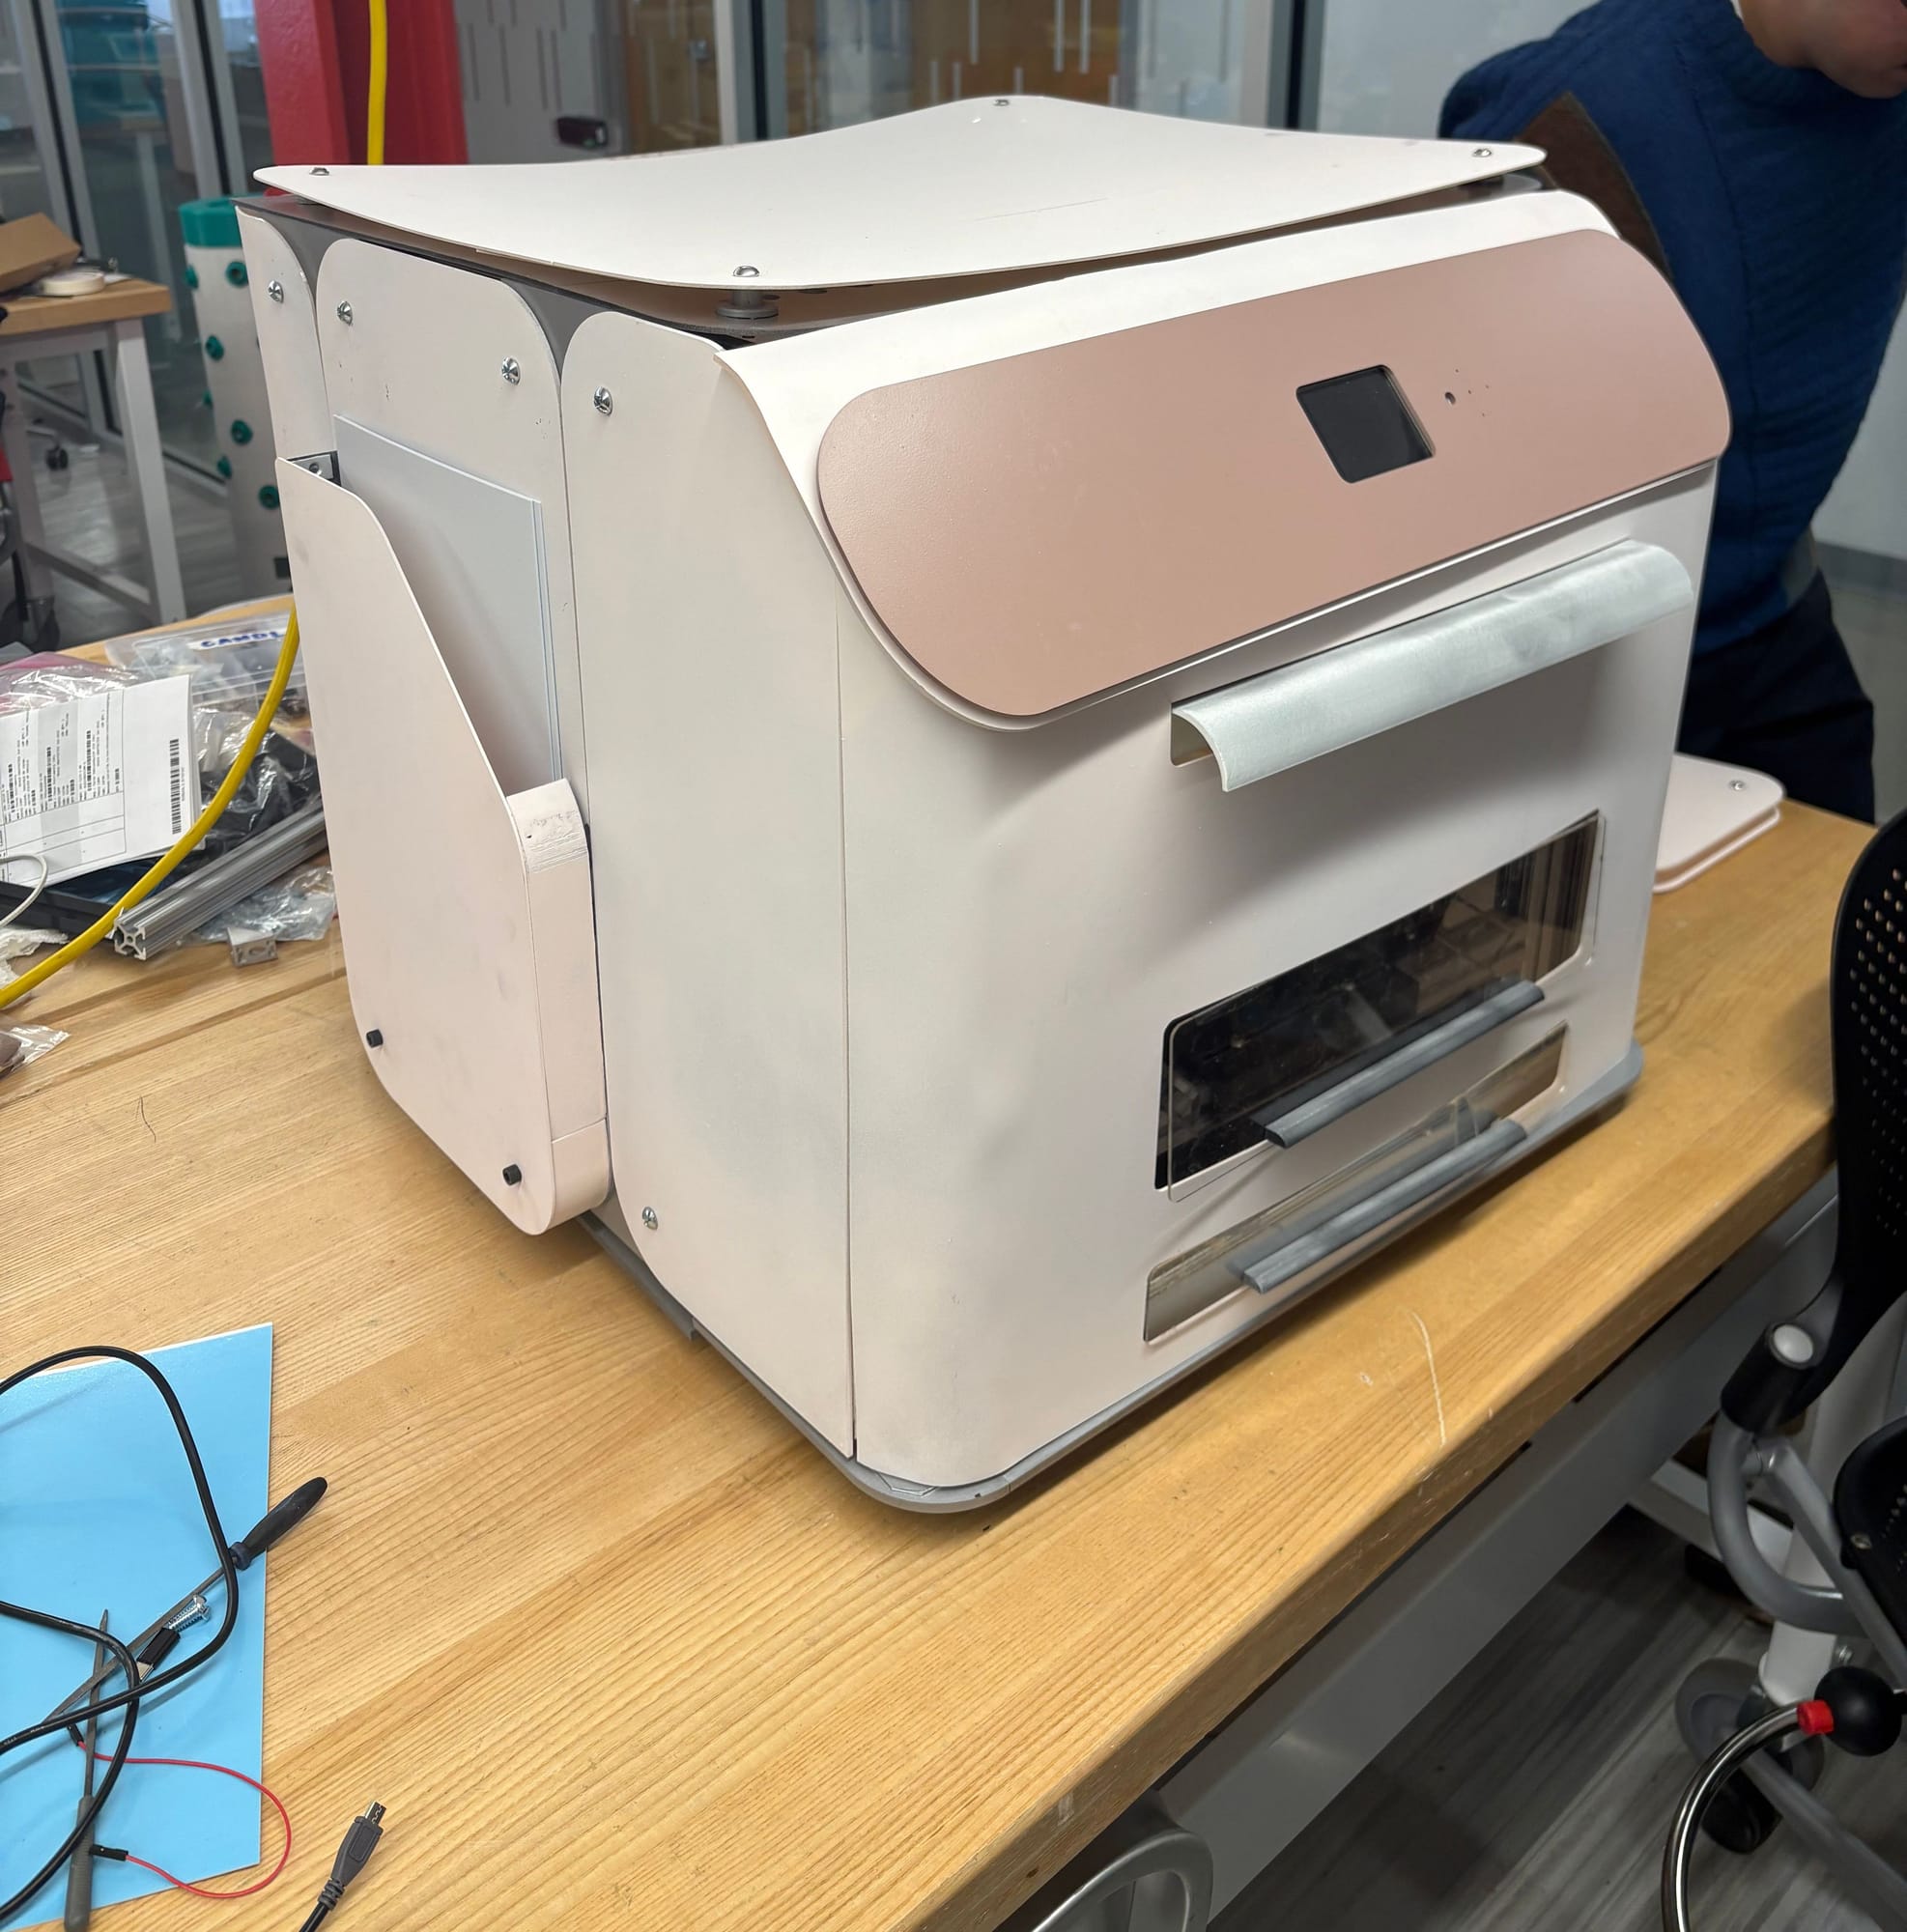
Sageware’s process consists of four steps: heating, molding, cutting, and dispensing.
Cutting
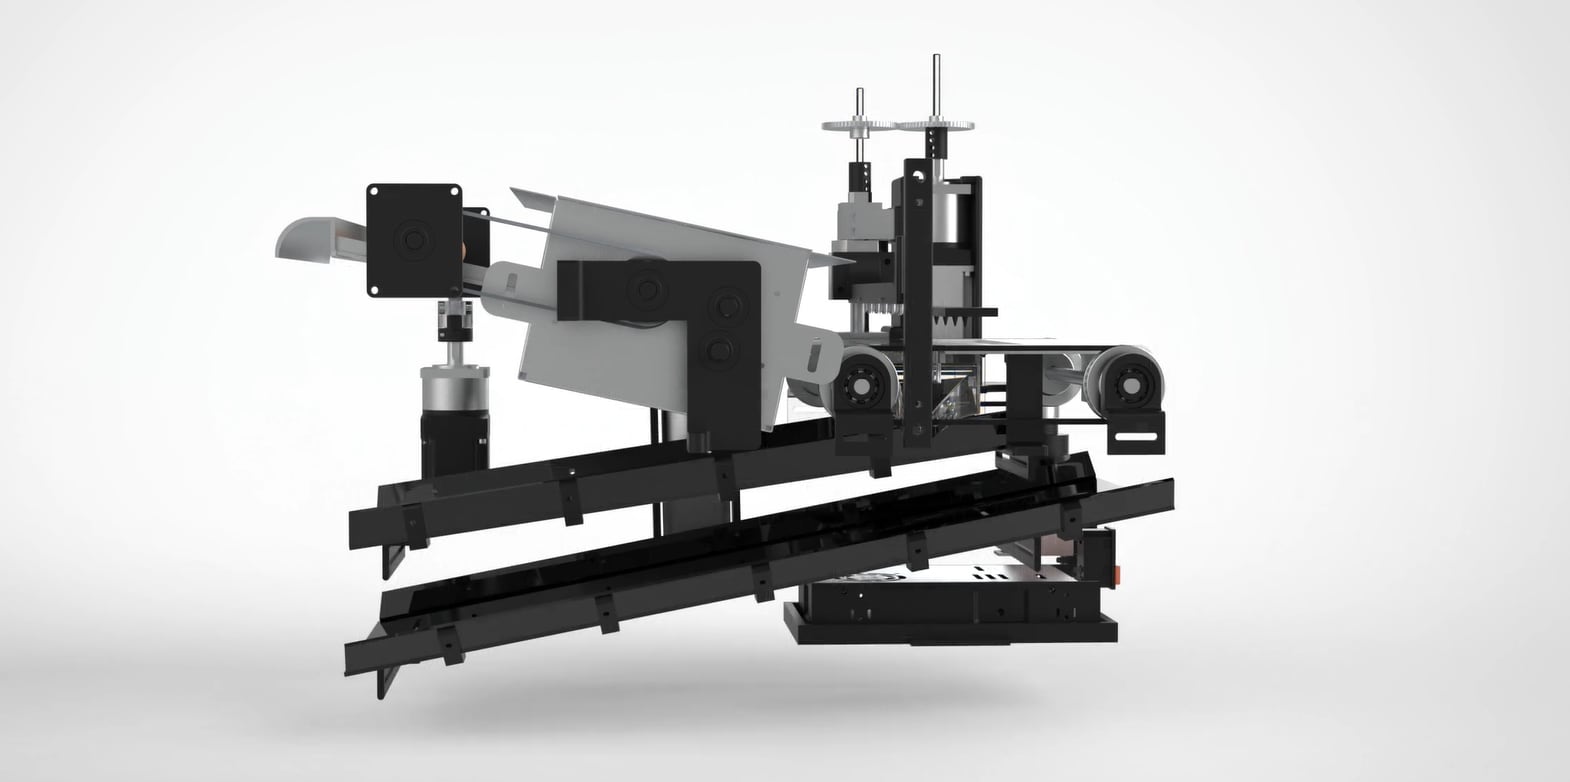
The heart of the cutting subsystem is a custom-machined steel stamp with five flower-shaped blades. For this, hard tool steel was used to ensure retention of a sharp edge with repeated use, requiring minimal service (and keeping cuts cleaner, as the client wanted).
This is fastened to an SLA resin jig for interfacing with power transfer components, reducing the total stock used (and therefore machining cost) when compared with machining the jig together with the stamp as one part. The jig/insert assembly is actuated vertically by a lead screw at one end, and fastened by a linear rail on the other.
Next project
Uplift Mobility DeviceLet’s talk.
Open to co-op, internship and project conversations in mechanical design, product development and R&D.